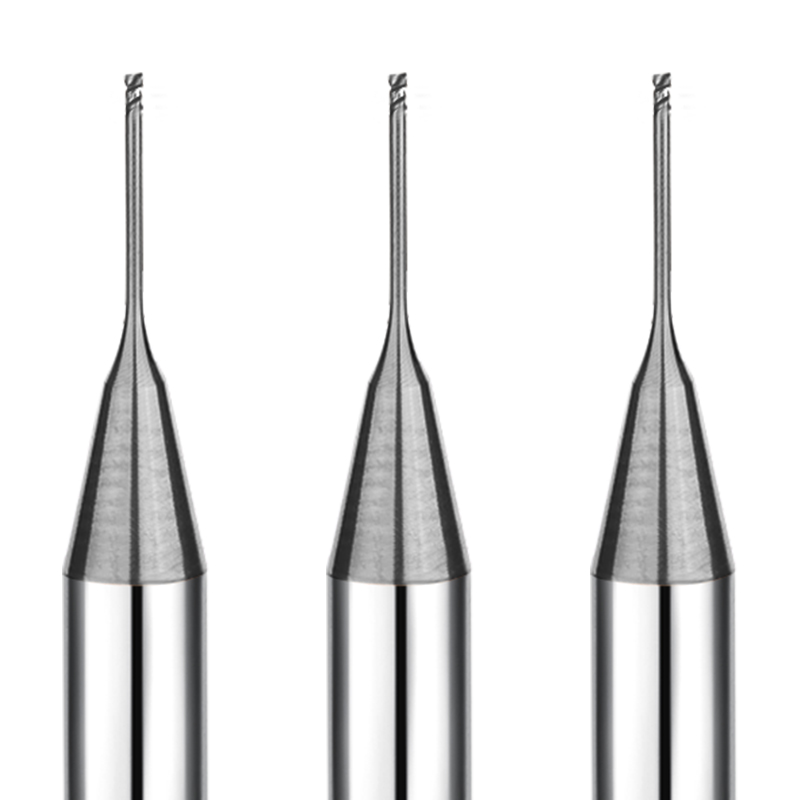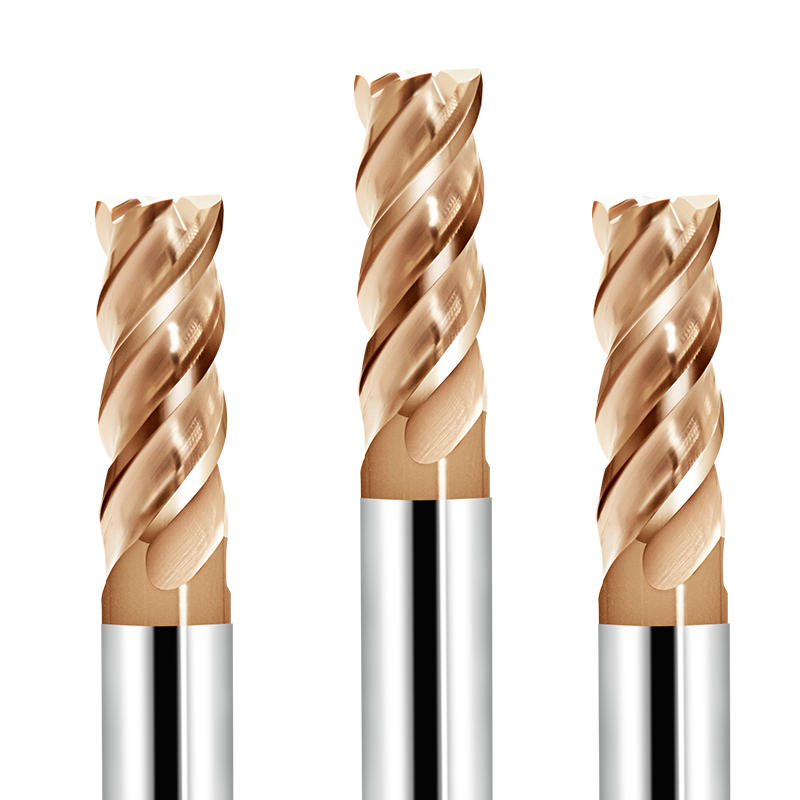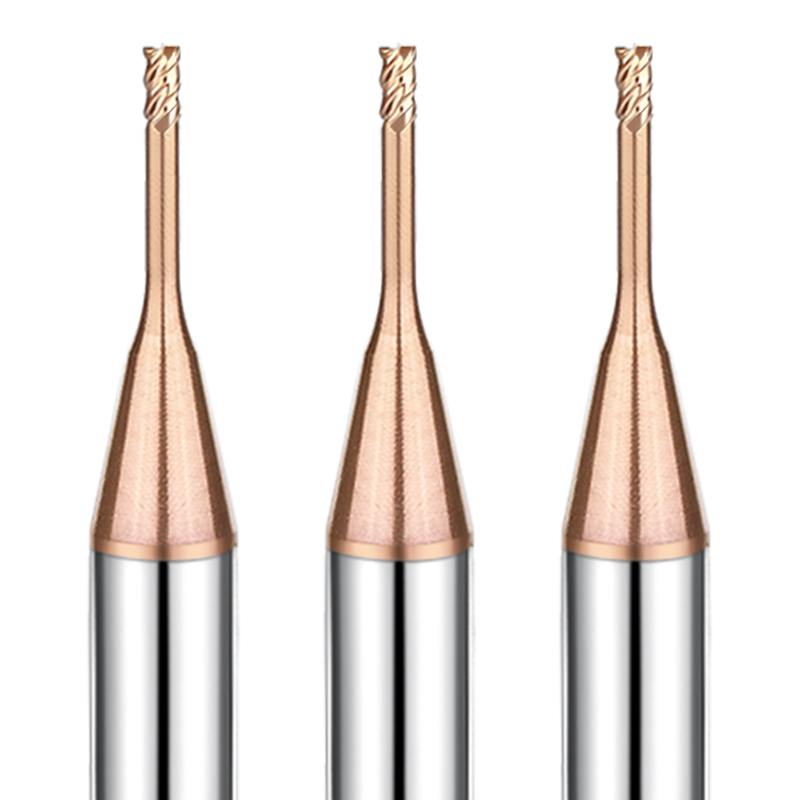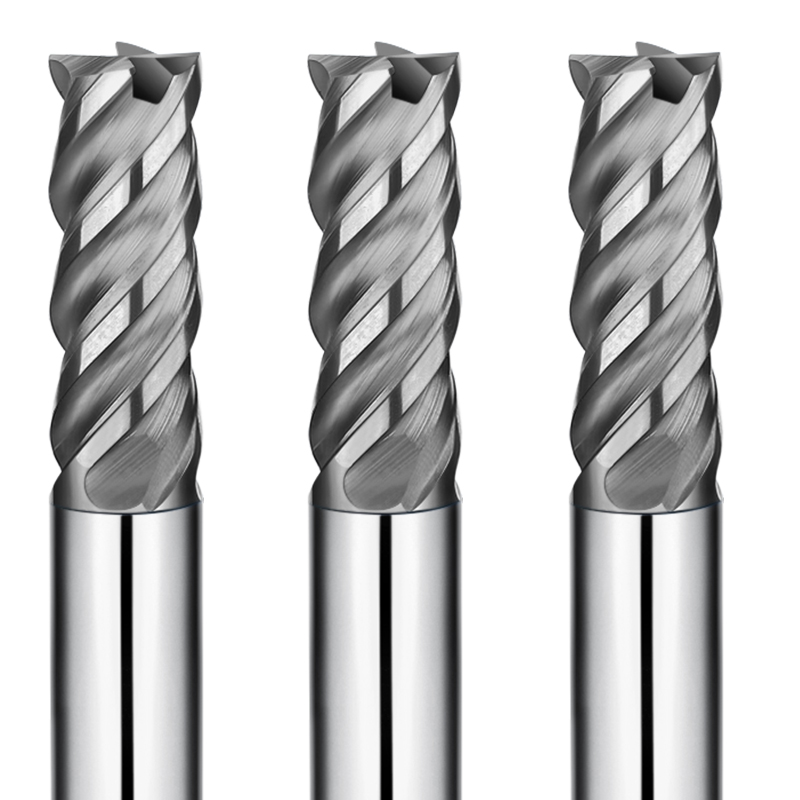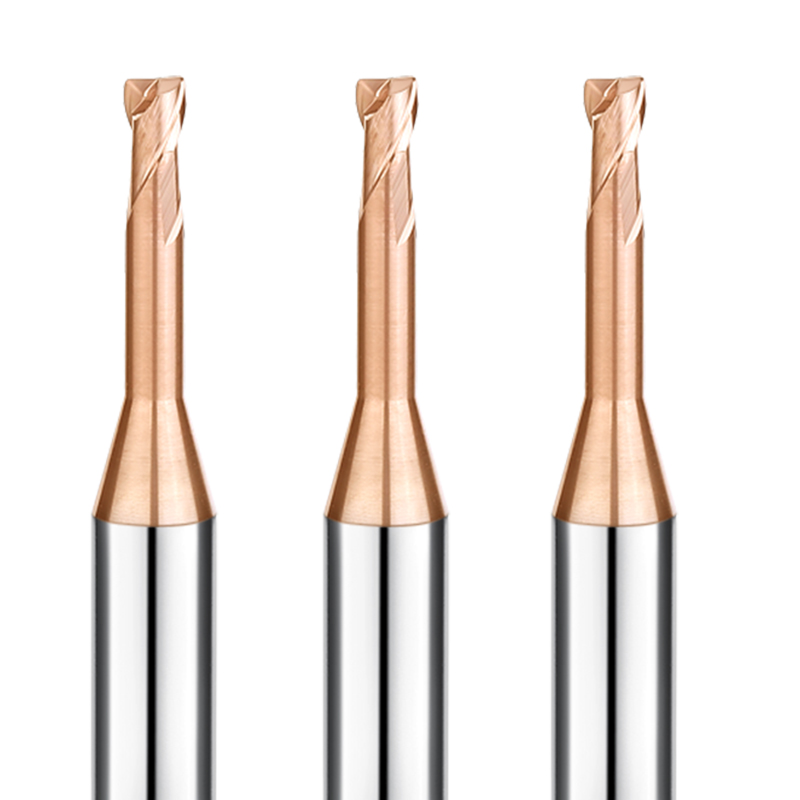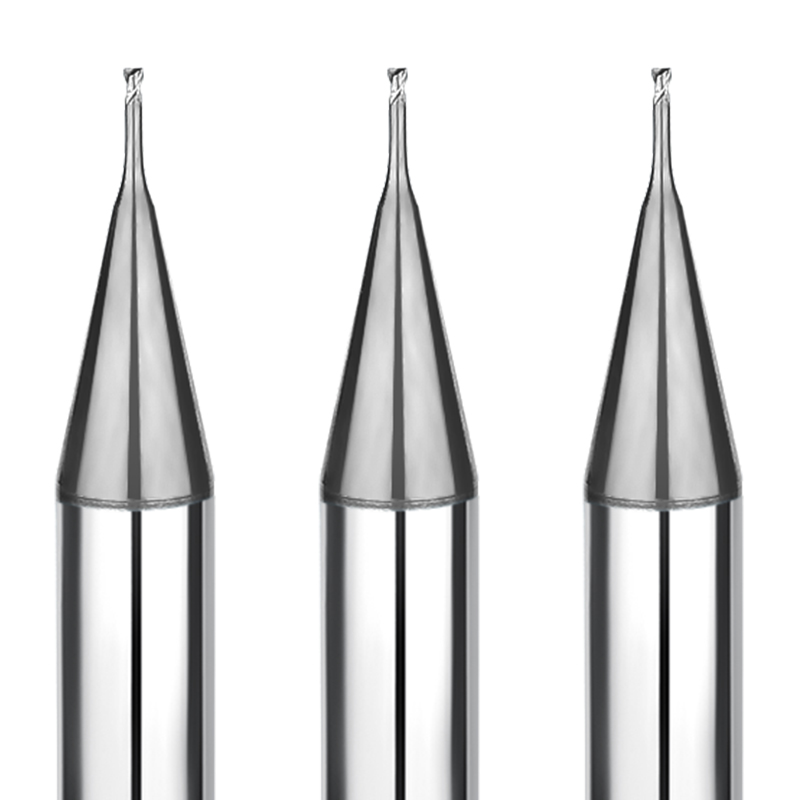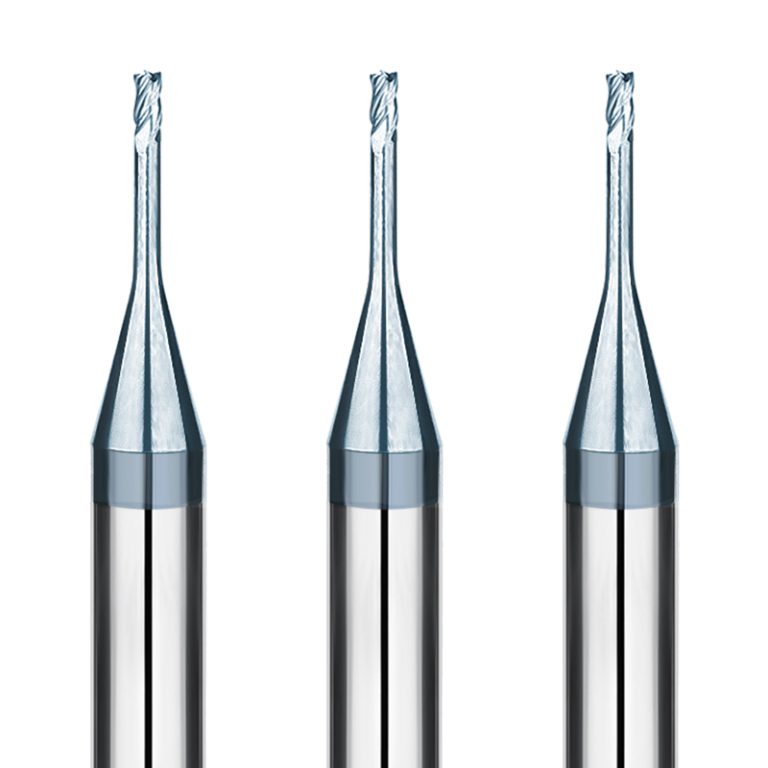
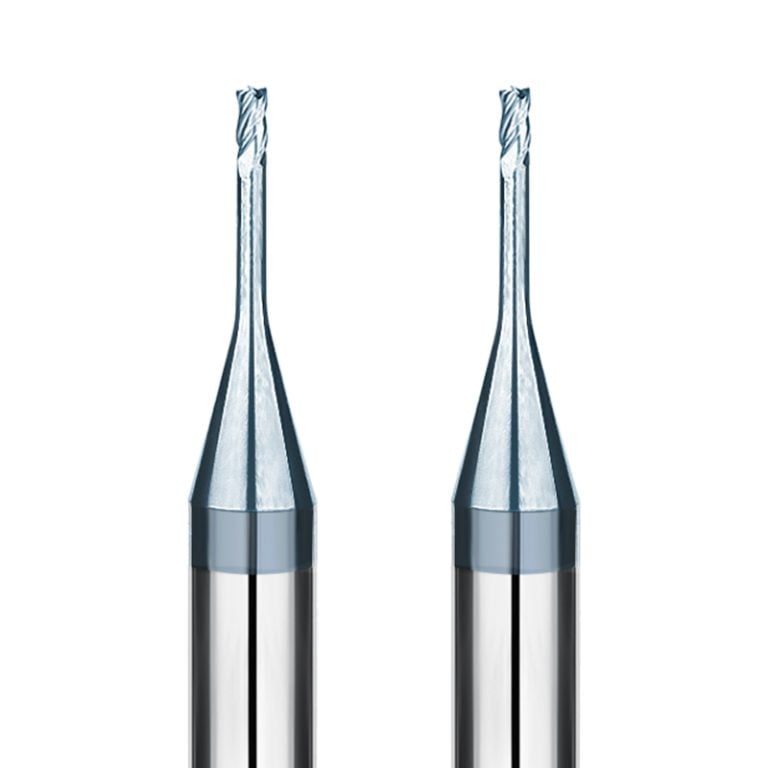
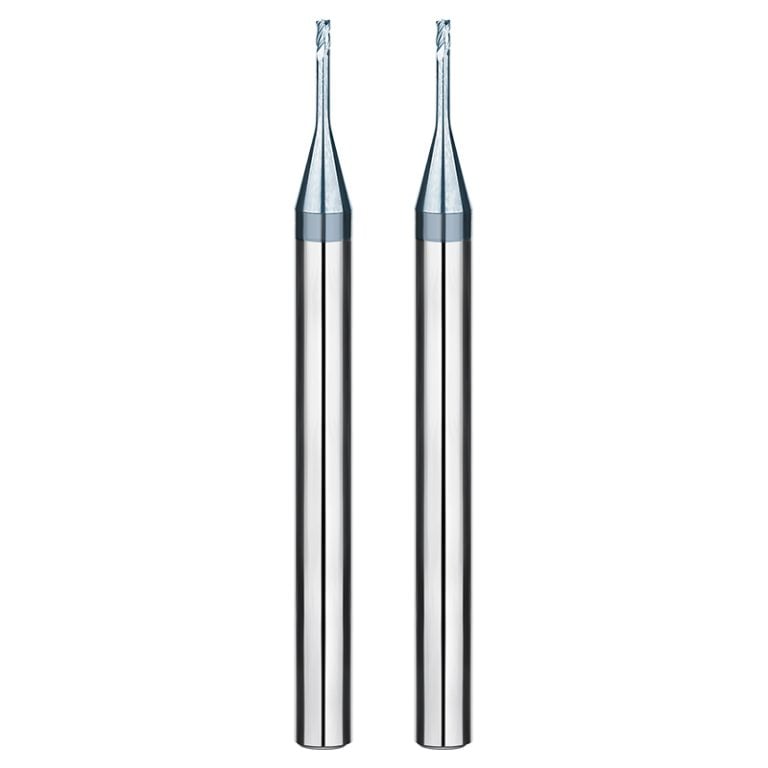
SAMHO HRC55 4 Flute Long-Neck Flat End Mill — High-Efficiency Solution for Deep Cavity Machining
High Precision Shank Diameter Control (0 to +0.003 mm)
Tight tolerance control ensures excellent clamping stability and high concentricity. This reduces tool runout and vibration during CNC machining. It improves surface finish and extends tool life in precision milling applications.
ALTiCrN High-Performance Coating (Wear & Heat Resistance)
Advanced ALTiCrN coating significantly increases hardness and oxidation resistance. It maintains stable cutting performance under high-speed machining, dry cutting, and elevated temperature conditions. Ideal for demanding mold and die applications.
Designed for Materials up to HRC 28–52
Optimized for medium to high hardness materials, including mold steel, stainless steel, and alloy steel. This long neck end mill provides a stable balance between cutting efficiency and tool durability in industrial CNC milling.
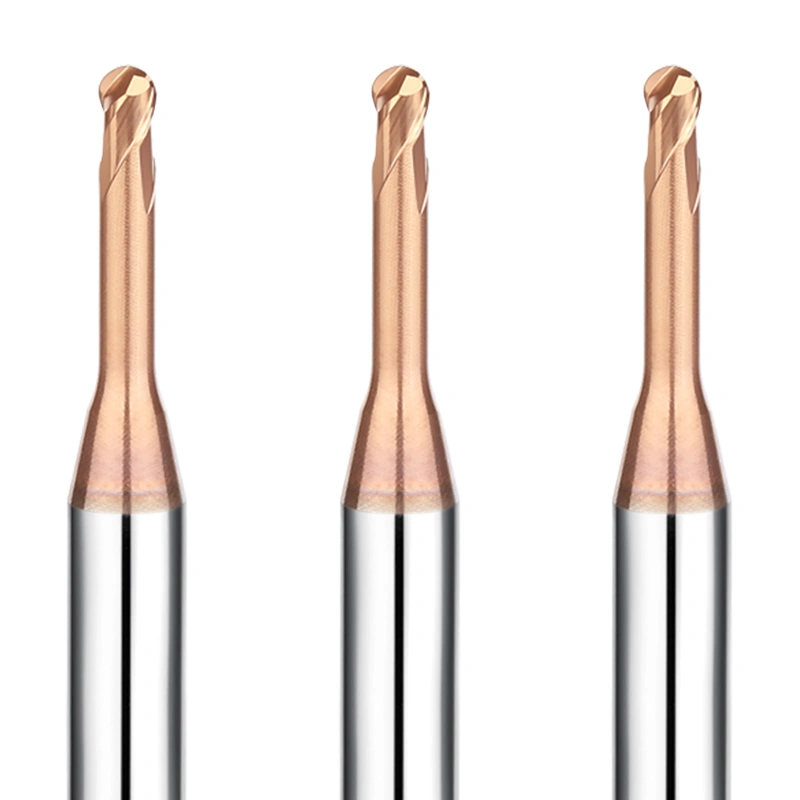
Long Neck End Mill Design for Deep Cavity Machining
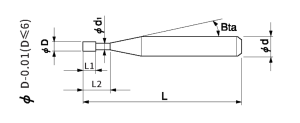
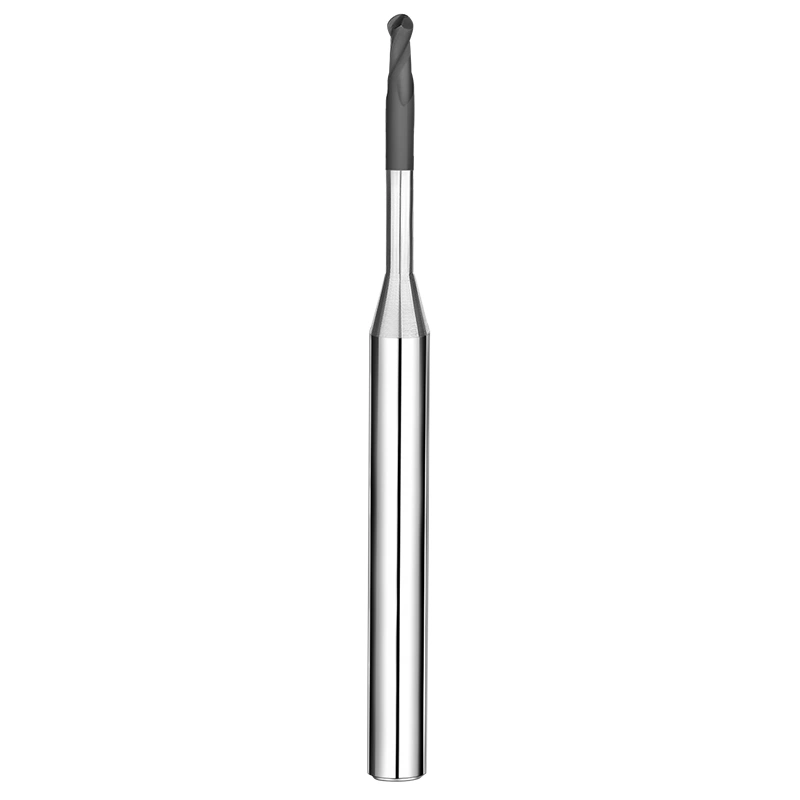
The long reach and extended neck design reduce interference in deep cavity and narrow space machining. It is ideal for deep slot milling, mold cavity finishing, and complex 3D contours. Improves accessibility in hard-to-reach machining areas.
Engineered for HRC55-Level Performance Stability
Built for high rigidity and toughness balance, this long neck flat milling cutter supports machining conditions up to HRC55 hardened materials. It delivers consistent cutting stability, reduced tool deflection, and extended service life in demanding CNC operations.
HRC55 4-Flute Long-Neck Flat End Mill — Professional Usage Recommendations
Recommended for Finishing and Semi-Finishing (HRC 28–52 Materials)
Suitable for medium to high hardness materials such as mold steel, stainless steel, and alloy steel. This 4 flute long neck end mill is primarily designed for finishing and semi-finishing operations. It delivers stable cutting performance and improved surface finish.
Control Cutting Loads to Prevent Tool Deflection
The long neck structure has reduced rigidity compared to standard end mills. Use light to medium cutting parameters. Avoid excessive axial and radial engagement. This helps reduce tool deflection, vibration, and chatter during deep cavity machining.
Use Short Tool Overhang for Maximum Stability
Keep tool overhang as short as possible to improve machining rigidity. Use high-precision tool holders such as shrink-fit chucks or precision ER collets. Proper clamping improves concentricity and reduces runout.
Recommended Climb Milling Strategy
Climb milling (down milling) is recommended for most applications. It reduces cutting impact and stabilizes tool load. This improves surface finish quality and extends tool life, especially in mold cavity finishing operations.
Optimize Cutting Parameters for Tool Life
Use moderate spindle speed with consistent feed rates. Avoid excessive feed that may cause edge chipping. For deep cavity machining, use step-down or layered cutting strategies to gradually remove material and maintain tool stability.
Ideal for Deep Cavities, Narrow Slots, and Complex Geometries
This long neck end mill is designed for deep cavity and high aspect ratio machining. It performs well in narrow slots and complex mold structures. Avoid prolonged heavy side cutting. Use segmented toolpaths to maintain stability and tool life.