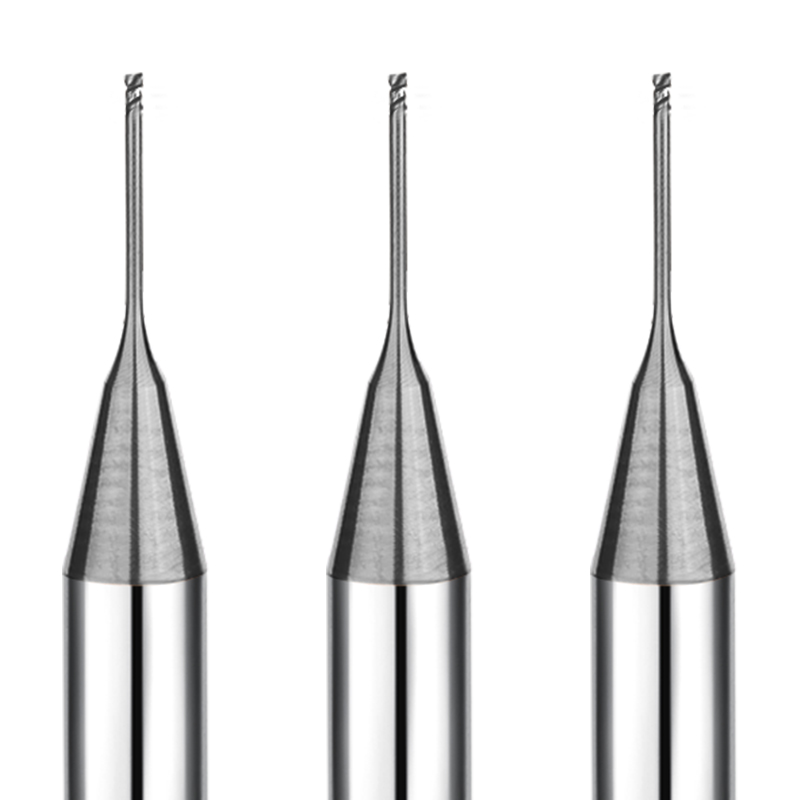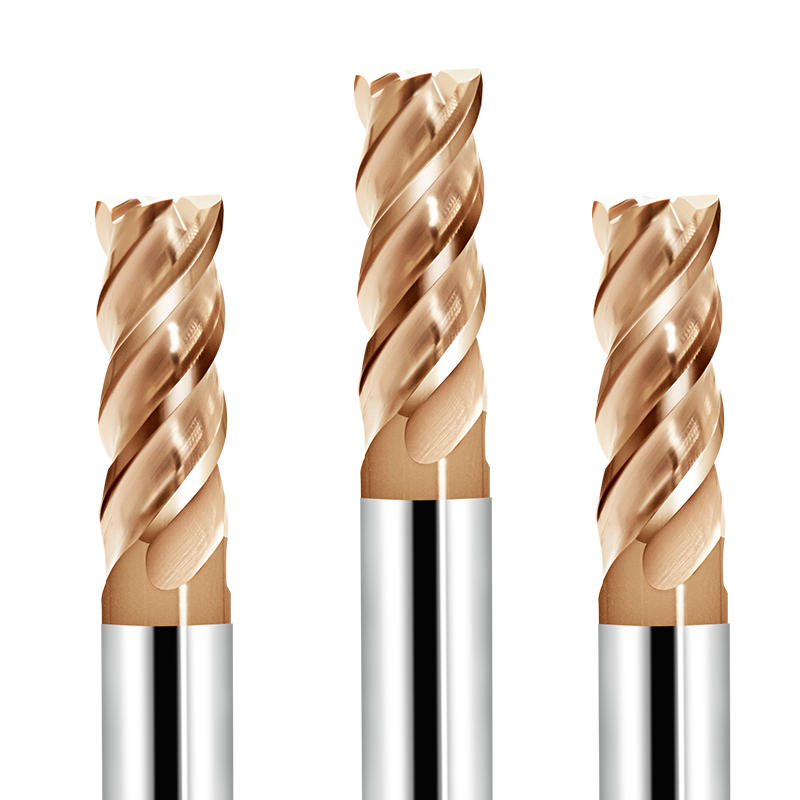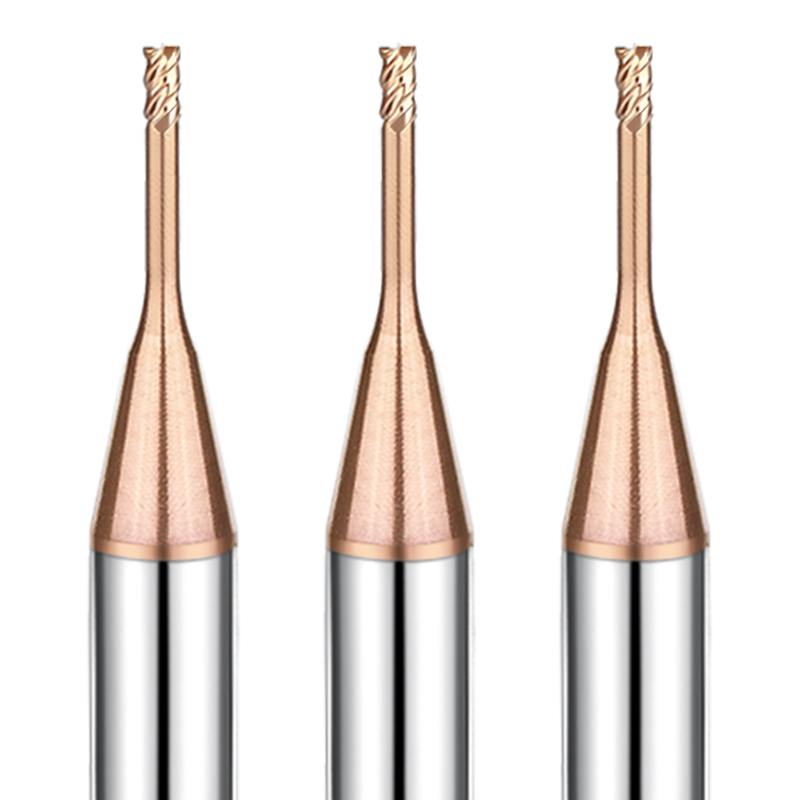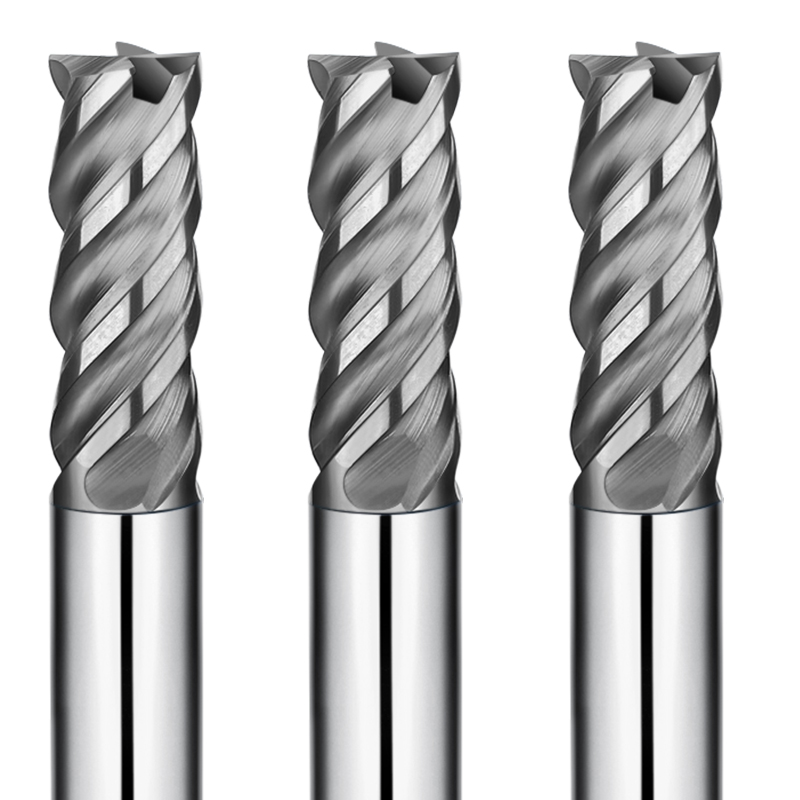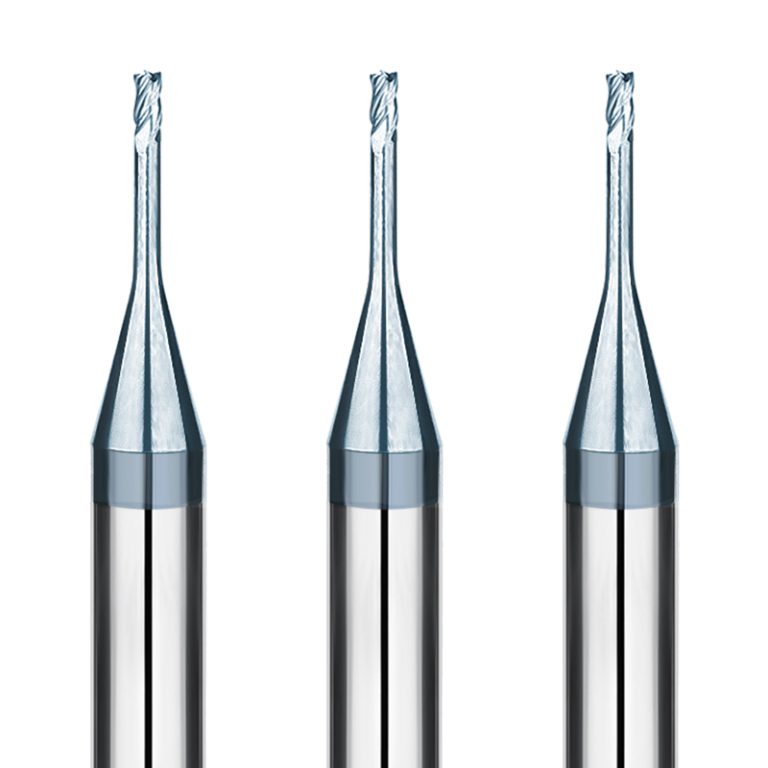
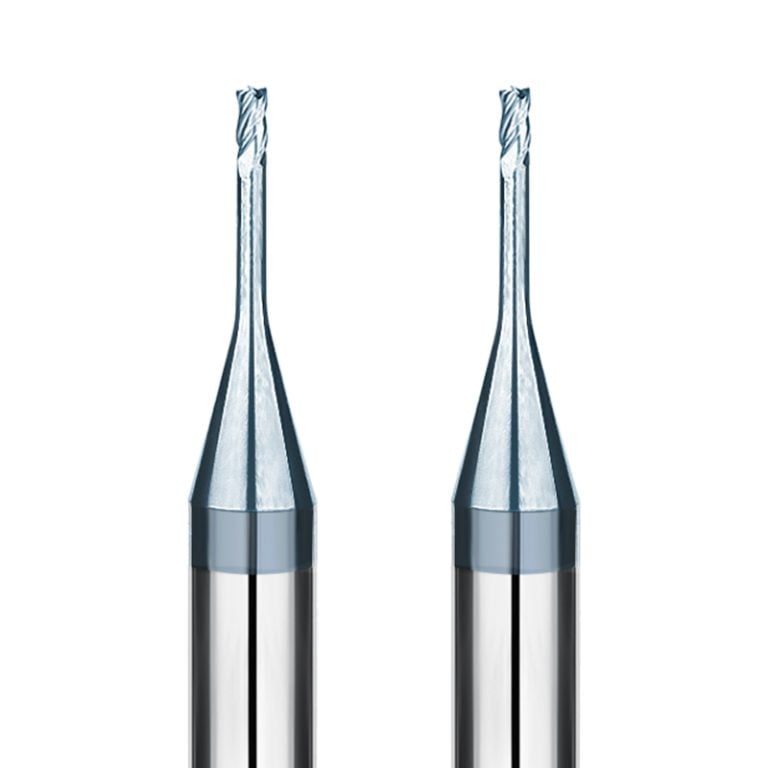
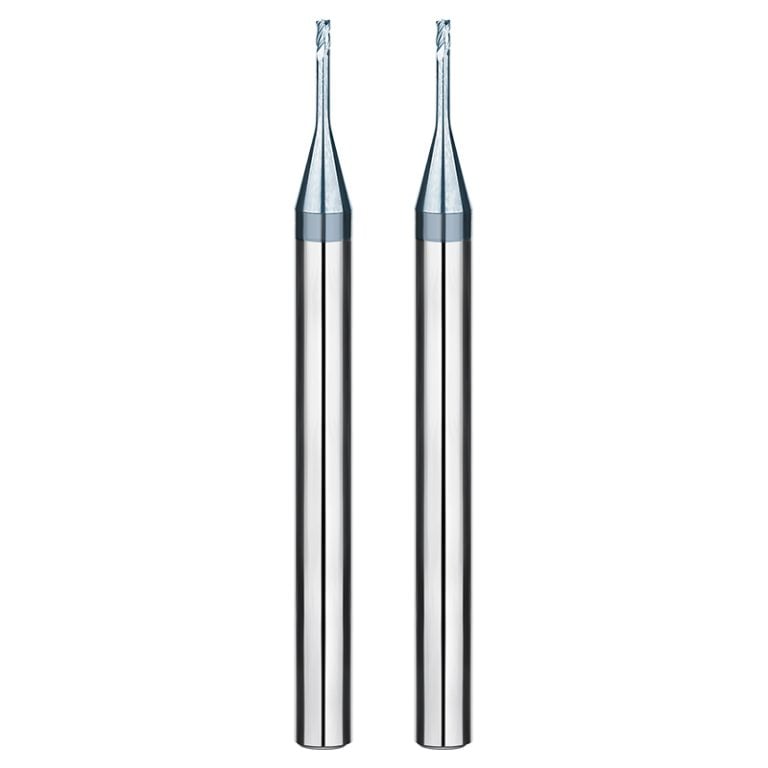
4 flute long neck flat end mills 4 flute long neck flat end mills 4 flute long neck flat end mills

hrc55 4 flute long neck flat end mill

Why Partner with SAMHO China?

Consistent High-Quality Manufacturing Standards

SAMHO follows strict industrial-grade production processes and full inspection control. Each HRC55 4 flute long neck square end mill is manufactured for consistent performance and stable CNC machining results. It is suitable for global industrial production environments.

Extended Tool Life and Lower Machining Costs

Advanced substrate materials and coating technology improve wear resistance and thermal stability. The tool maintains reliable performance in deep cavity machining and high-load cutting conditions. This helps reduce tool change frequency and overall machine downtime.

High-Precision Tolerance Control for Stable Machining

Critical dimensions are controlled within micron-level tolerances. This improves tool concentricity and dynamic balance during high-speed CNC milling. It reduces tool runout and vibration, resulting in better surface finish quality and machining stability.

Reliable Stock Availability and Fast Delivery

Standard specifications are maintained in stable inventory. This ensures fast shipping and consistent supply chain performance. It supports both bulk orders and urgent production requirements, improving manufacturing efficiency and delivery reliability.

Strong OEM / ODM Customization Capability

We provide full OEM and ODM services, including non-standard dimensions, coating customization, structural optimization, and private labeling. This supports customers in building differentiated product lines for specific market demands.

Continuous R&D and Process Innovation

SAMHO continuously improves tool geometry and coating performance based on real machining feedback. This ongoing development enhances cutting efficiency, improves tool life, and ensures stable performance in HRC55 long neck end mill applications.

SAMHO HRC55 4 Flute Long-Neck Flat End Mill — High-Efficiency Solution for Deep Cavity Machining

High Precision Shank Diameter Control (0 to +0.003 mm)

Tight tolerance control ensures excellent clamping stability and high concentricity. This reduces tool runout and vibration during CNC machining. It improves surface finish and extends tool life in precision milling applications.

ALTiCrN High-Performance Coating (Wear & Heat Resistance)

Advanced ALTiCrN coating significantly increases hardness and oxidation resistance. It maintains stable cutting performance under high-speed machining, dry cutting, and elevated temperature conditions. Ideal for demanding mold and die applications.

Designed for Materials up to HRC 28–52

Optimized for medium to high hardness materials, including mold steel, stainless steel, and alloy steel. This long neck end mill provides a stable balance between cutting efficiency and tool durability in industrial CNC milling.

Long Neck End Mill Design for Deep Cavity Machining

The long reach and extended neck design reduce interference in deep cavity and narrow space machining. It is ideal for deep slot milling, mold cavity finishing, and complex 3D contours. Improves accessibility in hard-to-reach machining areas.

Engineered for HRC55-Level Performance Stability

Built for high rigidity and toughness balance, this long neck flat milling cutter supports machining conditions up to HRC55 hardened materials. It delivers consistent cutting stability, reduced tool deflection, and extended service life in demanding CNC operations.


HRC55 4-Flute Long-Neck Flat End Mill — Professional Usage Recommendations

Recommended for Finishing and Semi-Finishing (HRC 28–52 Materials)

Suitable for medium to high hardness materials such as mold steel, stainless steel, and alloy steel. This 4 flute long neck end mill is primarily designed for finishing and semi-finishing operations. It delivers stable cutting performance and improved surface finish.

Control Cutting Loads to Prevent Tool Deflection

The long neck structure has reduced rigidity compared to standard end mills. Use light to medium cutting parameters. Avoid excessive axial and radial engagement. This helps reduce tool deflection, vibration, and chatter during deep cavity machining.

Use Short Tool Overhang for Maximum Stability

Keep tool overhang as short as possible to improve machining rigidity. Use high-precision tool holders such as shrink-fit chucks or precision ER collets. Proper clamping improves concentricity and reduces runout.

Recommended Climb Milling Strategy

Climb milling (down milling) is recommended for most applications. It reduces cutting impact and stabilizes tool load. This improves surface finish quality and extends tool life, especially in mold cavity finishing operations.

Optimize Cutting Parameters for Tool Life

Use moderate spindle speed with consistent feed rates. Avoid excessive feed that may cause edge chipping. For deep cavity machining, use step-down or layered cutting strategies to gradually remove material and maintain tool stability.

Ideal for Deep Cavities, Narrow Slots, and Complex Geometries

This long neck end mill is designed for deep cavity and high aspect ratio machining. It performs well in narrow slots and complex mold structures. Avoid prolonged heavy side cutting. Use segmented toolpaths to maintain stability and tool life.
Recommended Materials for Machining (Highly Recommended: ⭐️ | Recommended: ⭕️ | Suggested: )

Category Work Material Grade
DIE STEEL Carbon steels (S45C/S55C) ⭕️
Alloy steels (SK/SCM/SUS) ⭕️
Prehardened steels (NAK/HPM) ⭕️
Hardened steels (~55/~60/~70HRC)
SPECIAL MATERIAL Aluminum alloys
Graphite
Copper ⭕️
Plastics
Carbon fiber
Titanium alloys
Heat resistant alloys
Cemented carbide
Hard brittle (non-metallic) material

2 flute flat long neck end mill


Total 24 models

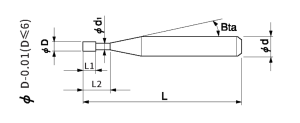
Model Number Outside Diameter LLength Of Cut Effective Length Shank Taper Angle Overall Length Number Of Flutes Shank Diameter In Stock
SHBLS4-010040 1 1.5 4 12° 50 4 4
SHBLS4-010060 1 1.5 6 12° 50 4 4
SHBLS4-010080 1 1.5 8 12° 50 4 4
SHBLS4-010100 1 1.5 10 12° 50 4 4
SHBLS4-015040 1.5 2.3 4 12° 50 4 4
SHBLS4-015060 1.5 2.3 6 12° 50 4 4
SHBLS4-015080 1.5 2.3 8 12° 50 4 4
SHBLS4-015100 1.5 2.3 10 12° 50 4 4
SHBLS4-020060 2 3 6 12° 50 4 4
SHBLS4-020080 2 3 8 12° 50 4 4
SHBLS4-020100 2 3 10 12° 50 4 4
SHBLS4-020120 2 3 12 12° 50 4 4
SHBLS4-020160 2 3 16 12° 50 4 4
SHBLS4-020200 2 3 20 12° 50 4 4
SHBLS4-030080 3 4.5 8 12° 50 4 4
SHBLS4-030100 3 4.5 10 12° 50 4 4
SHBLS4-030120 3 4.5 12 12° 50 4 4
SHBLS4-030160 3 4.5 16 12° 50 4 4
SHBLS4-030200 3 4.5 20 12° 50 4 4
SHBLS4-030080-6 3 4.5 8 12° 50 4 6
SHBLS4-030100-6 3 4.5 10 12° 50 4 6
SHBLS4-030120-6 3 4.5 12 12° 50 4 6
SHBLS4-030160-6 3 4.5 16 12° 50 4 6
SHBLS4-030200-6 3 4.5 20 12° 50 4 6


SHBLS4 Contour Milling Parameters

Work Material Oxygen-free CopperRed Copper HRC30-45 carbon steeland prehardened steel HRC45-55 hardened steel
(mm)Diameter (mm)Effective Length (min-1)Speed (mm/min)Feed (min-1)Speed (mm/min)Feed (min-1)Speed (mm/min)Feed
D1.0 4 13000 1300 13000 1300 12000 1200
D1.0 6 11000 1000 11000 1000 10000 800
D1.0 8 10000 800 10000 800 8500 700
D1.0 10 9000 500 9000 500 7500 500
D1.5 4 13000 1400 13000 1400 13000 1200
D1.5 6 11000 1200 11000 1200 10000 1000
D1.5 8 10000 1000 10000 1000 9000 900
D1.5 10 9000 900 9000 900 8500 800
D2.0 6 12000 1500 12000 1500 10000 1200
D2.0 8 11000 1300 11000 1300 9000 1000
D2.0 10 10000 1200 10000 1200 8000 800
D2.0 12 9000 900 9000 900 7000 700
D2.0 16 7500 700 7500 700 6000 600
D2.0 20 7000 400 7000 400 5500 300
D3.0 8 8500 2000 8500 2000 8000 1800
D3.0 10 8500 2000 8500 2000 8000 1800
D3.0 12 8000 1800 8000 1800 7000 1600
D3.0 16 7000 1400 7000 1400 6000 1200
D3.0 20 6500 1200 6500 1200 5500 1000
D3.0 8 8500 2000 8500 2000 8000 1800
D3.0 10 8500 2000 8500 2000 8000 1800
D3.0 12 8000 1800 8000 1800 7000 1600
D3.0 16 7000 1400 7000 1400 6000 1200
D3.0 20 6500 1200 6500 1200 5500 1000
Note:
*Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum spindle speed;
*Recommend oil coolant for Stainless Steels and Heat Resistance Alloys;
*Recommend using a non-contact measuring device to avoid damaging the precision tip point;
*Decrease both spindle speed and feed rate proportionally in case of chattering.
Download 2: hrc55 4 flute long neck flat end mill File

Related Product

Related Post

Get Your Custom Milling Tool Guide

Fill out the form below to receive SAMHO’s complete product catalog.