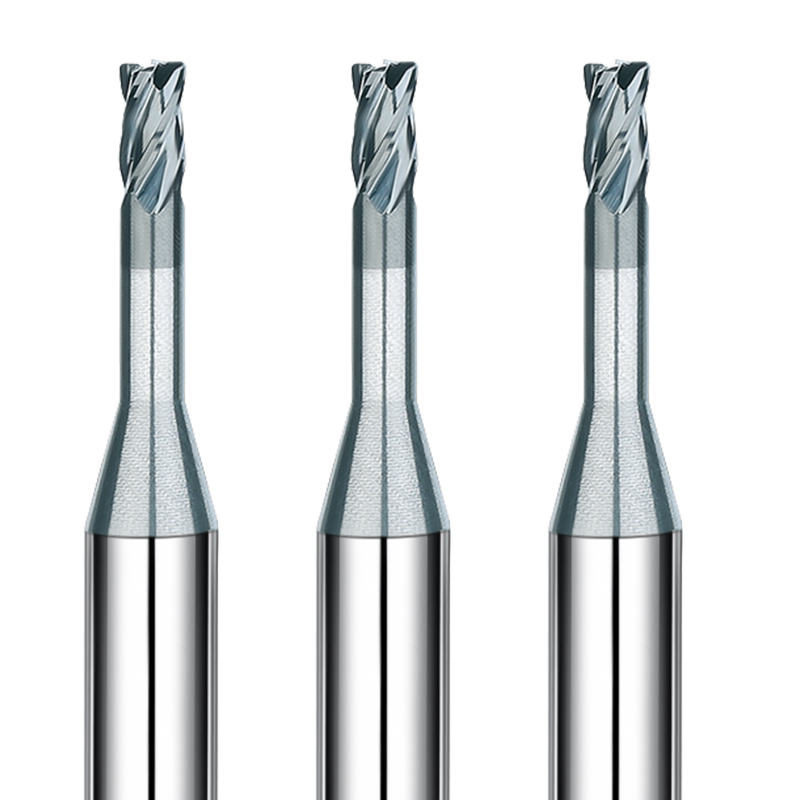
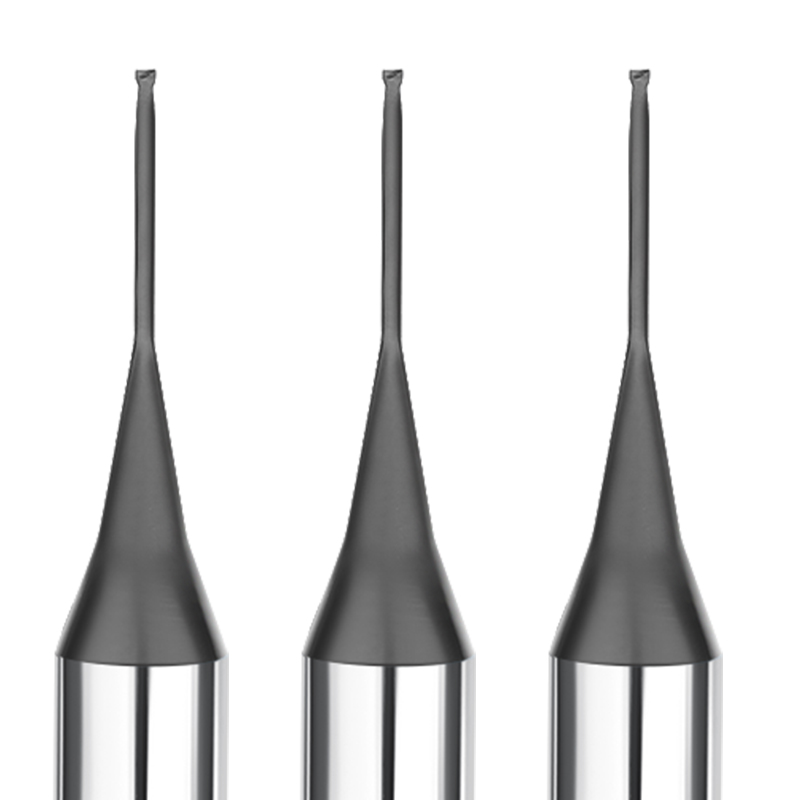
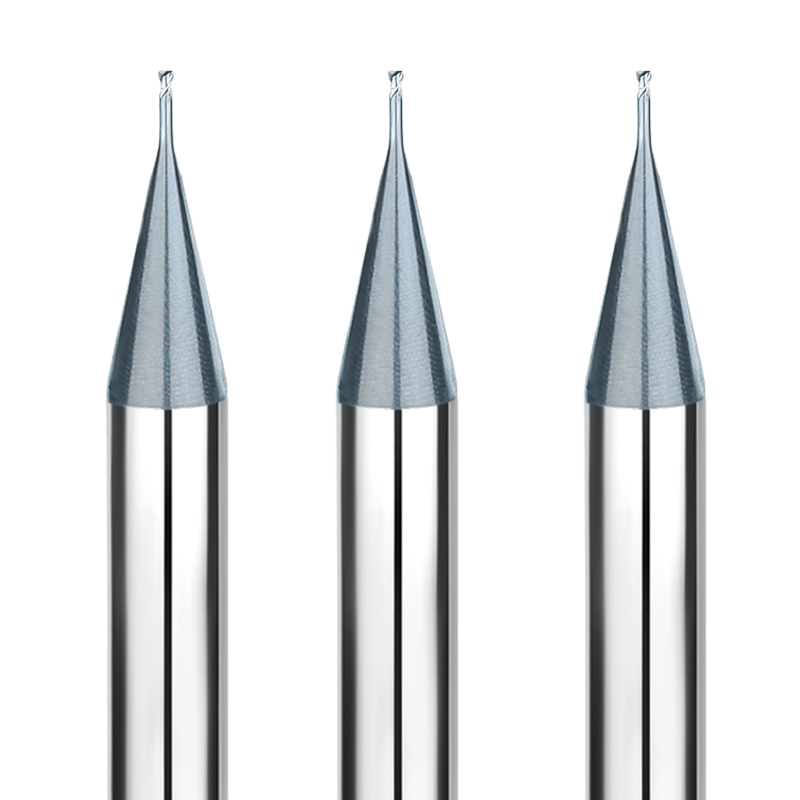
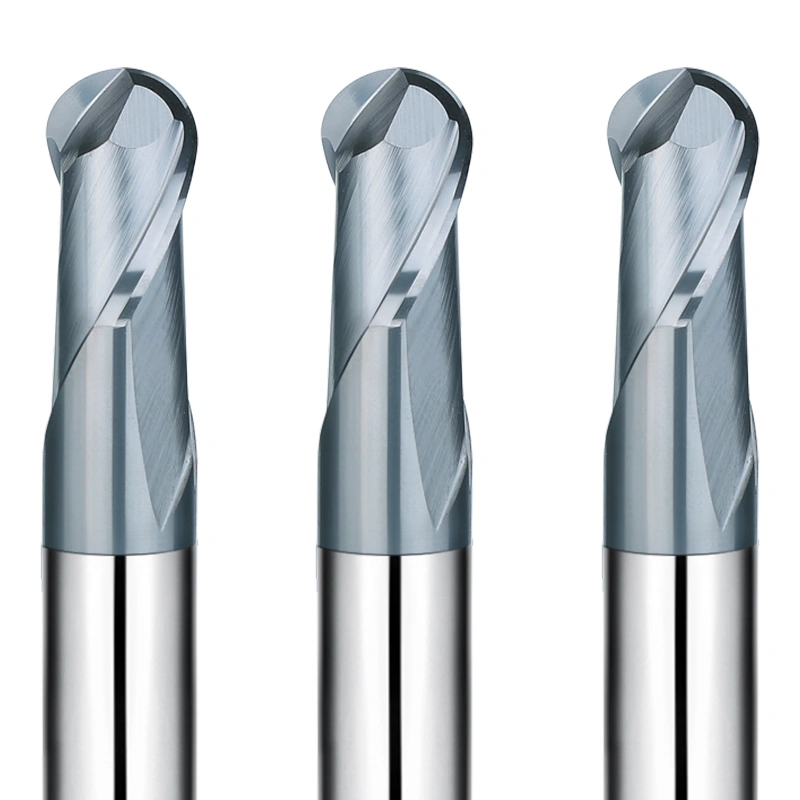
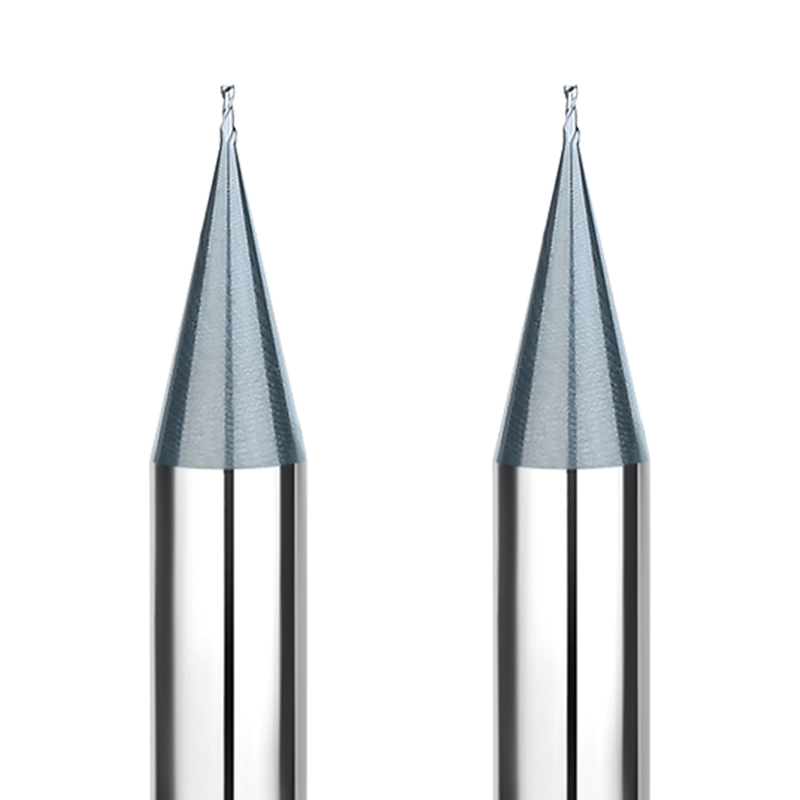
In high-precision electrode manufacturing and mold making, tool reach and surface quality are critical. The SAMHO DLC-Coated Long Neck Series is engineered to provide stable, mirror-like finishes in deep-cavity applications where standard tools fail due to vibration or material smearing.
Advanced Technical Features
- DLC Coating: The Anti-Stick Solution for Copper & Aluminum
The Diamond-Like Carbon (DLC) coating acts as a solid lubricant with exceptional surface hardness and anti-adhesion properties:
- Prevents Chip Welding: Eliminates built-up edge (BUE) even during high-speed dry cutting
- Enhances Tool Life: Reduces friction-induced heat, maintaining edge sharpness for longer production runs
- Long Neck Design for Interference-Free Deep Milling
Extended neck geometry provides superior clearance for deep cavity and narrow features:
- Reach Deep Contours: Ideal for complex 3D mold cores and undercuts
- Maintain Rigidity: Optimized neck-to-diameter ratios ensure stable cutting with minimal deflection
- 2-Flute Ball Nose Profile for Smooth 3D Surfaces
Precision-ground spherical tip ensures seamless 3-axis contouring:
- Seamless Transitions: Smooth finishing of curved surfaces and freeform geometries
- Reduced Polishing: High-quality finish minimizes secondary manual polishing
- Mirror-Polished Flutes for Rapid Chip Evacuation
Mirror-polished flute surfaces provide high-lubricity design:
- Excellent Chip Flow: Prevents clogging in deep slots and narrow pockets
- Dimensional Accuracy: Minimizes cutting forces that cause errors in ductile materials
Target Applications & Industries
Applications:
- Copper Electrode Machining: Precision finishing of high-purity red copper EDM electrodes
- Aluminum Mold Making: High-speed profiling of 3D cavities and complex pockets
- Medical & Electronics: Machining intricate plastic and non-ferrous components
Industries:
- Mold & Die
- Automotive
- Medical Device
- Aerospace
Field-Tested Cutting Parameters
SAMHO provides tested cutting data for red copper, aluminum, and resins to optimize CNC efficiency:
- Reduce Setup Time: Performance optimized out of the box
- Minimize Trial-and-Error: Stable, repeatable results across batches
- Protect the Tool: Follow 3xD calculation guidelines for long overhang conditions
Internal Links: → Products / End Mill / Ball Nose End Mill / Blog
Why Source Wholesale from SAMHO?
- 74+ Models in Stock: From micro-scale precision to standard deep milling tools
- Factory-Direct Pricing: Significant savings for bulk procurement and international distributors
- OEM Customization: Tailored neck lengths, specialized coatings, and custom geometries available
Recommended Materials for Machining (Highly Recommended: ⭐️ | Recommended: ⭕️ | Suggested: ◯)
| Category |
Work Material |
Grade |
| DIE STEEL |
Carbon steels (S45C/S55C) |
|
|
Alloy steels (SK/SCM/SUS) |
|
|
Prehardened steels (NAK/HPM) |
|
|
Hardened steels (~55/~60/~70HRC) |
|
| SPECIAL MATERIAL |
Aluminum alloys |
⭕️ |
|
Graphite |
|
|
Copper |
⭐️ |
|
Plastics |
⭕️ |
|
Carbon fiber |
|
|
Titanium alloys |
|
|
Heat resistant alloys |
|
|
Cemented carbide |
|
|
Hard brittle (non-metallic) material |
|
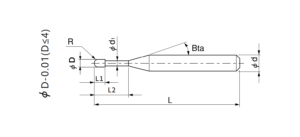
Total 74 models
| Model Number |
Outside Diameter |
Length Of Cut |
Effective Length |
Shank Taper Angle |
Overall Length |
Number Of Flutes |
Shank Diameter |
In Stock |
| SHDLR2-002005 |
R0.1 |
0.16 |
0.5 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-002010 |
R0.1 |
0.16 |
1 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-002020 |
R0.1 |
0.16 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-003010 |
R0.15 |
0.25 |
1 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-003020 |
R0.15 |
0.25 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-003030 |
R0.15 |
0.25 |
3 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-003040 |
R0.15 |
0.25 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-003060 |
R0.15 |
0.25 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-004010 |
R0.2 |
0.32 |
1 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-004020 |
R0.2 |
0.32 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-004030 |
R0.2 |
0.32 |
3 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-004040 |
R0.2 |
0.32 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-004060 |
R0.2 |
0.32 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-005020 |
R0.25 |
0.4 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-005030 |
R0.25 |
0.4 |
3 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-005040 |
R0.25 |
0.4 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-005060 |
R0.25 |
0.4 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-005080 |
R0.25 |
0.4 |
8 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-006020 |
R0.3 |
0.45 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-006030 |
R0.3 |
0.45 |
3 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-006040 |
R0.3 |
0.45 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-006060 |
R0.3 |
0.45 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-006080 |
R0.3 |
0.45 |
8 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-006080 |
R0.3 |
0.45 |
10 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-008020 |
R0.4 |
0.6 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-008040 |
R0.4 |
0.6 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-008060 |
R0.4 |
0.6 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-008080 |
R0.4 |
0.6 |
8 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-008100 |
R0.4 |
0.6 |
10 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-010020 |
R0.5 |
0.8 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-010030 |
R0.5 |
0.8 |
3 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-010040 |
R0.5 |
0.8 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-010060 |
R0.5 |
0.8 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-010080 |
R0.5 |
0.8 |
8 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-010100 |
R0.5 |
0.8 |
10 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-010120 |
R0.5 |
0.8 |
12 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-010140 |
R0.5 |
0.8 |
14 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-010160 |
R0.5 |
0.8 |
16 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-015040 |
R0.75 |
1.2 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-015060 |
R0.75 |
1.2 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-015080 |
R0.75 |
1.2 |
8 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-015100 |
R0.75 |
1.2 |
10 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-015120 |
R0.75 |
1.2 |
12 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-015140 |
R0.75 |
1.2 |
14 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-015160 |
R0.75 |
1.2 |
16 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-020040 |
R1 |
1.6 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-020060 |
R1 |
1.6 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-020080 |
R1 |
1.6 |
8 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-020100 |
R1 |
1.6 |
10 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-020120 |
R1 |
1.6 |
12 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-020160 |
R1 |
1.6 |
16 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-020040-6 |
R1 |
1.6 |
4 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-020060-6 |
R1 |
1.6 |
6 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-020080-6 |
R1 |
1.6 |
8 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-020100-6 |
R1 |
1.6 |
10 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-020120-6 |
R1 |
1.6 |
12 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-020140-6 |
R1 |
1.6 |
16 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-030060 |
R1.5 |
2.4 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-030080 |
R1.5 |
2.4 |
8 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-030100 |
R1.5 |
2.4 |
10 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-030120 |
R1.5 |
2.4 |
12 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-030160 |
R1.5 |
2.4 |
16 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-030200 |
R1.5 |
2.4 |
20 |
12° |
50 |
2 |
4 |
○ |
| SHDLR2-030060-6 |
R1.5 |
2.4 |
6 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-030080-6 |
R1.5 |
2.4 |
8 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-030100-6 |
R1.5 |
2.4 |
10 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-030120-6 |
R1.5 |
2.4 |
12 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-030160-6 |
R1.5 |
2.4 |
16 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-030200-6 |
R1.5 |
2.4 |
20 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-040080-6 |
R2 |
4 |
8 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-040100-6 |
R2 |
4 |
10 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-040120-6 |
R2 |
4 |
12 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-040160-6 |
R2 |
4 |
16 |
12° |
60 |
2 |
6 |
○ |
| SHDLR2-040200-6 |
R2 |
4 |
20 |
12° |
60 |
2 |
6 |
○ |
Milling Conditions
| Work Material |
Oxygen-free & Copper |
| (mm)Diameter |
(mm)Effective Length |
(min-1)Speed |
(mm/min)Feed |
Ap(mm)Axial depth |
Ae(mm)Radidl depth |
| D 0.2 |
0.5 |
30000 |
150 |
0.006 |
0.006 |
| D 0.2 |
1 |
30000 |
100 |
0.006 |
0.006 |
| D 0.2 |
1.5 |
30000 |
100 |
0.003 |
0.003 |
| D 0.3 |
1 |
28000 |
300 |
0.01 |
0.01 |
| D 0.3 |
1.5 |
28000 |
300 |
0.008 |
0.008 |
| D 0.3 |
2 |
24000 |
200 |
0.007 |
0.007 |
| D 0.3 |
3 |
20000 |
100 |
0.005 |
0.005 |
| D 0.3 |
3 |
20000 |
100 |
0.005 |
0.005 |
| D 0.4 |
1 |
24000 |
600 |
0.01 |
0.02 |
| D 0.4 |
2 |
24000 |
400 |
0.01 |
0.015 |
| D 0.4 |
3 |
20000 |
300 |
0.008 |
0.008 |
| D 0.4 |
4 |
18000 |
150 |
0.005 |
0.005 |
| D 0.4 |
4 |
18000 |
150 |
0.005 |
0.005 |
| D 0.5 |
1 |
22000 |
800 |
0.015 |
0.02 |
| D 0.5 |
2 |
22000 |
800 |
0.015 |
0.02 |
| D 0.5 |
4 |
18000 |
400 |
0.01 |
0.01 |
| D 0.5 |
6 |
14000 |
200 |
0.005 |
0.005 |
| D 0.5 |
8 |
14000 |
100 |
0.003 |
0.003 |
| D 0.6 |
2 |
20000 |
1000 |
0.02 |
0.02 |
| D 0.6 |
4 |
17000 |
500 |
0.015 |
0.02 |
| D 0.6 |
6 |
15000 |
400 |
0.01 |
0.02 |
| D 0.6 |
8 |
14000 |
200 |
0.005 |
0.01 |
| D 0.6 |
8 |
14000 |
200 |
0.005 |
0.01 |
| D 0.6 |
8 |
14000 |
200 |
0.005 |
0.01 |
| D 0.8 |
2 |
18000 |
1200 |
0.03 |
0.03 |
| D 0.8 |
4 |
18000 |
800 |
0.02 |
0.03 |
| D 0.8 |
6 |
14000 |
500 |
0.01 |
0.03 |
| D 0.8 |
8 |
14000 |
300 |
0.01 |
0.02 |
| D 0.8 |
8 |
14000 |
300 |
0.01 |
0.02 |
| D 1.0 |
2 |
16000 |
1500 |
0.03 |
0.05 |
| D 1.0 |
4 |
16000 |
1300 |
0.03 |
0.05 |
| D 1.0 |
4 |
16000 |
1300 |
0.03 |
0.05 |
| D 1.0 |
6 |
16000 |
1000 |
0.03 |
0.05 |
| D 1.0 |
8 |
14000 |
500 |
0.02 |
0.04 |
| D 1.0 |
10 |
12000 |
400 |
0.01 |
0.03 |
| D 1.0 |
12 |
11000 |
300 |
0.01 |
0.02 |
| D 1.0 |
14 |
10000 |
250 |
0.01 |
0.02 |
| D 1.0 |
16 |
10000 |
200 |
0.01 |
0.01 |
| D 1.5 |
4 |
16000 |
1600 |
0.03 |
0.06 |
| D 1.5 |
6 |
16000 |
1400 |
0.03 |
0.06 |
| D 1.5 |
8 |
16000 |
1200 |
0.03 |
0.05 |
| D 1.5 |
10 |
12000 |
800 |
0.02 |
0.05 |
| D 1.5 |
12 |
10000 |
500 |
0.02 |
0.04 |
| D 1.5 |
14 |
10000 |
400 |
0.01 |
0.03 |
| D 1.5 |
16 |
8000 |
300 |
0.01 |
0.03 |
| D 2 |
4 |
16000 |
1800 |
0.03 |
0.06 |
| D 2 |
6 |
15000 |
1800 |
0.03 |
0.06 |
| D 2 |
8 |
15000 |
1800 |
0.03 |
0.06 |
| D 2 |
10 |
15000 |
1800 |
0.03 |
0.06 |
| D 2 |
12 |
13000 |
1600 |
0.03 |
0.06 |
| D 2 |
16 |
10000 |
1000 |
0.02 |
0.06 |
| D 2 |
4 |
16000 |
1800 |
0.03 |
0.06 |
| D 2 |
6 |
15000 |
1800 |
0.03 |
0.06 |
| D 2 |
8 |
15000 |
1800 |
0.03 |
0.06 |
| D 2 |
10 |
15000 |
1800 |
0.03 |
0.06 |
| D 2 |
12 |
13000 |
1600 |
0.03 |
0.06 |
| D 2 |
16 |
10000 |
1000 |
0.02 |
0.06 |
| D 3 |
6 |
14000 |
2200 |
0.05 |
0.07 |
| D 3 |
8 |
14000 |
2200 |
0.05 |
0.07 |
| D 3 |
10 |
14000 |
2200 |
0.05 |
0.07 |
| D 3 |
12 |
14000 |
2200 |
0.04 |
0.07 |
| D 3 |
16 |
12000 |
2000 |
0.03 |
0.07 |
| D 3 |
20 |
11000 |
1000 |
0.03 |
0.07 |
| D 3 |
6 |
14000 |
2200 |
0.05 |
0.07 |
| D 3 |
8 |
14000 |
2200 |
0.05 |
0.07 |
| D 3 |
10 |
14000 |
2200 |
0.05 |
0.07 |
| D 3 |
12 |
14000 |
2200 |
0.04 |
0.07 |
| D 3 |
16 |
12000 |
2000 |
0.03 |
0.07 |
| D 3 |
20 |
11000 |
1000 |
0.03 |
0.07 |
| D 4 |
8 |
14000 |
2400 |
0.05 |
0.07 |
| D 4 |
10 |
14000 |
2400 |
0.05 |
0.07 |
| D 4 |
12 |
14000 |
2400 |
0.05 |
0.07 |
| D 4 |
16 |
14000 |
2200 |
0.04 |
0.07 |
| D 4 |
20 |
12000 |
2000 |
0.04 |
0.07 |
Note:
*Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum spindle speed;
*Recommend oil coolant for Stainless Steels and Heat Resistance Alloys.