
Last month, a German client returned a batch of broken tools used on quenched and tempered 4140 alloy steel. Less than 20 minutes into production, the spindle load spiked abnormally. Nearly the entire batch of 16mm tools snapped at the end-tooth transition zone. The on-site engineer was baffled: “We followed the catalog feed and speed charts to the letter, so why couldn’t these tools survive half a shift?”
We have seen this exact scenario play out for over fifteen years.
When dealing with premature edge chipping or sudden tool breakage with steel roughing end mills, many shops immediately blame the carbide substrate or coating adhesion. However, after auditing hundreds of failed setups, we know the root cause is rarely defective raw material. Instead, premature failure almost always stems from a disconnect in process dynamics under aggressive metal removal conditions:
- Thermal shock cracking: Rapid temperature swings from flood coolant during interrupted cuts generate micro-cracks along the wavy flute troughs of coated tools.
- Entry and rigidity mismatch: Aggressive ramp angles and unmanaged corner engagement create radial shock loads that instantly shear cutting teeth.
- Compounded dynamic runout: Overhangs past 3D combined with minor collet runout force a single tooth to take the entire feed load at high RPM.
The true goal of roughing is safely removing maximum material volume per minute, not testing a tool’s ultimate breaking point. On your shop floor, do you have machines where—despite conservative settings—you still hear that sudden, costly snap?
Premature Chipping Caused by Entry and Toolpath Strategy Errors
When troubleshooting early tool failure, engineers often tweak surface footage and chip load first. However, our field inspections across hundreds of machine shops show that over 40% of tool failures happen during initial entry. High Metal Removal Rates (MRR) require smart entry techniques rather than aggressive plunges. Even when a CAM toolpath looks clean on screen, ignoring dynamic machine acceleration and cutting resistance spikes will shatter the tool’s serrated teeth.
Efficient roughing toolpaths balance dynamic tool rigidity with chip evacuation space. When skinning rough forgings, plunging into deep cavities, or cutting sharp corners, sudden engagement spikes destroy load symmetry. Unless you optimize entry ramps and cornering feeds at the programming stage, no solid carbide substrate can survive continuous shock loads.
Instantaneous Damage to the End Teeth of Steel Roughing End Mills Caused by Vertical Plunging or Excessive Helical Entry Angles
While troubleshooting P20 mold base roughing at a large injection mold facility, we found their CAM programmers applied a uniform 5° helical ramp across all tools. While standard flat end mills might tolerate this angle, running large-diameter steel roughing end mills into deep pockets causes catastrophic failure. Because the center web lacks center-cutting geometry, steep ramp angles turn the center core into a dead zone that crushes against hardened steel.
Microscopic inspection of the failed tools revealed severe secondary flank chipping and metal adhesion. For tough alloy steels, keep your helical entry ramp between 1.5° and 2.5°, paired with a helical radius at least 70% of the cutter diameter. For narrow slots where ramping is impossible, pre-drilling a pilot hole is far safer than forcing the tool to plunge vertically.
Sudden Increase in Cutting Width at Corners Overloads Rough End Mill Side Edges
We recently assisted a North American automotive supplier experiencing frequent corner breakages with a 12 mm rough end mill in forged steel brackets. Real-time spindle monitoring revealed steady loads on straight cuts, followed by a 300% current spike inside 90° internal corners. Traditional offset toolpaths instantly expanded the tool engagement angle from 40° to 180°, generating massive shear stress on the flutes.
Eliminating this localized overload does not require slowing cycle times across the entire part. We transitioned the client to dynamic trochoidal milling, using small arc retractions and adaptive radial stepovers to maintain a constant tool engagement angle. On legacy CNC machines that cannot process dynamic paths, adding a 50% feed deceleration within 1 to 2 tool diameters of every corner prevents edge blowout.
Edge Overload Caused by Confusing Roughing vs Finishing End Mill Toolpath Boundaries
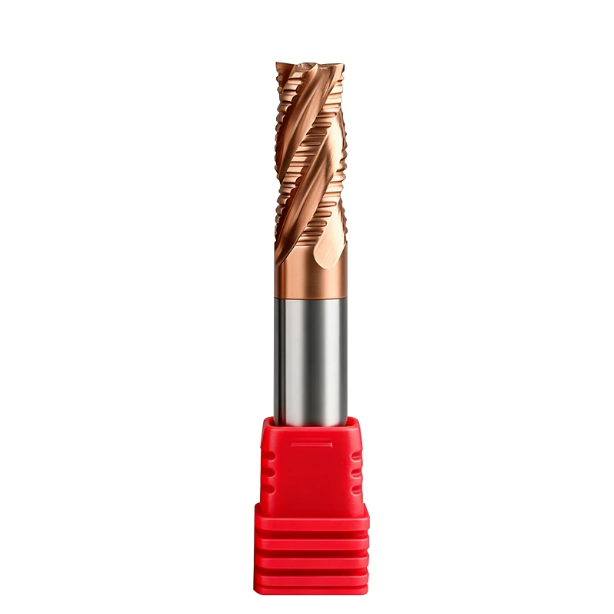
We regularly see two shop-floor extremes: operators running finish cutters as roughers to skip a tool change, or leaving a tiny 0.05 mm skin for a rougher to clean up. Evaluating a roughing vs finishing end mill highlights clear geometric differences. Roughing cutters use knuckle serrations and thick core diameters to fracture chips and handle shock, while finishing mills utilize razor-sharp edges and narrow flutes designed exclusively for wall straightness and fine finishes.
Pushing a finishing mill through heavy stock causes instant edge fracture as packed chips choke the shallow flutes. Conversely, using a roughing tool on minimal stock forces the wavy crests to rub and slide rather than shear metal cleanly. This friction generates work hardening and rapidly anneals the cutting edge. For reliable tool life, leave a consistent 0.3 mm to 0.5 mm radial stock allowance for the finishing pass.
Improper Cooling and Thermal Crack Control
Managing cutting heat is often the invisible deciding factor in overall tool longevity. When visiting machine shops in Europe and the US, we often see operators instinctively blast coolant nozzles upon seeing sparks. However, this reaction is counterproductive. Interrupted cutting cycles teeth through intense heat expansion followed by instant quenching outside the cut, and irregular coolant delivery creates destructive thermal shock.
Effective thermal management balances microscopic stress while clearing hot chips instantly. When cutting temperatures swing by hundreds of degrees per second, the thermal expansion mismatch between the carbide substrate and the PVD coating widens drastically. Once thermal fatigue exceeds the grain boundary strength, irreversible coating delamination and micro-cracking occur, quickly escalating into edge fracture.
Severe Thermal Shock Delamination on Roughing End Mills for Steel Caused by Intermittent Emulsion Application
While optimizing 4340 alloy steel roughing for a British gear manufacturer, we noticed tools suffered severe flank chipping within 30 minutes. Although external emulsion was running, high spindle speeds and deep flutes created an air barrier that deflected the coolant. This produced an intermittent wet-dry state on the roughing end mills for steel, which were designed specifically for high-temperature dry cuts.
Under an electron microscope, the failed tools showed dense comb cracks perpendicular to the cutting edge alongside delaminated TiAlSiN coating. For heavy interrupted steel cuts, we advise shutting off external flood coolant entirely. Instead, use dry air blasts at 90+ PSI (0.6 MPa) or Minimum Quantity Lubrication (MQL) to evacuate chips. Carrying heat away inside the chip stabilizes the solid carbide substrate.
Chip Entanglement and Secondary Crushing with Carbide Bullnose End Mills in Deep Slot Roughing
When roughing deep blind pockets, many programmers prefer carbide bullnose end mills for their robust corner strength. However, without dedicated chip clearing, the corner radius quickly turns into a dangerous heat trap. In a recent mold steel troubleshooting job, the absence of high-pressure through-spindle air caused hot chips to pack tightly into the slot bottom, repeatedly crushing against the corner radius.
This chip recutting in a confined zone easily pushed local temperatures above 1650°F (900°C), compromising the tool’s red hardness and micro-annealing the carbide substrate. Stripped of its hardness, the radiused edge suffered plastic deformation and chipped out instantly. If your machine lacks high-pressure through-spindle air or coolant, reduce your radial stepover (Ae) and run multi-step air blasts to prevent chip packing.
Clamping Rigidity and Uncontrolled Radial Runout
When roughing tools break, operators often blame speed rates or raw material hardness while overlooking the toolholder interface. Roughing steel routinely generates thousands of Newtons of cutting force. Any minute taper backlash or holder deflection is magnified exponentially at thousands of RPM. Your toolholder taper fit, clamping force, and gauge length define the true dynamic rigidity of the entire setup.
When runout enters the equation, balanced multi-flute cutting disappears. The total cutting load shifts abruptly onto a single cutting edge. Even worse, microscopic runout triggers severe forced vibration and regenerative chatter. This subjects the carbide flutes to relentless mechanical shock alongside high shear loads, directly accelerating catastrophic tool fracture.
ER Collet Runout Exceeding 0.0004″ Causes Single-Tooth Overload in Steel Roughing End Mills
Last year, we troubleshot an ongoing breakage issue on 42CrMo4 forged steel for a German heavy equipment builder. Their four-flute steel roughing end mills were failing randomly. Dial indicator checks revealed that their worn ER32 collets had over 0.0007″ (0.018 mm) of dynamic runout at the tool tip. Rather than four teeth sharing a uniform 0.003″ chip load, one tooth took over 0.005″ while the others idled.
This unbalanced loading forced the overloaded tooth to micro-chip almost immediately. Once that leading edge chipped, cutting resistance spiked and snapped the entire tool within seconds. For heavy roughing in tough steels, we mandate keeping total runout at the tool tip under 0.0002″ (0.005 mm). Swapping aged ER collets for high-torque hydraulic or milling chucks dramatically boosts tool life without touching your feed rates.
Severe Harmonic Resonance and Wave-Edge Chipping in Long-Reach Rough End Mill Setups
Deep-cavity clearing in injection molds often forces programmers to run a rough end mill at gauge lengths exceeding 4D or 5D. When running long overhangs in standard set-screw or collet chucks, spindles frequently hit resonant frequencies that generate a piercing squeal and heavy chatter marks on sidewalls. This high-frequency deflection quickly exceeds the bending strength of the carbide shank.
Knuckle-profile roughers rely on wave crests to shear and troughs to break chips, creating natural cyclic stress shifts. Under heavy resonance, severe stress concentrates right at the transition between crest and trough, chipping the wave peaks and fatiguing the carbide core. For deep pockets with long reach, switch to heavy-metal anti-vibration shanks or shrink-fit holders, and adjust spindle RPM to dodge harmonic frequencies.
Mismatch Between Tool Geometry and Workpiece Material Hardness
During shop-floor visits, we frequently see a “one-size-fits-all” approach: stocking a generic cutter to rough everything from soft mild steel to pre-hardened die blocks. While machinists often blame “unmachinable” material, our manufacturing data proves that most premature failures stem from micro-geometry mismatches. Material yield strength, ductility, and thermal conductivity dictate how cutting forces distribute across the shear zone.
A tool’s core diameter, flute volume, rake angle, and edge prep determine where cutting forces go and how heat escapes. Cutting hardened steel requires reinforced edge prep to survive extreme compressive stress, while roughing soft, gummy alloys demands generous flute clearance to stop chip welding. Ignoring material hardness and microstructure forces the cutter into unnatural stress states that trigger rapid tool breakdown.
Incorrect Selection of Corner Radius and Flute Geometry for Carbide Bullnose End Mills in Hardened Mold Steel Roughing
While helping a European die shop rough 1.2379 (D2) tool steel at HRC 48–52, we resolved an issue where their tools chipped out within 15 minutes. They were using carbide bullnose end mills designed with thin cores and tight R0.5 (0.020″) corner radii. That small radius concentrated massive cutting forces onto a tiny contact zone, while the narrow web lacked the torsional rigidity to survive heavy cutting loads.
Hardened steels generate extreme radial cutting resistance, making sharp corner radii vulnerable to instantaneous shear chipping. For roughing steels above HRC 45, we recommend stepping up to a heavy-duty core ratio of 65%+ and expanding the corner radius to R1.5 or R2.0 (0.060″–0.080″). The larger radius spreads primary cutting loads and improves heat transfer, while a slight negative rake with a reinforced T-land prevents catastrophic edge fracture.
Chip Packing Issues When Using the Same Roughing End Mills for Steel on Soft Alloys vs. Heat-Treated Steels
On a multi-facility valve manufacturing line, a client reported frequent tool stalling and catastrophic breakage. They ran the same roughing end mills for steel (engineered for 4140 pre-hardened stock) on 304 stainless and low-carbon steel. Our failure analysis showed the flutes were packed solid with extruded chips. Heavy built-up edge (BUE) and friction welding caused the cutters to snap under excessive torsional load.
Heat-treated steels yield short, brittle chips that clear easily through fine-pitch wavy profiles with neutral rake angles. Conversely, low-carbon and austenitic stainless steels produce tough, continuous ribbons that instantly clog narrow flutes. For gummy, high-elongation materials, run a coarse-pitch knuckle profile with a 10°–12° positive rake and mirror-polished flutes so continuous chips evacuate without heat buildup or material welding.
Insufficient Supply Chain Collaboration and On-Site Process Validation
After analyzing toolpaths, thermal shock, setup rigidity, and geometry, we must address an overlooked factor: technical collaboration with your tooling source. In many machine shops, purchasing simply compares catalog list prices, while operators toss broken end mills into the scrap bin. This disconnect hides the root causes of tool failure and causes shops to miss major opportunities to lower their true cost per part.
Unlocking maximum tool life requires validating the cutter against machine dynamics, workholding rigidity, and actual workpiece hardness. When batch roughing runs hit sudden breakage, tweaking feeds and speeds at the control rarely solves the root issue. Establishing open data exchange between tooling design engineers and machine operators is the fastest way to eliminate unpredictable tool breakage.
Collaborating with a Professional CNC Roughing End Mill Supplier on Failure Analysis and Parameter Compensation
When premature chipping hits your production line, emailing a blurry photo of a broken shank rarely yields useful answers. As tool manufacturers, we look for comprehensive diagnostic data: fracture surface topography (fatigue striations vs. brittle shear), edge hone wear uniformity, and spindle load spikes on entry. Working with a specialized cnc roughing end mill supplier helps you turn shop-floor data into targeted cutter modifications.
If you are milling rough forgings or deep mold cavities with frequent edge micro-chipping, share your spindle load spikes alongside high-magnification wear photos with us. In most cases, we do not need to overhaul your cutting parameters. Widening the edge hone or T-land by 0.0008″ (0.02 mm) or applying a thermal-resistant nanocomposite PVD coating dramatically boosts impact toughness while maintaining high metal removal rates.
Establishing Quantitative Tool Life Management Standards for Rough End Mill Setups
High-volume production lines rarely let a tool run until it snaps, yet many job shops still rely on operator ear and chip color to gauge tool wear. For a heavy-duty rough end mill, relying on guesswork frequently causes scrapped parts and damaged spindles. We advise setting hard replacement limits based on measurable thresholds: maximum uniform flank wear (VB) of 0.008″–0.012″ (0.2–0.3 mm) or a 15% increase in steady-state spindle load.
If you run high-value steel forgings or large mold blocks, track the full wear progression across three to five test tools. Record cut distance and in-cut time across the initial, steady-state, and accelerated wear phases to map an accurate wear curve. Programming this threshold into your CNC controller ensures safe tool changes before catastrophic breakage, protecting raw parts while keeping the carbide core intact for re-grinding.






