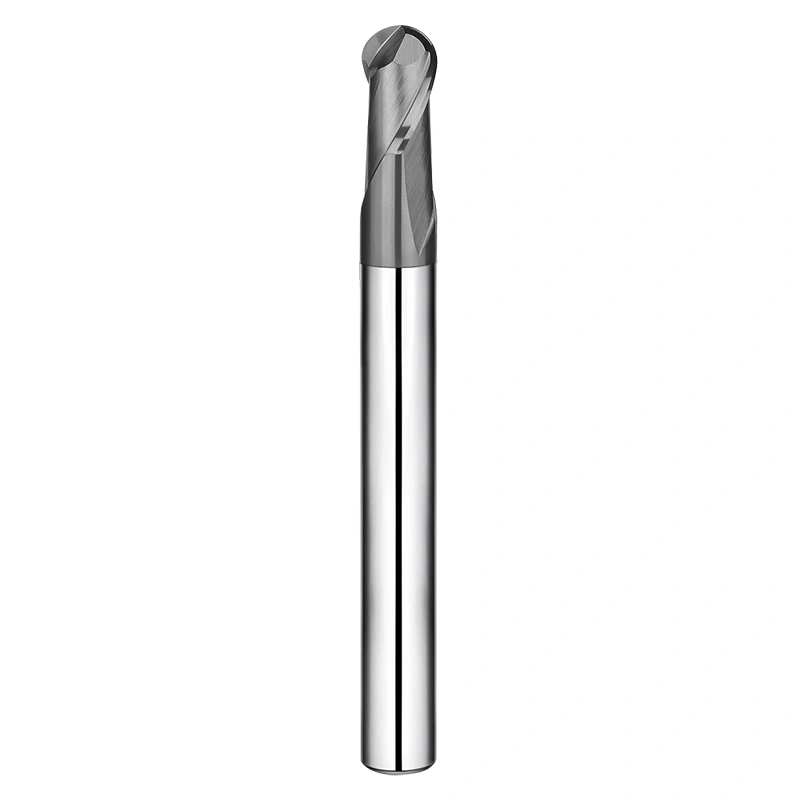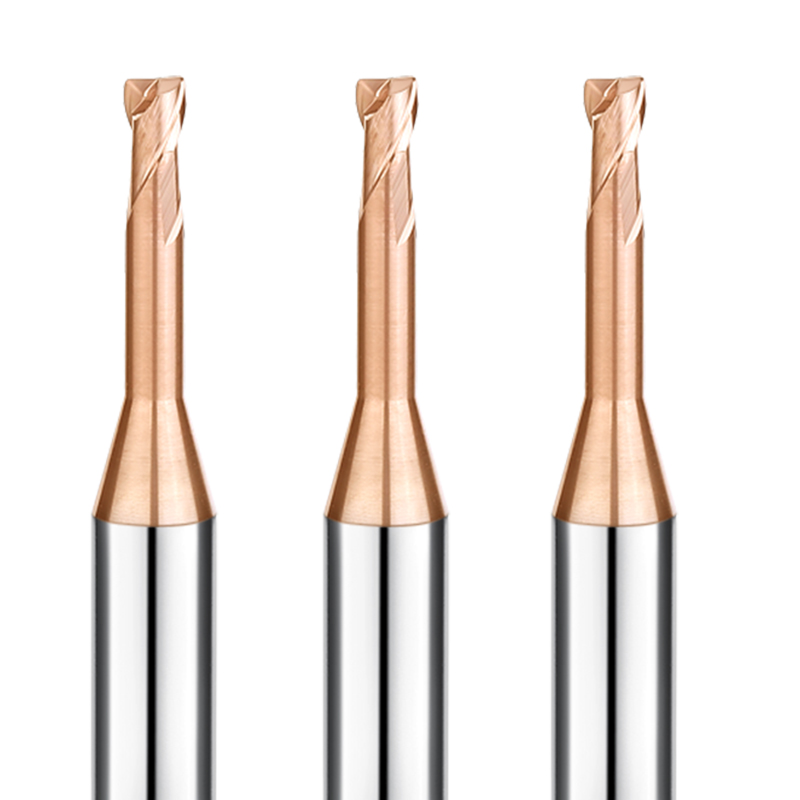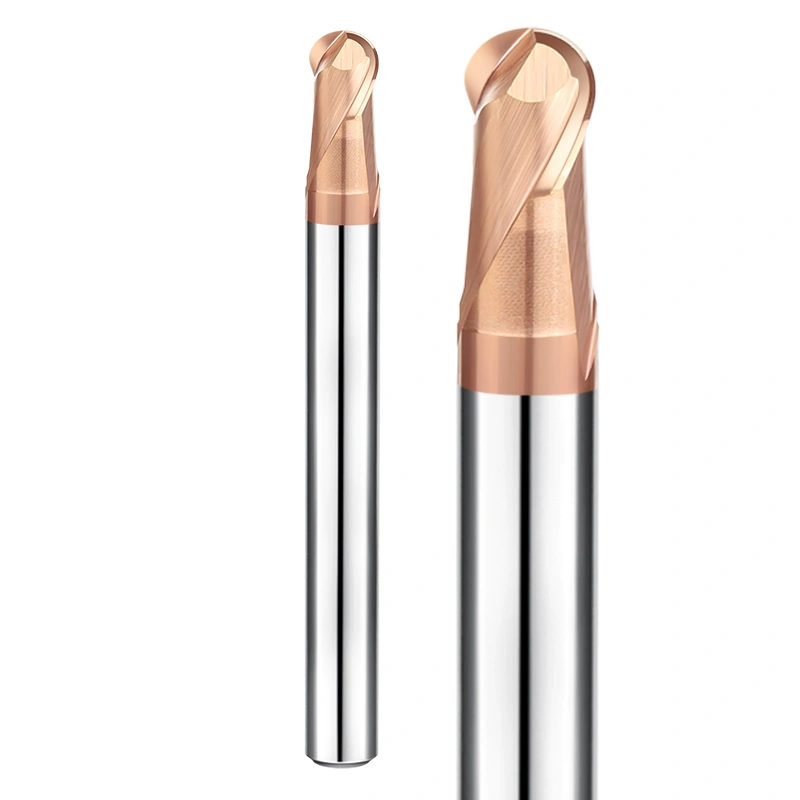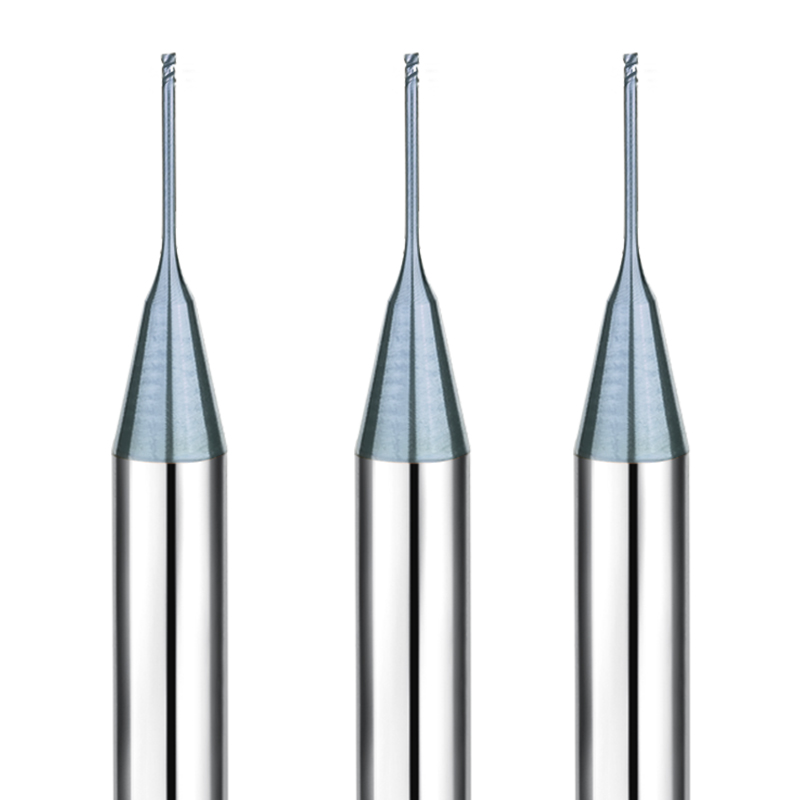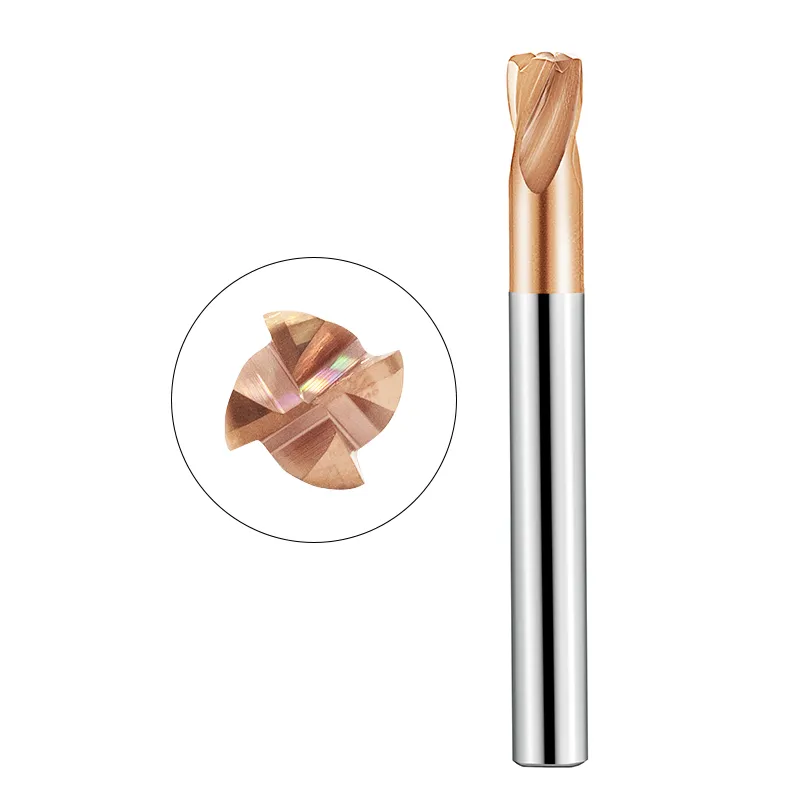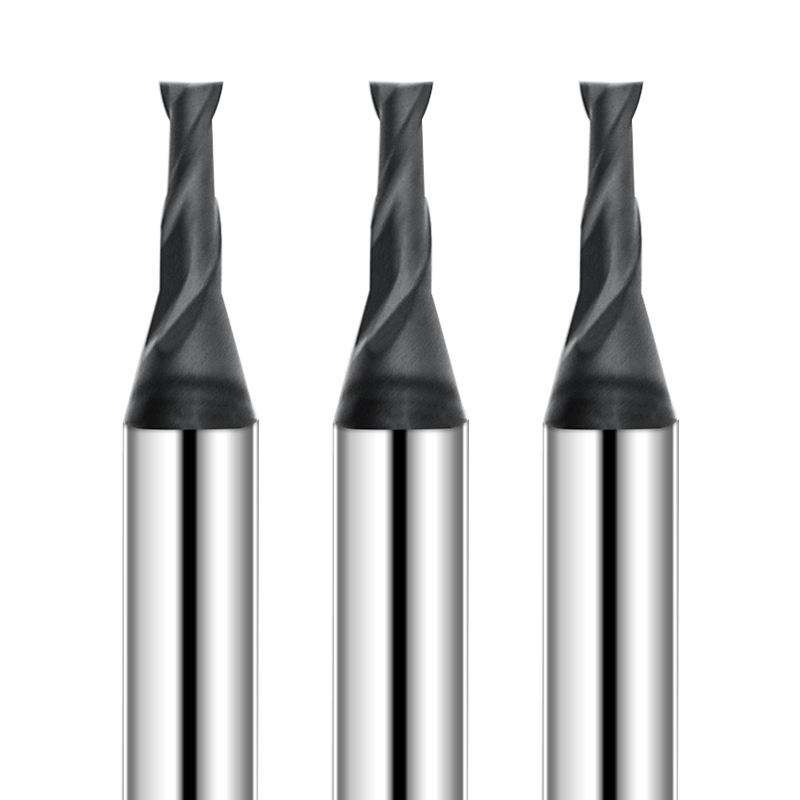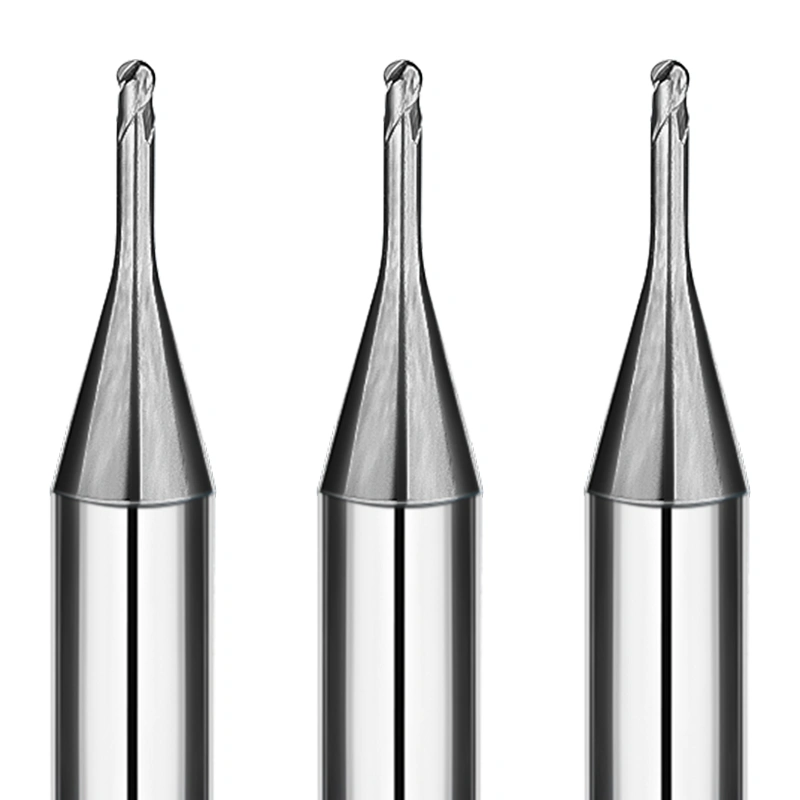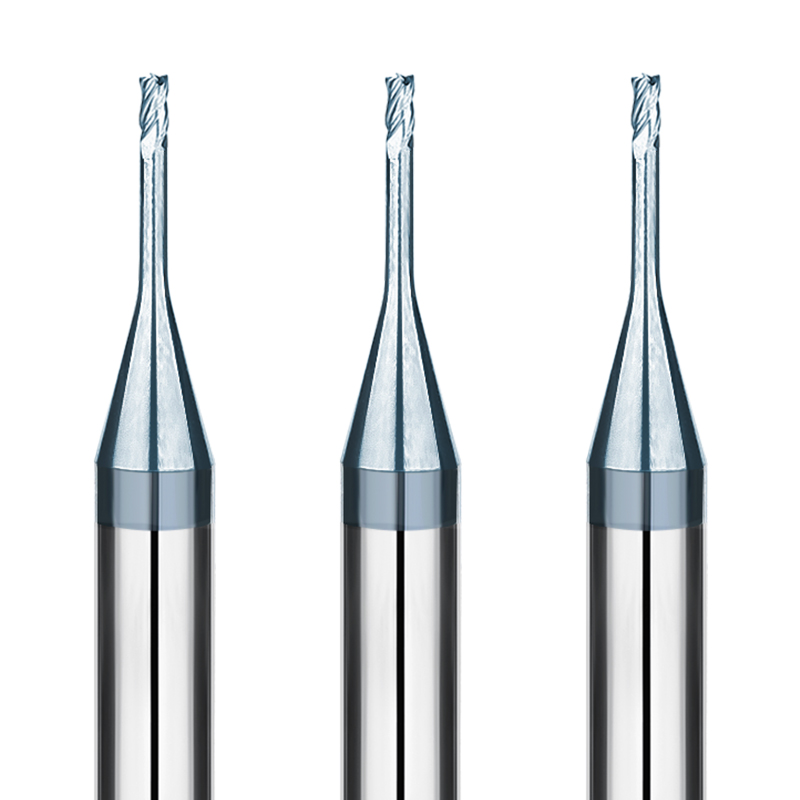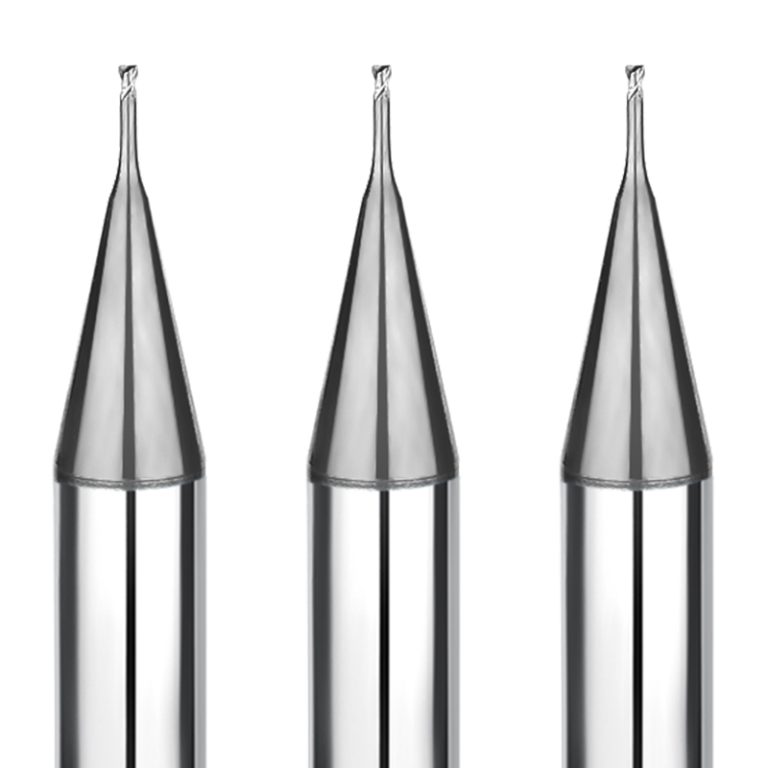
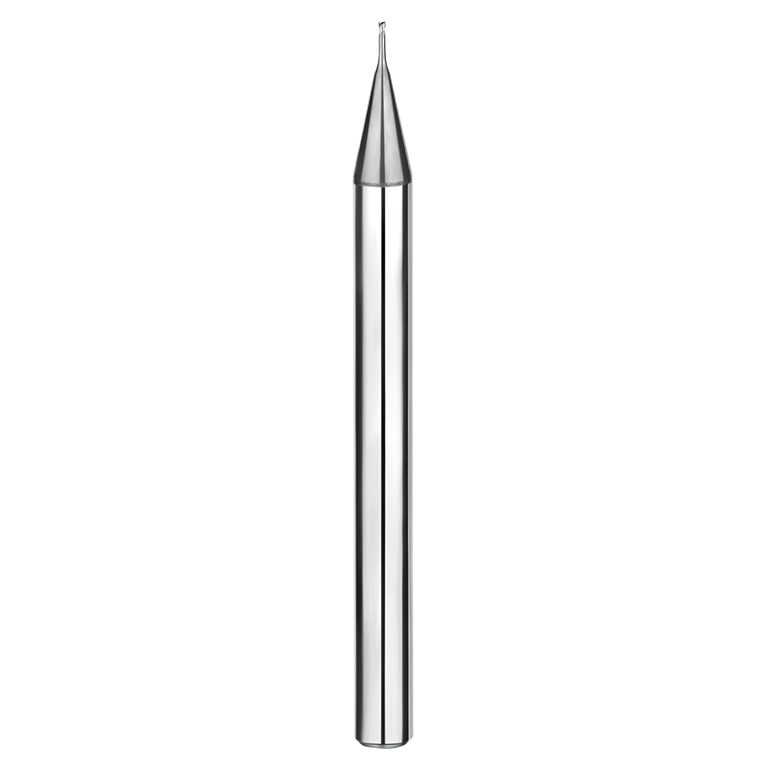
end mill for copper end mill for copper

End Mill for Copper 2 Flute Long Neck Corner Radius End Mill

SAMHO DLC-Coated 2-Flute Rounded Corner Long-Neck End Mill–A High-Efficiency Precision Machining Solution for Copper

Do not let tool sticking, built-up edge, or unstable machining reduce your production yield. SAMHO non-ferrous metal cutting tools are engineered for high-precision copper machining. They also deliver stable performance on aluminum alloys and resin materials, making them suitable for demanding CNC production environments.

With advanced DLC low-friction coating technology and a long-neck clearance design, this tool effectively reduces material adhesion during copper machining. It improves cutting stability, enhances surface finish quality, and extends consistent tool life.

Applicable Materials:Optimized for precision copper parts and electrode machining. Also suitable for aluminum alloys and resin materials.
Stable Cutting Performance:The DLC coating reduces friction and minimizes built-up edge formation. This improves cutting consistency during continuous machining operations.

The SAMHO DLC-coated 2-flute long neck rounded end mill (D0.3R0.05–D2R0.2 mm) is engineered for high-precision machining of non-ferrous metals. It is especially effective for finishing copper, and it also performs well in aluminum alloys and resin materials.

The tool features a low-friction DLC coating that significantly reduces tool adhesion and built-up edge during copper machining. This improves cutting stability and surface quality.


Advanced Technical Features

High-Adhesion DLC Coating for Stable, Long Tool Life

This tool uses proprietary low-friction DLC coating technology designed for non-ferrous metal machining. It delivers strong wear resistance and excellent anti-adhesion performance.

  • High Wear Resistance: Maintains sharp cutting edges during continuous machining of copper and other non-ferrous materials.
  • Strong Anti-Adhesion Performance: Effectively reduces built-up edge (BUE) and material sticking during copper cutting, improving tool stability and tool life.

Long Neck Design with Rounded Cutting Edge for Deep and Complex Machining

The long neck structure combined with a rounded edge geometry improves accessibility and cutting stability in demanding applications.

  • Deep Cavity Machining Capability: Suitable for deep cavity machining in copper, precision molds, and complex 3D geometries.
  • Rounded Edge Design: Reduces edge stress concentration, improves anti-chipping performance, and enhances surface finish quality.
  • Wide Material Application: Suitable for copper, aluminum alloys, and resin materials.

2-Flute Design for Efficient Chip Evacuation and Stable Cutting

The optimized 2-flute geometry is designed for stable and efficient non-ferrous metal machining.

  • Efficient Chip Removal: Quickly evacuates chips to reduce re-cutting and improve surface quality.
  • Stable Cutting Performance: Reduces cutting forces and vibration for consistent machining results.
  • Better Thermal Control: Limits heat buildup and helps prevent thermal deformation in copper workpieces.

Ultra-Fine Grain Carbide with High-Precision Manufacturing

Made from high-strength ultra-fine grain carbide and produced with precision grinding technology.

  • Consistent Dimensional Accuracy: Tight tolerance control ensures stable batch-to-batch consistency.
  • Improved Tool Toughness: Enhances fracture resistance for demanding CNC machining conditions.
  • High Machining Reliability: Suitable for precision copper electrode machining and fine component production.

Target Applications & Industries

This series of DLC-coated 2-flute corner radius long neck end mills is designed for precision non-ferrous metal machining. It is especially effective for stable and efficient cutting of copper. It also performs well in aluminum alloys and resin materials.

This tool is widely used in:

  • Machining of precision copper components and electrodes
  • Deep cavity, narrow slot, and complex mold processing
  • Precision milling of aluminum alloy structural parts
  • Machining of resin and engineering plastic components
  • High-precision contouring and 3D surface machining

Why Choose SAMHO as Your Wholesale Partner?

SAMHO specializes in high-performance cutting tools for non-ferrous metal machining. We provide stable, high-consistency tooling solutions for copper, aluminum alloys, and resin materials. Our products are designed to support both OEM and ODM manufacturing requirements.

Optimized for Non-Ferrous Metal Machining
The low-friction DLC coating reduces material adhesion and built-up edge during copper machining. This improves cutting stability and surface finish quality.

Long-Neck Clearance Design
The long-neck structure is ideal for deep cavities, narrow slots, and complex geometries. It improves tool reach and machining flexibility.

Ultra-High Precision Manufacturing
Shank diameter is controlled within 0 to +0.003 mm tolerance. This ensures stable clamping performance and consistent batch quality.

OEM / ODM Support
We provide customized tooling solutions based on specific machine setups and machining requirements.
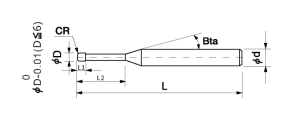
Recommended Materials for Machining (Highly Recommended: ⭐️ | Recommended: ⭕️ | Suggested: )

Category Work Material Grade
DIE STEEL Carbon steels (S45C/S55C)
Alloy steels (SK/SCM/SUS)
Prehardened steels (NAK/HPM)
Hardened steels (~55/~60/~70HRC)
SPECIAL MATERIAL Aluminum alloys ⭕️
Graphite
Copper ⭐️
Plastics ⭕️
Carbon fiber
Titanium alloys
Heat resistant alloys
Cemented carbide
Hard brittle (non-metallic) material

long neck corner radius end mill

Total 71 models

Model Number Outside Diameter Length Of Cut Effective Length Radius Shank Taper Angle Overall Length Number Of Flutes Shank Diameter In Stock
SHDLSR2-003005010 D0.3 0.25 1 R0.05 12° 50 2 4
SHDLSR2-003005020 D0.3 0.25 2 R0.05 12° 50 2 4
SHDLSR2-004005010 D0.4 0.32 1 R0.05 12° 50 2 4
SHDLSR2-004005020 D0.4 0.32 2 R0.05 12° 50 2 4
SHDLSR2-004005030 D0.4 0.32 3 R0.05 12° 50 2 4
SHDLSR2-004005040 D0.4 0.32 4 R0.05 12° 50 2 4
SHDLSR2-00401010 D0.4 0.32 1 R0.1 12° 50 2 4
SHDLSR2-00401020 D0.4 0.32 2 R0.1 12° 50 2 4
SHDLSR2-00401030 D0.4 0.32 3 R0.1 12° 50 2 4
SHDLSR2-00401040 D0.4 0.32 4 R0.1 12° 50 2 4
SHDLSR2-005005010 D0.5 0.4 1 R0.05 12° 50 2 4
SHDLSR2-005005020 D0.5 0.4 2 R0.05 12° 50 2 4
SHDLSR2-005005030 D0.5 0.4 3 R0.05 12° 50 2 4
SHDLSR2-005005040 D0.5 0.4 4 R0.05 12° 50 2 4
SHDLSR2-00501010 D0.5 0.4 1 R0.1 12° 50 2 4
SHDLSR2-00501020 D0.5 0.4 2 R0.1 12° 50 2 4
SHDLSR2-00501030 D0.5 0.4 3 R0.1 12° 50 2 4
SHDLSR2-00501040 D0.5 0.4 4 R0.1 12° 50 2 4
SHDLSR2-006005020 D0.6 0.5 2 R0.05 12° 50 2 4
SHDLSR2-006005030 D0.6 0.5 3 R0.05 12° 50 2 4
SHDLSR2-006005040 D0.6 0.5 4 R0.05 12° 50 2 4
SHDLSR2-006005060 D0.6 0.5 6 R0.05 12° 50 2 4
SHDLSR2-00601020 D0.6 0.5 2 R0.1 12° 50 2 4
SHDLSR2-00601030 D0.6 0.5 3 R0.1 12° 50 2 4
SHDLSR2-00601040 D0.6 0.5 4 R0.1 12° 50 2 4
SHDLSR2-00601060 D0.6 0.5 6 R0.1 12° 50 2 4
SHDLSR2-008005020 D0.8 0.65 2 R0.05 12° 50 2 4
SHDLSR2-008005030 D0.8 0.65 3 R0.05 12° 50 2 4
SHDLSR2-008005040 D0.8 0.65 4 R0.05 12° 50 2 4
SHDLSR2-008005060 D0.8 0.65 6 R0.05 12° 50 2 4
SHDLSR2-008005080 D0.8 0.65 8 R0.05 12° 50 2 4
SHDLSR2-00801020 D0.8 0.65 2 R0.1 12° 50 2 4
SHDLSR2-00801030 D0.8 0.65 3 R0.1 12° 50 2 4
SHDLSR2-00801040 D0.8 0.65 4 R0.1 12° 50 2 4
SHDLSR2-00801060 D0.8 0.65 6 R0.1 12° 50 2 4
SHDLSR2-00801080 D0.8 0.65 8 R0.1 12° 50 2 4
SHDLSR2-00802020 D0.8 0.65 2 R0.2 12° 50 2 4
SHDLSR2-00802030 D0.8 0.65 3 R0.2 12° 50 2 4
SHDLSR2-00802040 D0.8 0.65 4 R0.2 12° 50 2 4
SHDLSR2-00802060 D0.8 0.65 6 R0.2 12° 50 2 4
SHDLSR2-00802080 D0.8 0.65 8 R0.2 12° 50 2 4
SHDLSR2-01001040 D1.0 1 4 R0.1 12° 50 2 4
SHDLSR2-01001060 D1.0 1 6 R0.1 12° 50 2 4
SHDLSR2-01001080 D1.0 1 8 R0.1 12° 50 2 4
SHDLSR2-01001100 D1.0 1 10 R0.1 12° 50 2 4
SHDLSR2-01001120 D1.0 1 12 R0.1 12° 50 2 4
SHDLSR2-01002040 D1.0 1 4 R0.2 12° 50 2 4
SHDLSR2-01002060 D1.0 1 6 R0.2 12° 50 2 4
SHDLSR2-01002080 D1.0 1 8 R0.2 12° 50 2 4
SHDLSR2-01002100 D1.0 1 10 R0.2 12° 50 2 4
SHDLSR2-01002120 D1.0 1 12 R0.2 12° 50 2 4
SHDLSR2-01501040 D1.5 1.5 4 R0.1 12° 50 2 4
SHDLSR2-01501060 D1.5 1.5 6 R0.1 12° 50 2 4
SHDLSR2-01501080 D1.5 1.5 8 R0.1 12° 50 2 4
SHDLSR2-01501100 D1.5 1.5 10 R0.1 12° 50 2 4
SHDLSR2-01501120 D1.5 1.5 12 R0.1 12° 50 2 4
SHDLSR2-01502040 D1.5 1.5 4 R0.2 12° 50 2 4
SHDLSR2-01502060 D1.5 1.5 6 R0.2 12° 50 2 4
SHDLSR2-01502080 D1.5 1.5 8 R0.2 12° 50 2 4
SHDLSR2-01502100 D1.5 1.5 10 R0.2 12° 50 2 4
SHDLSR2-01502120 D1.5 1.5 12 R0.2 12° 50 2 4
SHDLSR2-02001060 D2.0 2 6 R0.1 12° 50 2 4
SHDLSR2-02001080 D2.0 2 8 R0.1 12° 50 2 4
SHDLSR2-02001100 D2.0 2 10 R0.1 12° 50 2 4
SHDLSR2-02001120 D2.0 2 12 R0.1 12° 50 2 4
SHDLSR2-02001160 D2.0 2 16 R0.1 12° 50 2 4
SHDLSR2-02002060 D2.0 2 6 R0.2 12° 50 2 4
SHDLSR2-02002080 D2.0 2 8 R0.2 12° 50 2 4
SHDLSR2-02002100 D2.0 2 10 R0.2 12° 50 2 4
SHDLSR2-02002120 D2.0 2 12 R0.2 12° 50 2 4
SHDLSR2-02002160 D2.0 2 16 R0.2 12° 50 2 4

Contour Milling Parameters

Work Material Oxygen-free & Copper
(mm)Diameter (mm)Effective Length (min-1)Speed (mm/min)Feed
D0.3 1 30000 240
D0.3 2 30000 120
D0.4 1 26000 300
D0.4 2 24000 260
D0.4 3 22000 180
D0.4 4 18000 120
D0.4 1 26000 300
D0.4 2 24000 220
D0.4 3 22000 180
D0.4 4 18000 120
D0.5 1 20000 500
D0.5 2 18000 360
D0.5 4 16000 200
D0.5 6 14000 120
D0.5 1 20000 500
D0.5 2 18000 360
D0.5 4 16000 200
D0.5 6 14000 120
D0.6 2 16000 700
D0.6 4 13000 400
D0.6 6 11000 200
D0.6 8 10000 120
D0.6 2 16000 700
D0.6 4 13000 400
D0.6 6 11000 200
D0.6 8 10000 120
D0.8 2 16000 1200
D0.8 4 14000 800
D0.8 6 13000 600
D0.8 8 12000 300
D0.8 2 16000 1200
D0.8 4 14000 800
D0.8 6 13000 500
D0.8 8 12000 300
D0.8 2 16000 1200
D0.8 4 14000 800
D0.8 6 13000 500
D0.8 8 12000 300
D1.0 4 13000 1000
D1.0 6 11000 700
D1.0 8 10000 500
D1.0 10 8500 300
D1.0 10 8500 300
D1.0 4 13000 1000
D1.0 6 11000 700
D1.0 8 10000 500
D1.0 10 8500 300
D1.0 10 8500 300
D1.5 4 13000 1000
D1.5 6 10000 1000
D1.5 8 9000 800
D1.5 10 8500 700
D1.5 10 8500 700
D1.5 4 13000 1000
D1.5 6 10000 1000
D1.5 8 9000 800
D1.5 10 8500 700
D1.5 10 8500 700
D2 6 12000 1500
D2 8 11000 1000
D2 10 10000 900
D2 12 9000 800
D2 16 7500 600
D2 6 12000 1500
D2 8 11000 1000
D2 10 10000 900
D2 12 9000 800
D2 16 7500 600

Note:
Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum
spindle speed;

*Recommend oil coolant for Stainless Steels and Heat Resistance Alloys;

*Recommend using a non-contact measuring device to avoid damaging the precision tip point;

*Decrease both spindle speed and feed rate proportionally in case of chattering.

Download 2: End Mill for Copper 2 Flute Long Neck Corner Radius End Mill File

Related Product

Related Post

Get Your Custom Milling Tool Guide

Fill out the form below to receive SAMHO’s complete product catalog.