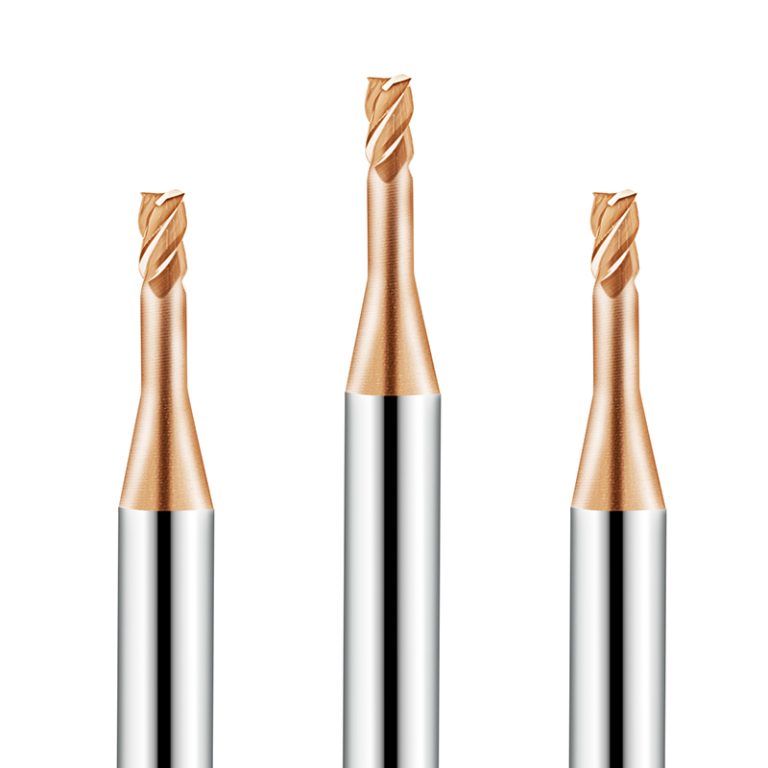
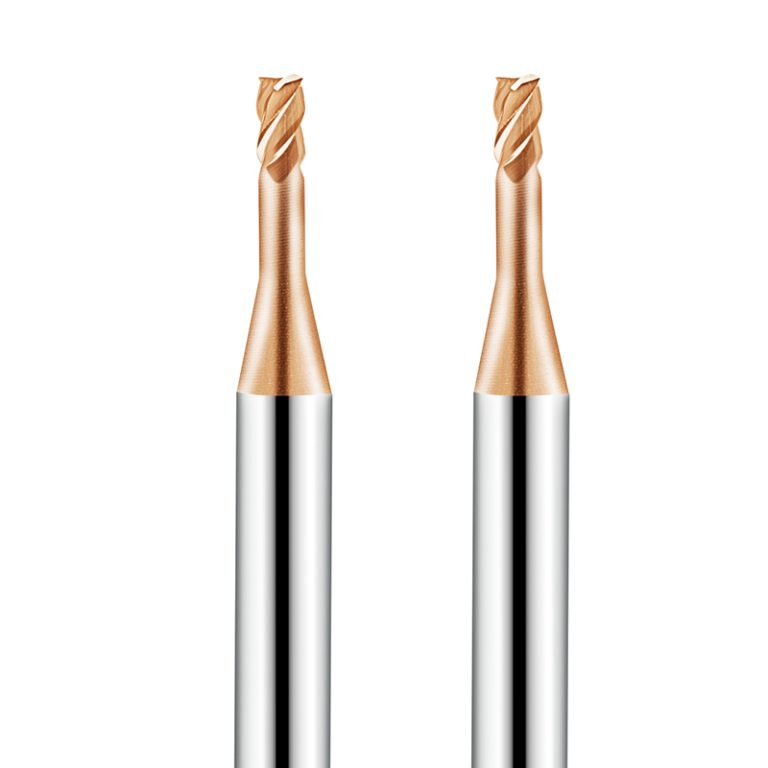
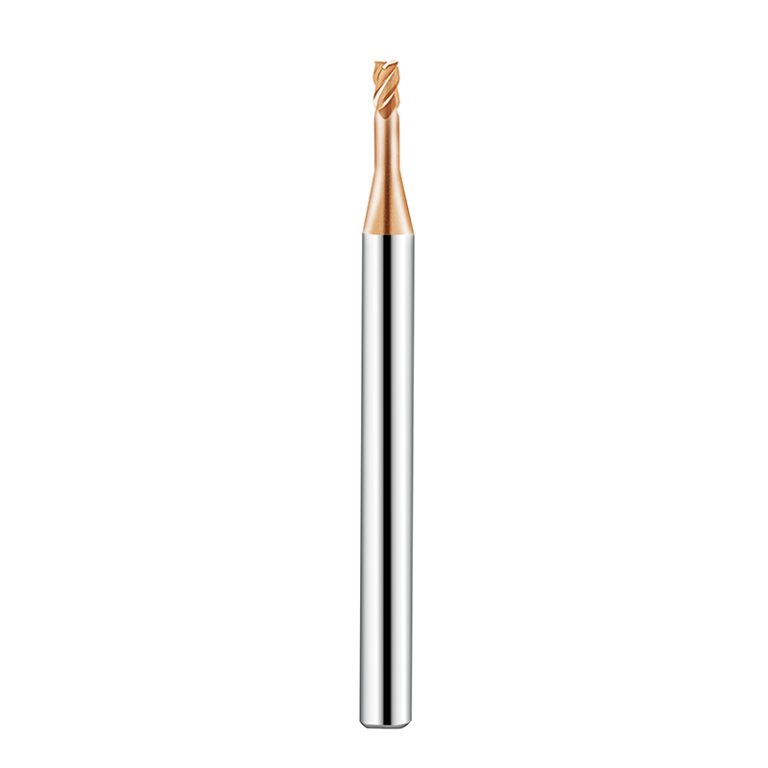
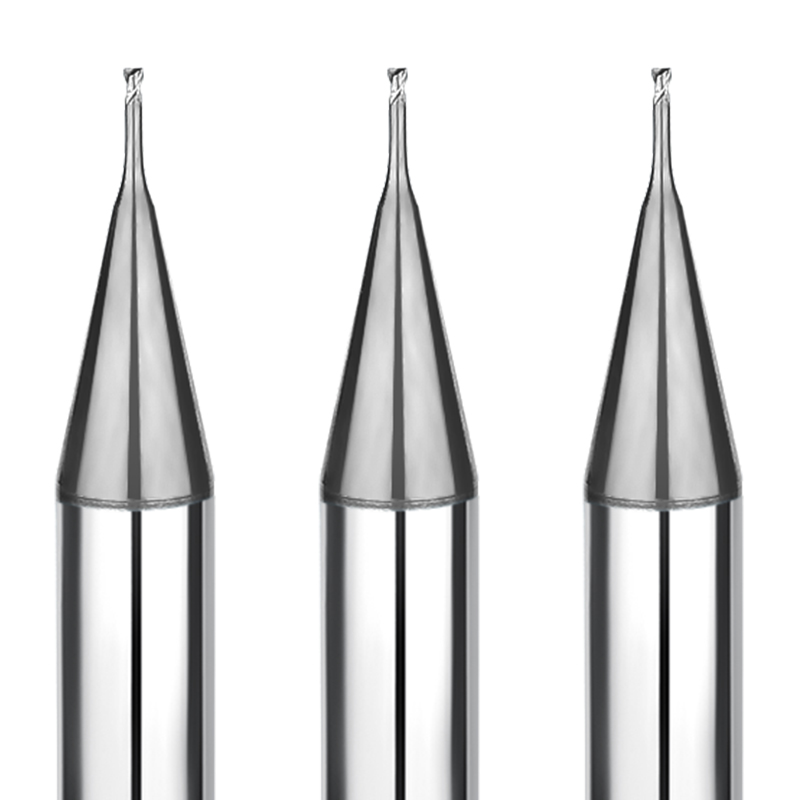
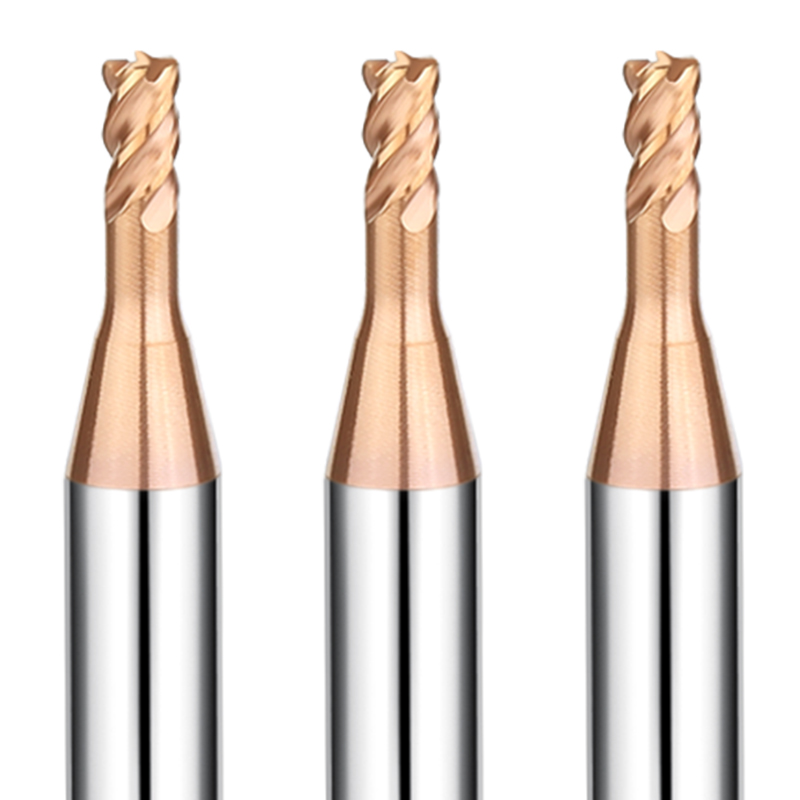
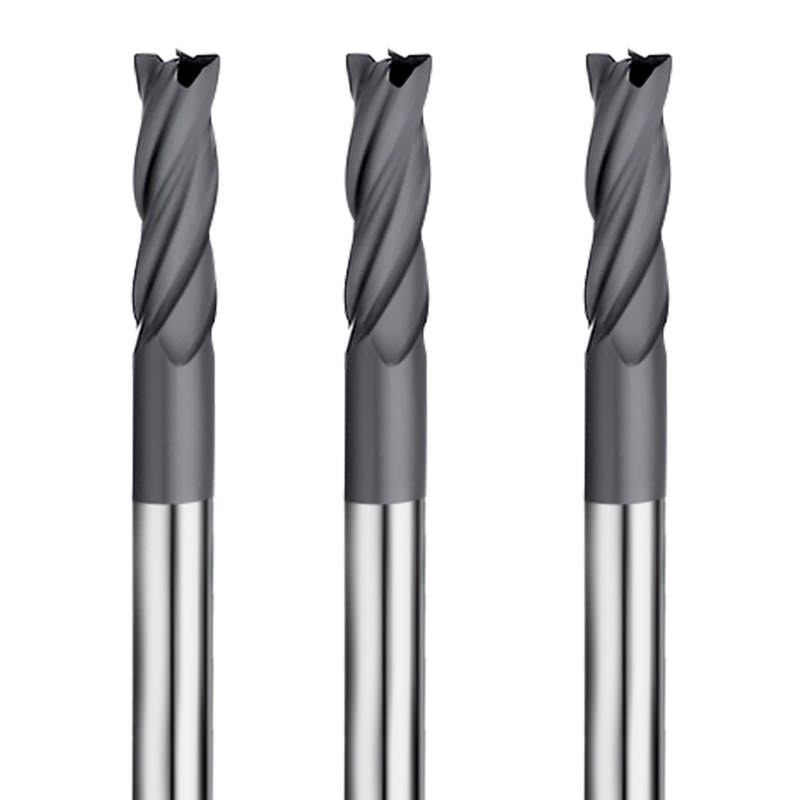
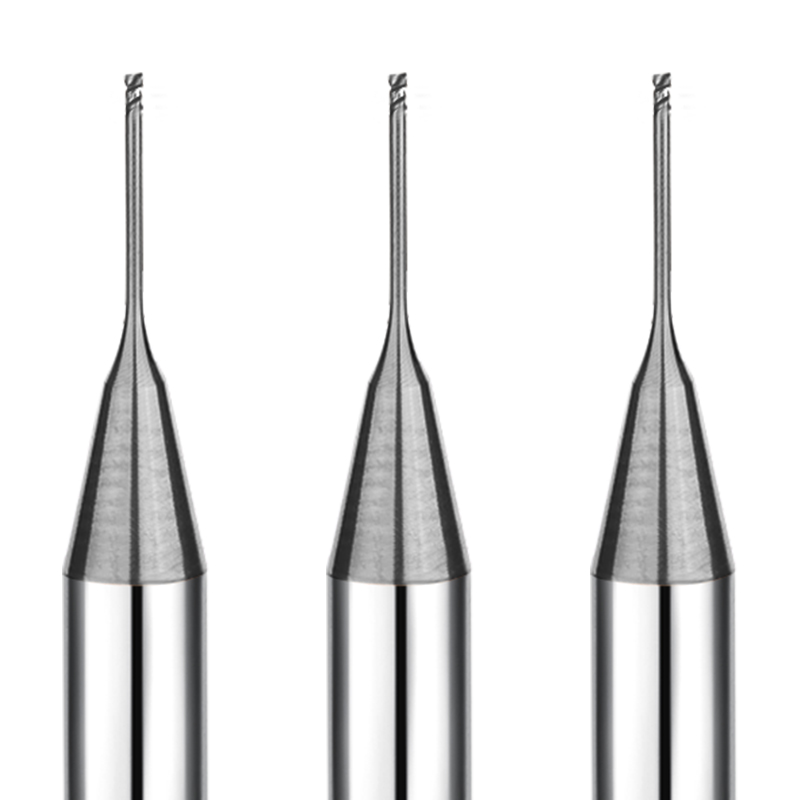
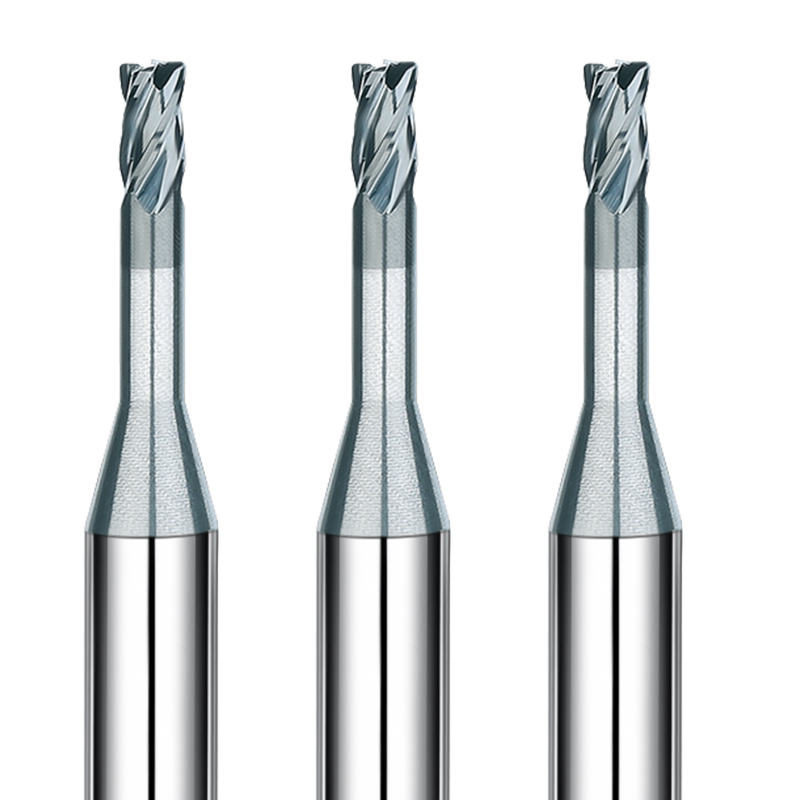
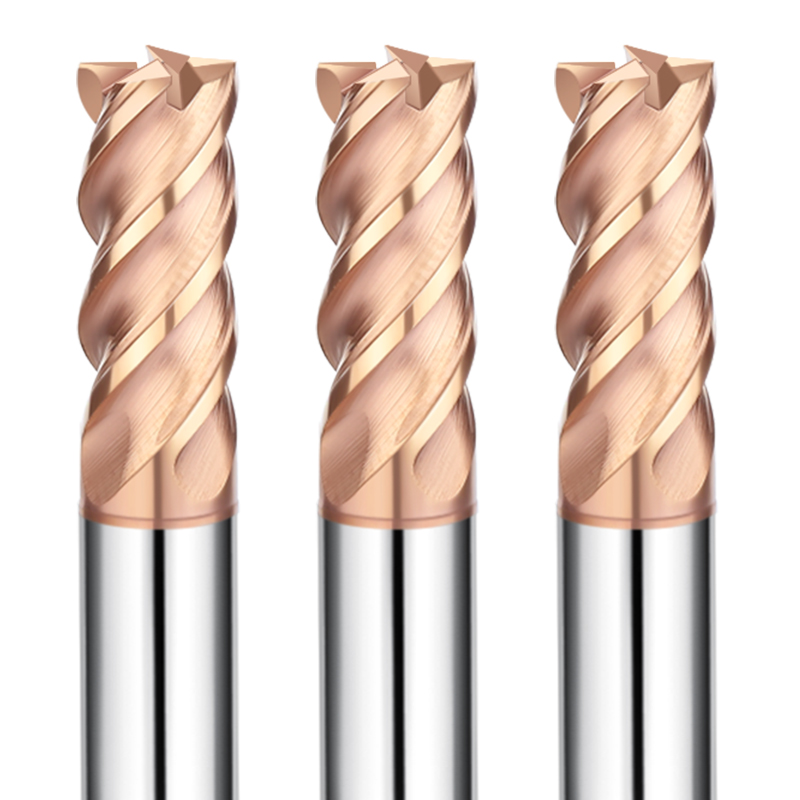
In the field of hardened steel machining, tool performance requirements are extremely demanding. Cutting tools must offer superior wear resistance, exceptional stability, and precise, efficient machining. SAMHO’s 4-flute long-neck flat end mill (D1-D3 mm), with a specialized coating, is engineered to meet these challenges. It is optimized for CNC operators, enabling precise and efficient machining of hardened steel while extending tool life and boosting productivity.
Advanced Technical Features
High-Adhesion Coating for Exceptional Tool Life
Our proprietary high-performance coating gives these tools extreme hardness and chemical inertness.
- Wear Resistance: Maintains a sharp cutting edge during continuous high-temperature machining of hardened steel.
- Micro-Chipping Prevention: Keeps the coating firmly bonded to the carbide substrate even in high-speed cutting conditions.
Cutting-Edge Geometry Designed for Precision Machining of Hardened Steel
- 4-Flute Long Neck Design: Ideal for precision CNC milling of deep cavities and high-hardness hardened steel workpieces.
- Optimized Tip and Neck Geometry: Reduces cutting load, minimizes heat buildup, and improves machining stability.
Efficient Cutting and Chip Evacuation
- Optimized Multi-Flute Geometry: Enhances chip evacuation, quickly clearing chips from the cutting zone.
- Reduced Cutting Heat: Minimizes the heat-affected zone, preventing cracking or deformation in hardened steel.
Ultra-Fine Grain Carbide Substrate and Precision Grinding
- Dimensional Accuracy: Strictly controlled within ±0.01 mm for consistent batch production.
- Exceptional Fracture Resistance: Significantly improves tool durability, especially for high-hardness, highly abrasive hardened steels.
Target Applications & Industries
This series of 4-flute long-neck flat end mills is specifically designed for precision CNC milling of hardened steel. It is highly versatile and widely applicable to:
- Precision milling of deep cavities in high-hardness hardened steel workpieces.
- Machining of mold cavities and complex structures with consistent accuracy.
- High-precision contour and internal angle transition machining, ideal for intricate designs.
- Batch production of workpieces that require exceptional wear resistance and dimensional precision.
Why Choose SAMHO as Your Wholesale Partner?
Custom OEM/ODM Solutions: Tailored to meet diverse client requirements.
Precisely Controlled Shank Diameter: Tolerances of 0–0.003 mm ensure stable and secure tool mounting.
Premium Materials and Coatings: Deliver exceptional wear resistance and extended tool life.
Engineered for Precision CNC Machining of Hardened Steel: High efficiency, low cutting heat, and consistently reliable precision.
Recommended Materials for Machining (Highly Recommended: ⭐️ | Recommended: ⭕️ | Suggested: ◯)
| Category |
Work Material |
Grade |
| DIE STEEL |
Carbon steels (S45C/S55C) |
|
|
Alloy steels (SK/SCM/SUS) |
|
|
Prehardened steels (NAK/HPM) |
|
|
Hardened steels (~55/~60/~70HRC) |
⭐️ |
| SPECIAL MATERIAL |
Aluminum alloys |
|
|
Graphite |
|
|
Copper |
|
|
Plastics |
|
|
Carbon fiber |
|
|
Titanium alloys |
|
|
Heat resistant alloys |
|
|
Cemented carbide |
|
|
Hard brittle (non-metallic) material |
|
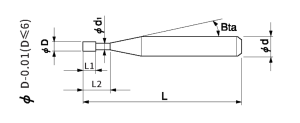
Total 26 models
| Model Number |
Outside Diameter |
Length Of Cut |
Effective Length |
Shank Taper Angle |
Overall Length |
Number Of Flutes |
Shank Diameter |
In Stock |
| SHHLS4-010040 |
1 |
1.5 |
4 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-010060 |
1 |
1.5 |
6 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-010080 |
1 |
1.5 |
8 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-010100 |
1 |
1.5 |
10 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-010160 |
1 |
1.5 |
16 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-015040 |
1.5 |
2.3 |
4 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-015060 |
1.5 |
2.3 |
6 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-015080 |
1.5 |
2.3 |
8 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-015100 |
1.5 |
2.3 |
10 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-015160 |
1.5 |
2.3 |
16 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-020060 |
2 |
3 |
6 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-020080 |
2 |
3 |
8 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-020100 |
2 |
3 |
10 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-020120 |
2 |
3 |
12 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-020160 |
2 |
3 |
16 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-020200 |
2 |
3 |
20 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-030080 |
3 |
4.5 |
8 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-030100 |
3 |
4.5 |
10 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-030120 |
3 |
4.5 |
12 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-030160 |
3 |
4.5 |
16 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-030200 |
3 |
4.5 |
20 |
12° |
50 |
4 |
4 |
○ |
| SHHLS4-030080-6 |
3 |
4.5 |
8 |
12° |
50 |
4 |
6 |
○ |
| SHHLS4-030100-6 |
3 |
4.5 |
10 |
12° |
50 |
4 |
6 |
○ |
| SHHLS4-030120-6 |
3 |
4.5 |
12 |
12° |
50 |
4 |
6 |
○ |
| SHHLS4-030160-6 |
3 |
4.5 |
16 |
12° |
50 |
4 |
6 |
○ |
| SHHLS4-030200-6 |
3 |
4.5 |
20 |
12° |
50 |
4 |
6 |
○ |
Contour Milling Parameters
| Work Material |
|
HRC48-55 hardened steel |
HRC56-62 hardened steel |
HRC63-70 hardened steel |
| Diameter |
Effective Length(mm) |
(min-1) Speed |
(mm/min) Feed |
(mm) Axial depth |
(mm) Radidl depth |
(min-1) Speed |
(mm/min) Feed |
(mm) Axial depth |
(mm) Radidl depth |
(min-1) Speed |
(mm/min) Feed |
(mm) Axial depth |
(mm) Radidl depth |
| 1 |
4 |
23000 |
900 |
0.04 |
0.5 |
18000 |
800 |
0.03 |
0.4 |
14000 |
500 |
0.02 |
0.3 |
| 1 |
6 |
18000 |
700 |
0.02 |
0.5 |
14000 |
600 |
0.01 |
0.4 |
10000 |
400 |
0.007 |
0.3 |
| 1 |
8 |
16000 |
600 |
0.02 |
0.5 |
12000 |
500 |
0.01 |
0.4 |
8000 |
340 |
0.005 |
0.3 |
| 1 |
10 |
14000 |
500 |
0.01 |
0.5 |
10000 |
400 |
0.007 |
0.4 |
6000 |
250 |
0.005 |
0.3 |
| 1 |
16 |
12000 |
320 |
0.006 |
0.5 |
9000 |
250 |
0.004 |
0.4 |
5500 |
150 |
0.003 |
0.3 |
| 1.5 |
4 |
20000 |
900 |
0.05 |
0.75 |
18000 |
800 |
0.04 |
0.6 |
4000 |
600 |
0.03 |
0.45 |
| 1.5 |
6 |
20000 |
800 |
0.04 |
0.75 |
18000 |
700 |
0.03 |
0.6 |
14000 |
500 |
0.02 |
0.45 |
| 1.5 |
8 |
18000 |
600 |
0.03 |
0.75 |
14000 |
600 |
0.03 |
0.6 |
10000 |
380 |
0.01 |
0.45 |
| 1.5 |
10 |
16000 |
500 |
0.03 |
0.75 |
14000 |
500 |
0.02 |
0.6 |
10000 |
350 |
0.01 |
0.45 |
| 1.5 |
16 |
10000 |
360 |
0.01 |
0.75 |
9000 |
300 |
0.007 |
0.6 |
6800 |
200 |
0.005 |
0.45 |
| 2 |
6 |
18000 |
900 |
0.06 |
1 |
15000 |
750 |
0.05 |
0.8 |
12000 |
600 |
0.03 |
0.6 |
| 2 |
8 |
16000 |
800 |
0.05 |
1 |
12000 |
600 |
0.04 |
0.8 |
9500 |
500 |
0.02 |
0.6 |
| 2 |
10 |
14000 |
700 |
0.05 |
1 |
12000 |
500 |
0.04 |
0.8 |
9500 |
450 |
0.02 |
0.6 |
| 2 |
12 |
12000 |
600 |
0.04 |
1 |
10000 |
500 |
0.03 |
0.8 |
8200 |
400 |
0.01 |
0.6 |
| 2 |
16 |
10000 |
500 |
0.03 |
1 |
9200 |
400 |
0.02 |
0.8 |
7500 |
340 |
0.007 |
0.6 |
| 2 |
20 |
9200 |
380 |
0.02 |
1 |
8500 |
340 |
0.01 |
0.8 |
6000 |
260 |
0.005 |
0.6 |
| 3 |
8 |
14000 |
900 |
0.1 |
1.5 |
10000 |
800 |
0.07 |
1.2 |
8000 |
600 |
0.05 |
0.9 |
| 3 |
10 |
14000 |
900 |
0.1 |
1.5 |
10000 |
800 |
0.07 |
1.2 |
8000 |
600 |
0.05 |
0.9 |
| 3 |
12 |
12000 |
800 |
0.08 |
1.5 |
9200 |
700 |
0.06 |
1.2 |
7200 |
500 |
0.04 |
0.9 |
| 3 |
16 |
10000 |
700 |
0.007 |
1.5 |
8500 |
600 |
0.05 |
1.2 |
6500 |
400 |
0.03 |
0.9 |
| 3 |
20 |
9000 |
700 |
0.07 |
1.5 |
7800 |
600 |
0.04 |
1.2 |
5800 |
400 |
0.02 |
0.9 |
Note:
*Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum spindle speed;
*Recommend oil coolant for Stainless Steels and Heat Resistance Alloys;
*Recommend using a non-contact measuring device to avoid damaging the precisiontip point;
*Decrease both spindle speed and feed rate proportionally in case of chattering;
*When the material hardness is greater than HRC58 degrees, it is recommended to use air blow cooling for roughing andoil mistor air blow cooling for finishing.