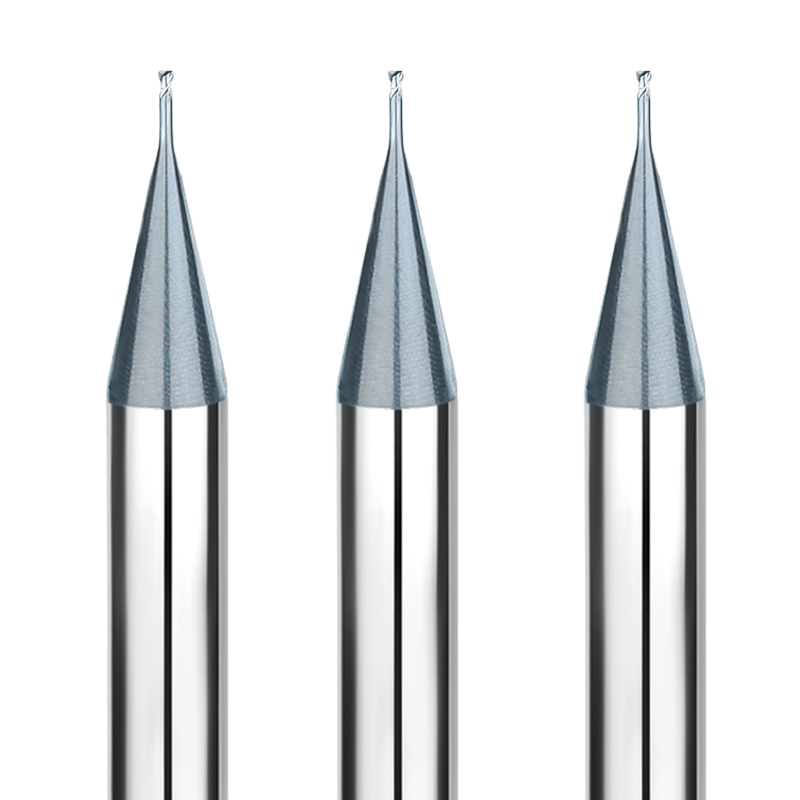
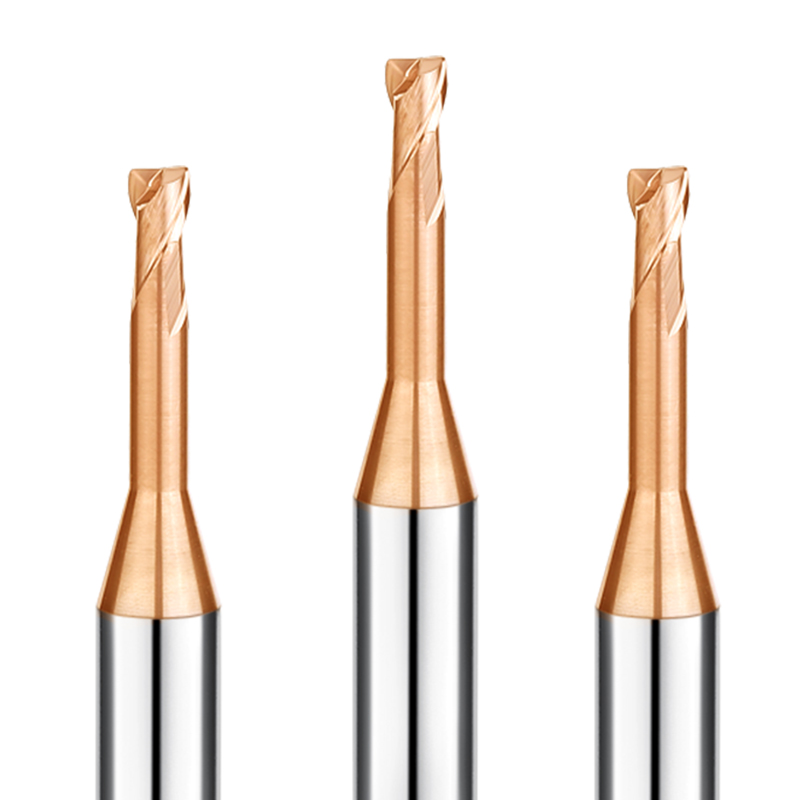
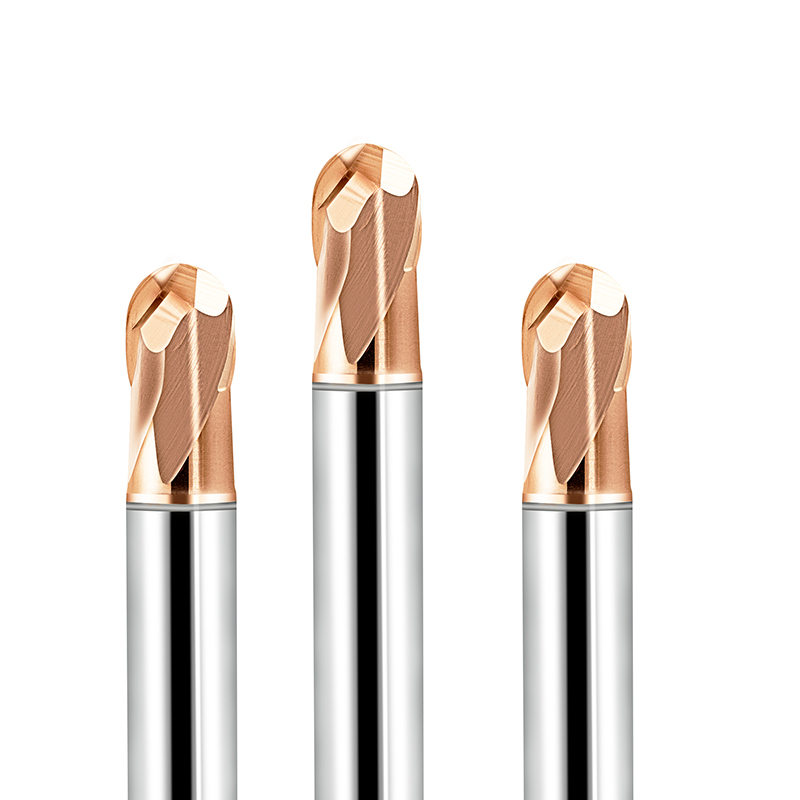
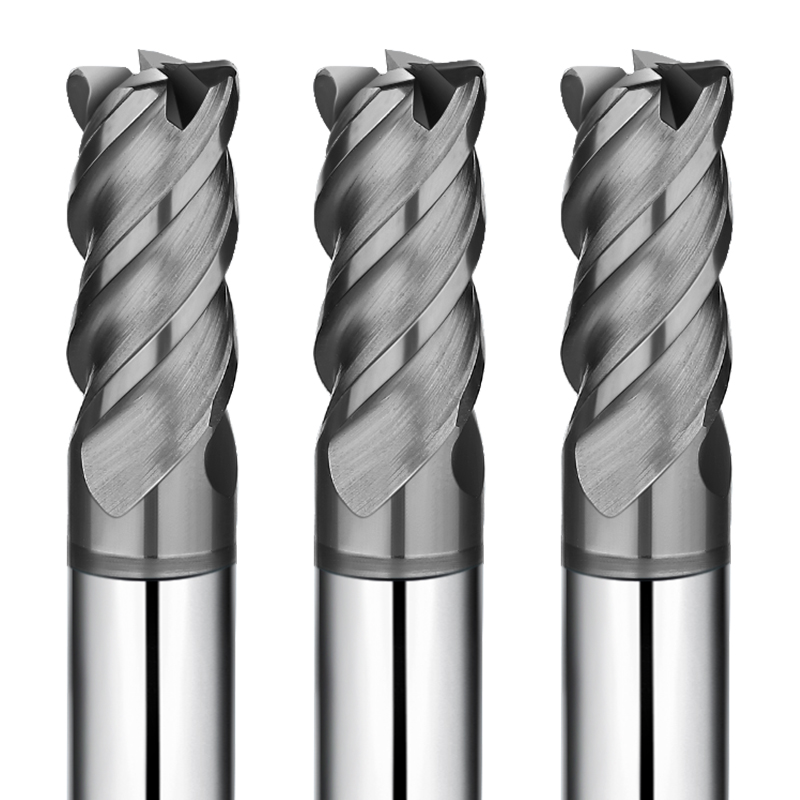
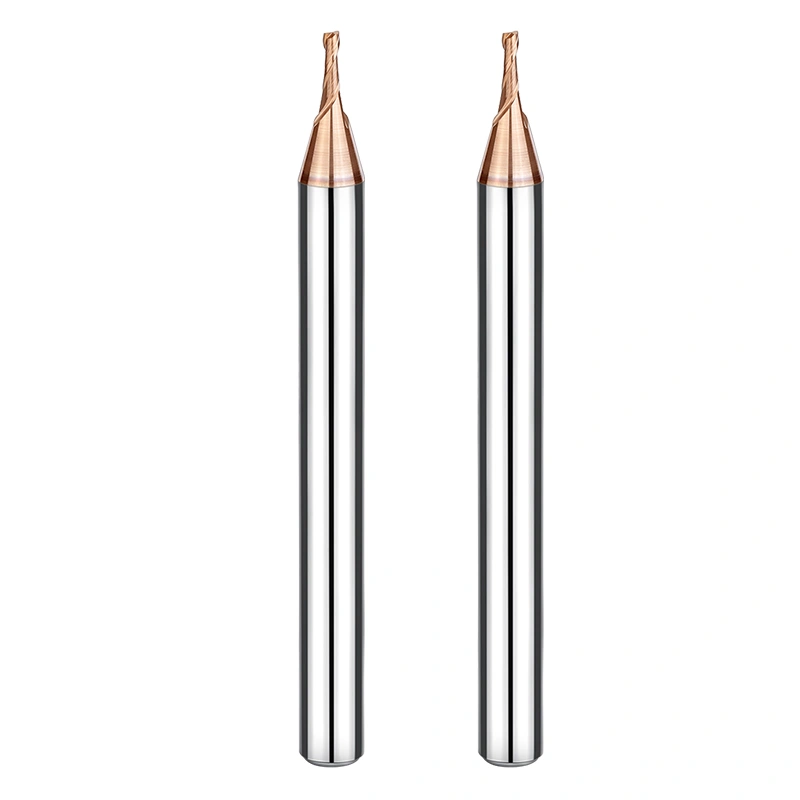
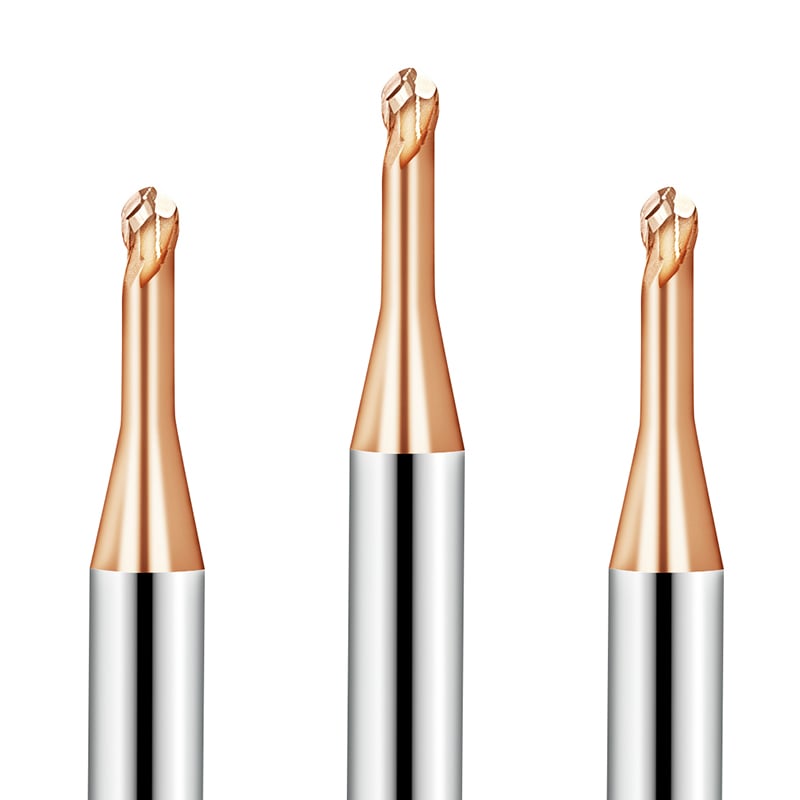
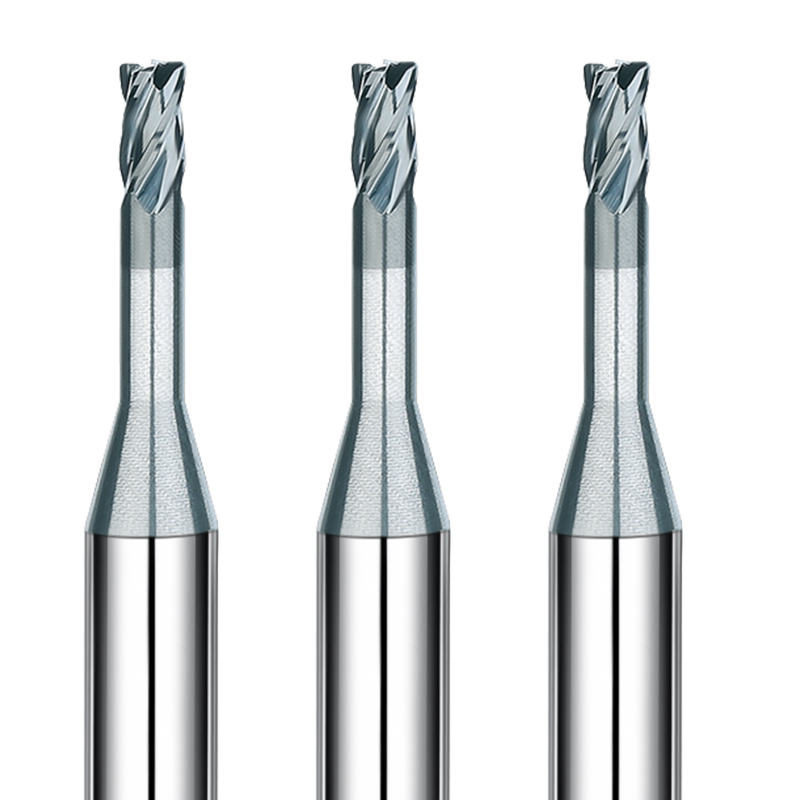
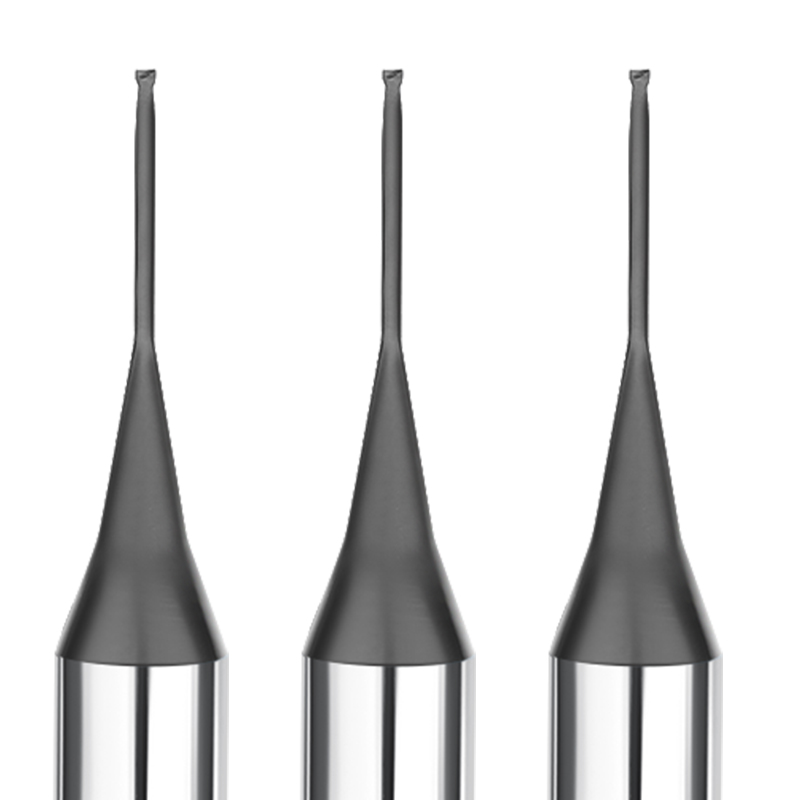
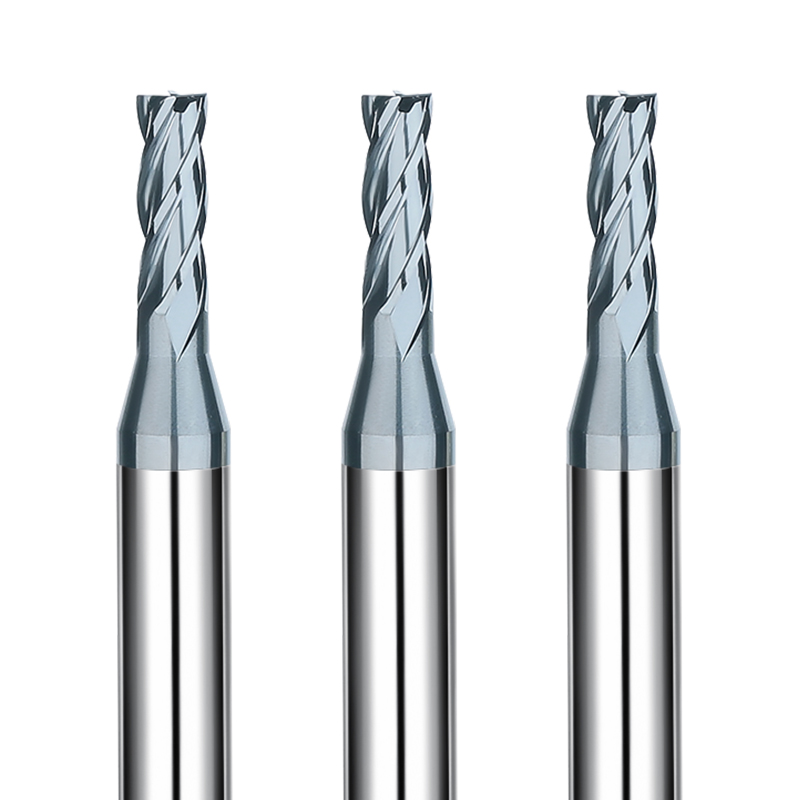
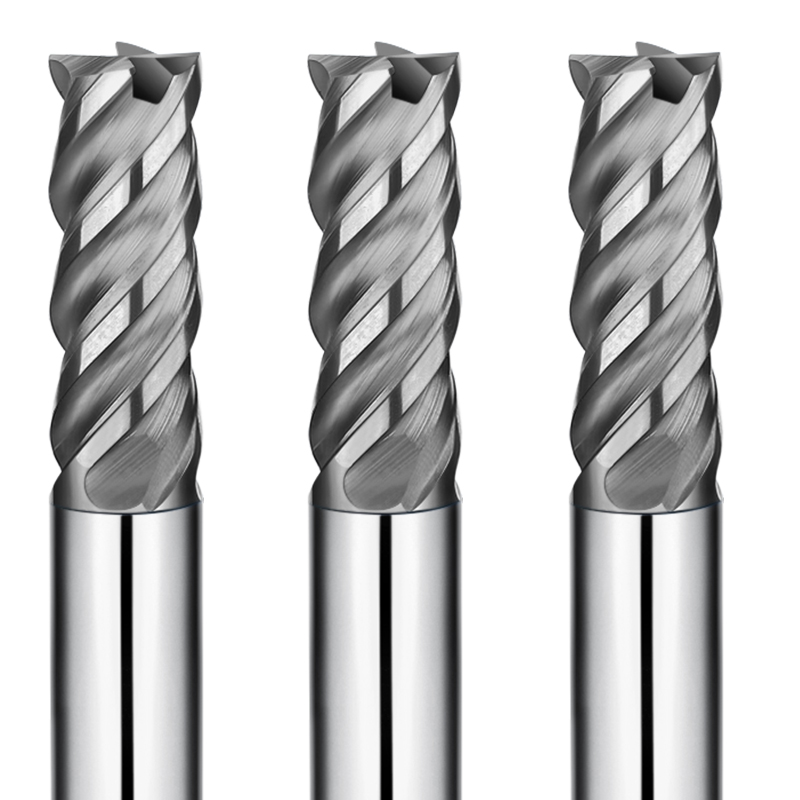
In the production of EDM electrodes and aluminum components, tool adhesion is the primary cause of poor surface finish and tool breakage. The SAMHO DLC-coated flat end mill combines a solid lubricant surface with high-rigidity carbide to deliver mirror-like finishes in non-ferrous machining.
Advanced Technical Features
- DLC Coating for Ultra-Low Friction & Non-Stick Cutting
The DLC coating provides exceptionally low friction and high surface hardness, essential when machining red copper and aluminum:
- Resists Built-Up Edge (BUE): Prevents material from welding to the cutting edge
- Reduces Cutting Heat: Allows higher speeds and feeds under dry or MQL conditions
- Optimized 2-Flute Design for Rapid Chip Evacuation
Ductile materials like pure copper and soft resins produce long, gummy chips. The open 2-flute geometry ensures:
- Maximum Chip Space: Prevents clogging and chip recutting in deep slots
- Clean Cutting Action: Burr-free edges and accurate vertical shoulders
- Mirror-Polished Flutes for Superior Surface Finish
Mirror-polished flute surfaces reduce friction during chip flow, ensuring:
- Dimensional Accuracy: Minimizes tool deflection caused by radial forces
- High Surface Quality: Delivers out-of-the-box mirror finishes on high-purity copper parts
- Application-Specific Cutting Parameters
SAMHO provides field-tested cutting data for copper, aluminum, and resins to optimize RPM, feed rates, and minimize setup time and tool failure risk
Target Applications & Industries
Applications:
- EDM Electrode Machining: Precision milling of red copper and graphite-composite electrodes
- Aluminum Component Manufacturing: High-speed slotting and contouring of 6061/7075 alloys
- Resin & Plastic Tooling: Clean, smear-free cutting of resin-based materials and soft plastics
Industries:
- Mold & Die
- Automotive
- Electronics (Heat Sinks)
- Medical Device Manufacturing
Pro-Tips for Machining Ductile Materials
- Coolant Strategy: Use MQL or high-pressure air blast to enhance chip removal and surface finish
- High-Speed Stability: Ensure balanced tool holders (Shrink-fit or Hydraulic) to minimize runout
- Tool Maintenance: Protect the ultra-sharp DLC edge with non-contact tool setters to prevent micro-chipping
Why Choose SAMHO as Your Wholesale Partner?
- Massive Model Selection: 16+ specialized models cover slotting and shoulder milling needs
- Unbeatable Wholesale Pricing: Factory-direct pricing for bulk procurement and global distributors
- OEM & Customization: Custom neck lengths and coatings available for unique project requirements
Recommended Materials for Machining (Highly Recommended: ⭐️ | Recommended: ⭕️ | Suggested: ◯)
| Category |
Work Material |
Grade |
| DIE STEEL |
Carbon steels (S45C/S55C) |
|
|
Alloy steels (SK/SCM/SUS) |
|
|
Prehardened steels (NAK/HPM) |
|
|
Hardened steels (~55/~60/~70HRC) |
|
| SPECIAL MATERIAL |
Aluminum alloys |
⭕️ |
|
Graphite |
|
|
Copper |
⭐️ |
|
Plastics |
⭕️ |
|
Carbon fiber |
|
|
Titanium alloys |
|
|
Heat resistant alloys |
|
|
Cemented carbide |
|
|
Hard brittle (non-metallic) material |
|
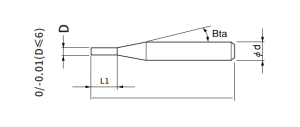
Total 16 models
| Model Number |
Outside Diameter |
Length Of Cut |
Effective Length |
Shank Taper Angle |
Overall Length |
Number Of Flutes |
Shank Diameter |
In Stock |
| SHDS2-0010020 |
0.1 |
0.2 |
– |
12° |
50 |
2 |
4 |
○ |
| SHDS2-0020040 |
0.2 |
0.4 |
– |
12° |
50 |
2 |
4 |
○ |
| SHDS2-0030060 |
0.3 |
0.6 |
– |
12° |
50 |
2 |
4 |
○ |
| SHDS2-0040080 |
0.4 |
0.8 |
– |
12° |
50 |
2 |
4 |
○ |
| SHDS2-0050100 |
0.5 |
1 |
– |
12° |
50 |
2 |
4 |
○ |
| SHDS2-0060150 |
0.6 |
1.5 |
– |
12° |
50 |
2 |
4 |
○ |
| SHDS2-0070180 |
0.7 |
1.8 |
– |
12° |
50 |
2 |
4 |
○ |
| SHDS2-0080200 |
0.8 |
2 |
– |
12° |
50 |
2 |
4 |
○ |
| SHDS2-0100300 |
1 |
3 |
– |
12° |
50 |
2 |
4 |
○ |
| SHDS2-0150400 |
1.5 |
4 |
– |
12° |
50 |
2 |
4 |
○ |
| SHDS2-0200500 |
2 |
5 |
– |
12° |
50 |
2 |
4 |
○ |
| SHDS2-0250600 |
2.5 |
6 |
– |
12° |
50 |
2 |
4 |
○ |
| SHDS2-0300800-4 |
3 |
8 |
– |
12° |
50 |
2 |
4 |
○ |
| SHDS2-0401000-4 |
4 |
10 |
– |
– |
50 |
2 |
4 |
○ |
| SHDS2-0401000-6 |
4 |
10 |
– |
12° |
60 |
2 |
6 |
○ |
| SHDS2-0601500 |
6 |
15 |
– |
– |
60 |
2 |
6 |
○ |
Milling Conditions
| Work Material |
Oxygen-free & Copper |
| (mm)Diameter |
(min-1)Speed |
(mm/min)Feed |
| D1.0 |
10000 |
150 |
| D1.5 |
8000 |
180 |
| D2.0 |
8000 |
200 |
| D2.5 |
6000 |
300 |
| D3 |
7000 |
300 |
| D4 |
7000 |
300 |
| D4 |
7000 |
300 |
| D6 |
7000 |
300 |
Milling Amount for Side Milling(mm)
| Work Material \ Length of Cut |
2.5D (Length of Cut=Diameter*2.5) |
4D (Length of Cut=Diameter*4) |
| 45HRC以下Below 45HRC |
ae=0.07D ap=2D |
ae=0.07D ap=2D |
| 45HRC以上Above 45HRC |
ae=0.03D ap=1.5D |
ae=0.03D ap=1.5D |
D: Diameter (mm)
ap:Axial Depth (mm)
ae: Radial Depth (mm)
Note:
*Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum spindle speed;
*Recommend oil coolant for Stainless Steels and Heat Resistance Alloys.
Contour Milling
| Work Material |
Oxygen-free & Copper |
| (mm)Diameter |
(min-1)Speed |
(mm/min)Feed |
| D0.1 |
40000 |
180 |
| D0.2 |
40000 |
300 |
| D0.3 |
36000 |
500 |
| D0.4 |
30000 |
700 |
| D0.5 |
32000 |
800 |
| D0.6 |
26000 |
800 |
| D0.7 |
26000 |
800 |
| D0.8 |
22000 |
1000 |
| D1.0 |
18000 |
1200 |
| D1.5 |
16000 |
1500 |
| D2.0 |
16000 |
1800 |
| D2.5 |
14000 |
1800 |
| D3 |
12000 |
2200 |
| D4 |
12000 |
2200 |
| D4 |
12000 |
2200 |
| D6 |
10000 |
2400 |
Note:
*Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum spindle speed;
*Recommend oil coolant for Stainless Steels and Heat Resistance Alloys;
*Recommend using a non-contact measuring device to avoid damaging the precisiontip point;
*Decrease both spindle speed and feed rate proportionally in case of chattering;