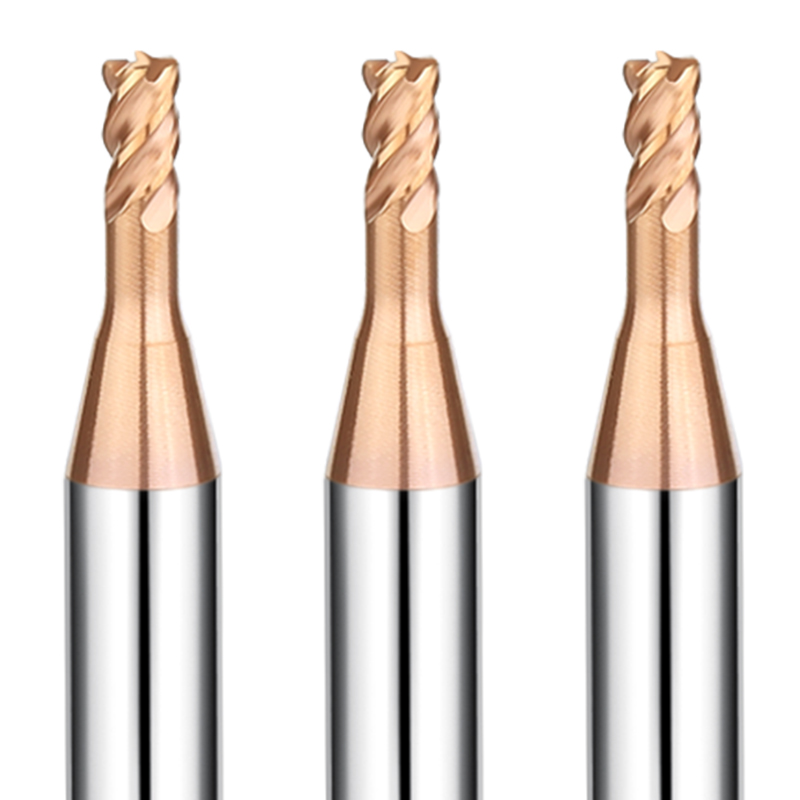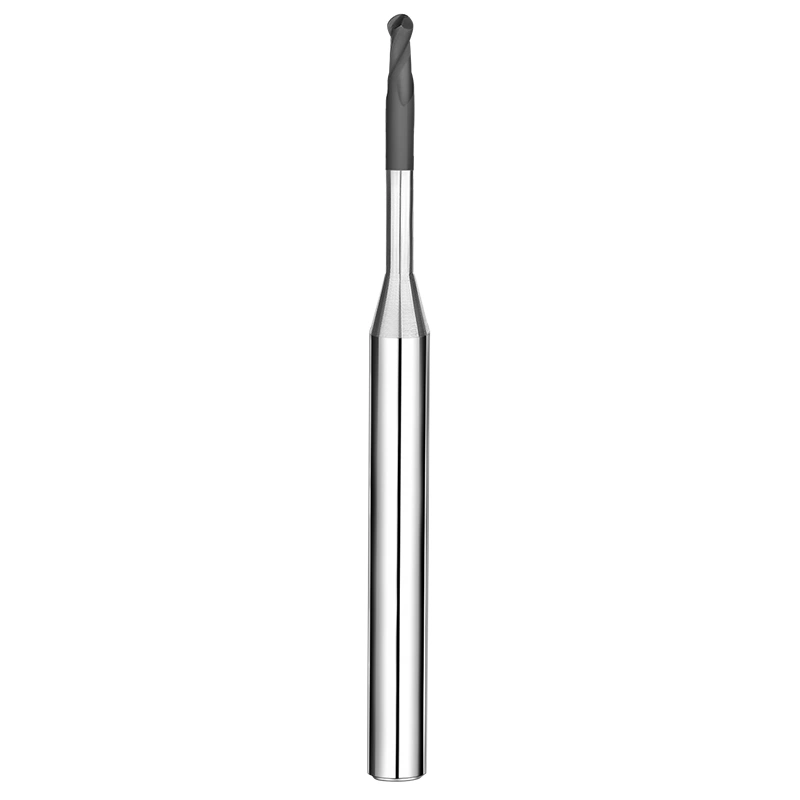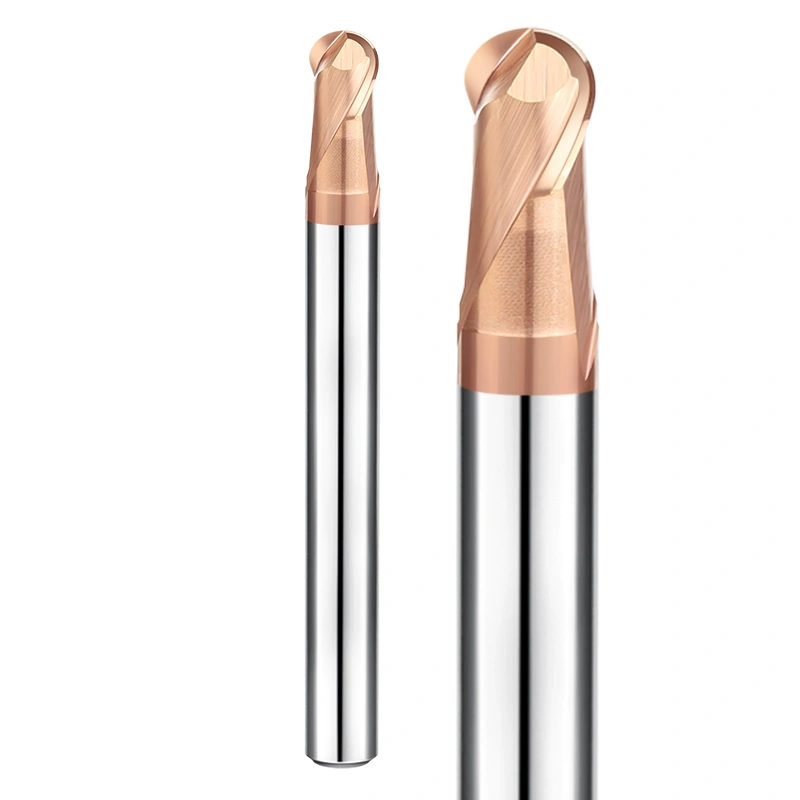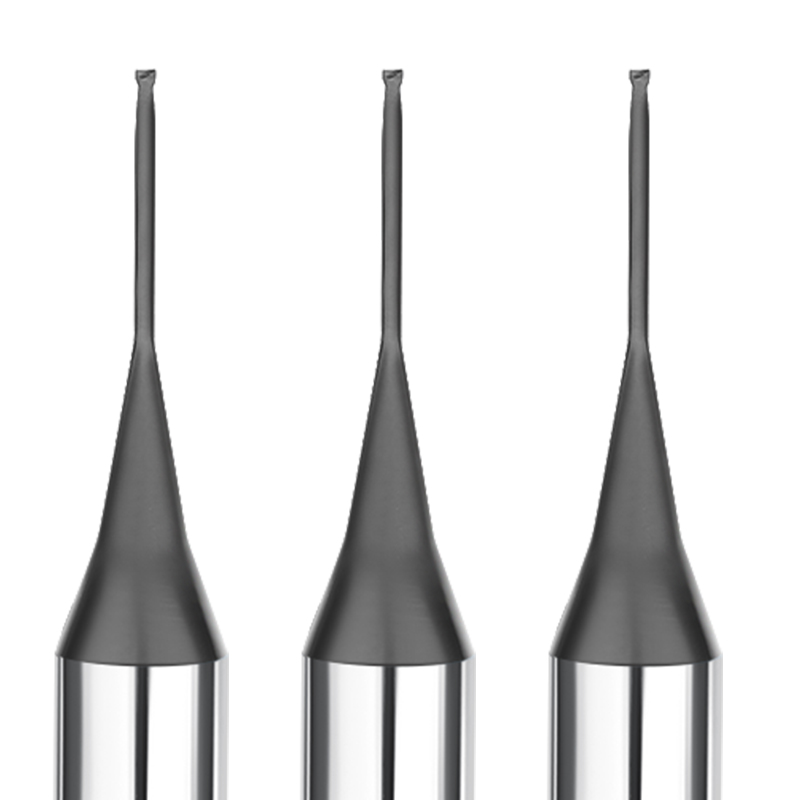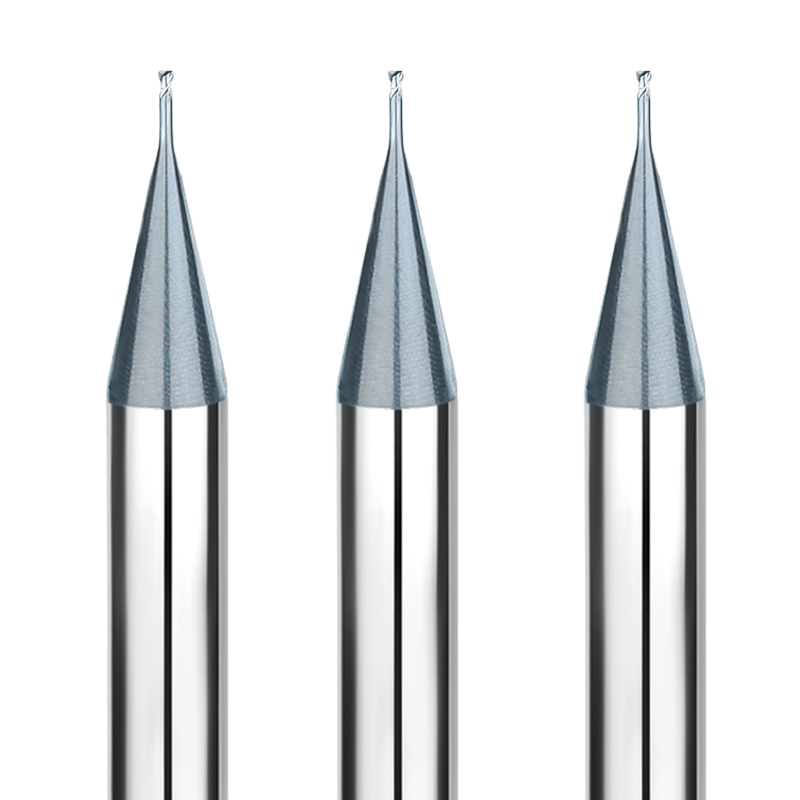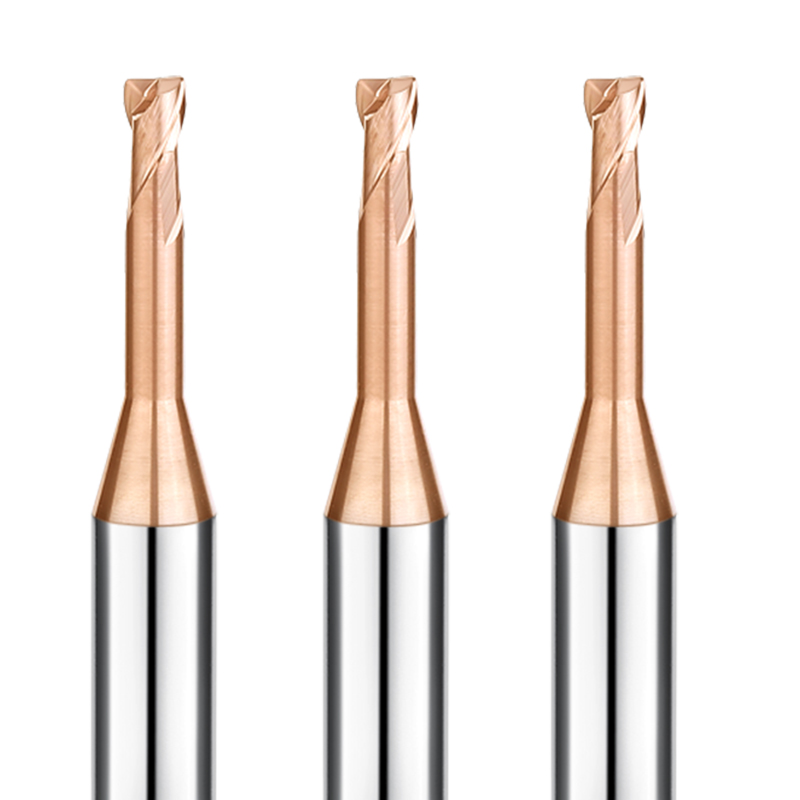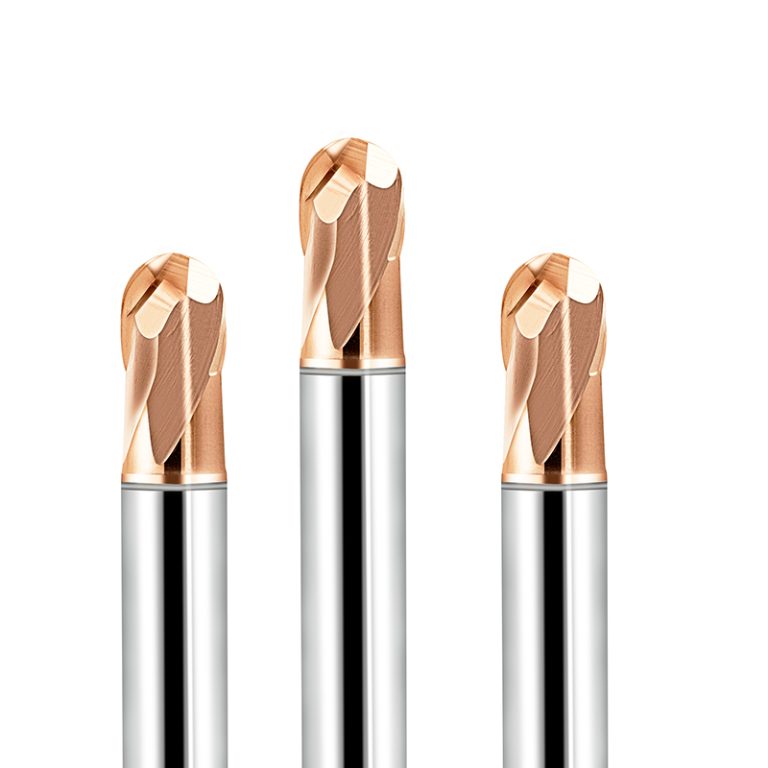
end mill end mill end mill

End Mill for Hardened Steel 2 Flute Ball Nose End Mill

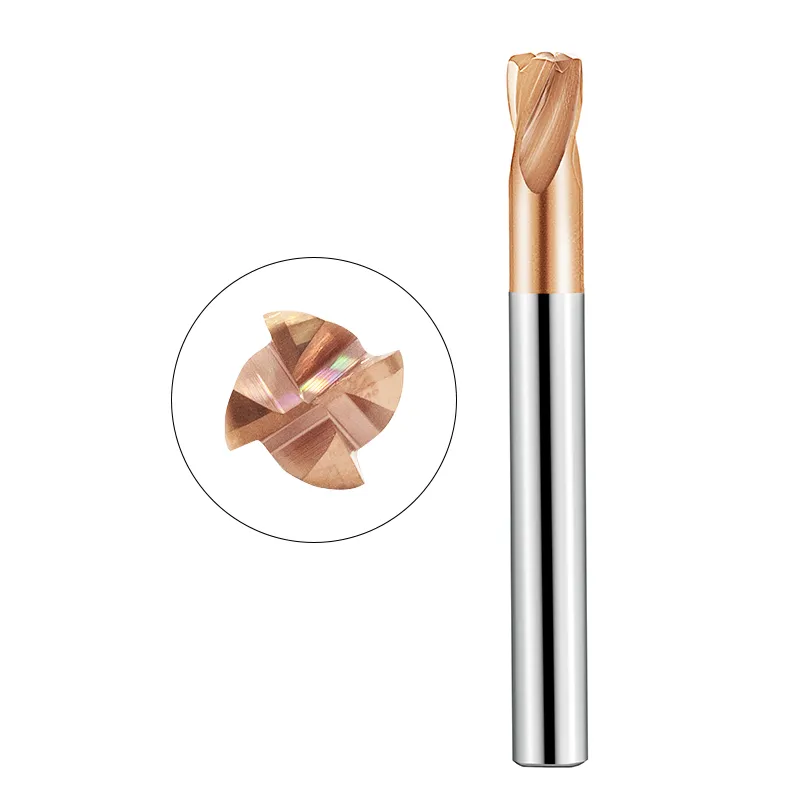
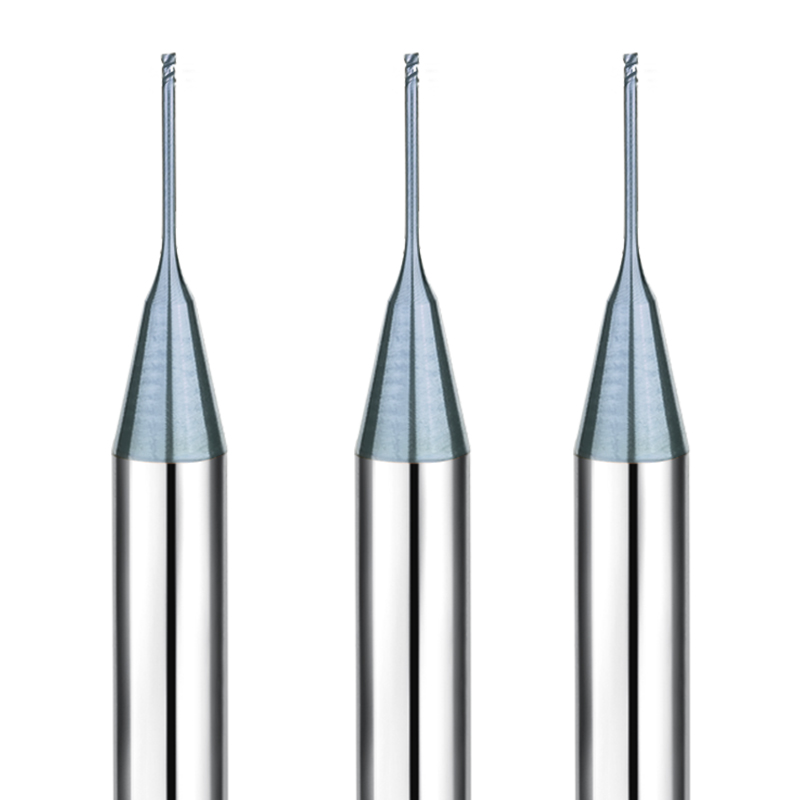
SAMHO 2-Flute Ball Nose End Mill — The Ultimate Tool for Precision CNC Milling of High-Hardness Steel

Don’t let high-hardness materials slow down your production. The SAMHO 2-flute ball endmill is engineered for precision machining of high-hardness and heat-treated steels. It delivers both exceptional durability and high machining accuracy. Thanks to cutting-edge high-adhesion coating technology, tool life is significantly extended, and performance remains stable even under continuous high-load cutting.

Applicable Materials: High-hardness steels, heat-treated steels, and other high-strength components.

Ultimate Durability: Made from a high-strength, micro-grained cemented carbide matrix and coated with advanced high-adhesion material, this ball end mill resists wear and edge chipping, ensuring reliable performance during high-speed, high-load CNC milling.

High-Precision Tool Holder: The precision-machined shank guarantees stable clamping, improving machining repeatability and surface finish.

In machining high hardness and heat treated steels, tool performance requirements are extremely demanding. Tools must offer both exceptional wear resistance and precise cutting ability. SAMHO’s coated 2 flute ball end mills (R0.1–R6 mm) are engineered to meet these strict standards. They enhance CNC machining efficiency, improve surface finish, and enable operators to perform precise milling on high-hardness materials with ease.


Advanced Technical Features

High-Adhesion Coating for Ultra-Long Tool Life

Using proprietary high-performance coating technology, these 2-flute ballnose end mills deliver exceptional hardness and thermal resistance. They provide stable and reliable performance when machining high-hardness and heat-treated steels.

  • Superior Wear Resistance: Significantly delays tool wear during continuous high-speed cutting, maintaining a sharp and consistent cutting edge.
  • Robust Micro-Chipping Resistance: The coating forms a strong bond with the carbide substrate, resisting edge chipping caused by high-impact cutting forces.
  • Suitable for High-Load Machining: Ensures stable cutting performance and consistent tool life even under heavy-duty conditions.

Ball-Nose Geometry Designed for 3D Surfaces and Complex Contours

The precision ball-nose geometry excels in machining complex spatial surfaces. It is ideal for mold finishing, profile milling, and other 3D CNC applications.

  • Mold Surface Machining: Perfect for finishing 3D cavities, complex contours, and free-form surfaces.
  • High-Hardness Steel Finishing: Maintains stable surface quality when machining heat-treated or high-hardness steels.
  • Exceptional Detail Retention: Preserves sharp contours and consistent precision in small-radius areas and transition zones.

Efficient Dual-Flute Design for Enhanced Machining Stability

The dual-flute structure balances cutting forces and optimizes heat control, improving overall CNC milling stability.

  • Optimized Chip Evacuation: Efficiently removes chips and prevents accumulation in the cutting zone.
  • Reduced Heat Buildup: Minimizes thermal load, extending tool life during high-hardness steel machining.
  • Enhanced Machining Stability: Reduces vibration and cutting force fluctuations, producing smoother surfaces.

Ultra-Fine Grain Carbide Substrate + High-Precision Grinding

Manufactured from high-strength, ultra-fine grain carbide and precision 5-axis grinding, these tools ensure consistent and reliable machining performance.

  • High Dimensional Accuracy: Critical tolerances are controlled within ±0.01 mm.
  • Superior Fracture Resistance: Increases durability against impact forces in high-hardness steel applications.
  • High Batch Consistency: Ideal for demanding mold production environments requiring stability and repeatability.

Target Applications & Industries

This series of 2 flute ball nose end mills bit is highly versatile and engineered for precision CNC milling of high-hardness materials:

  • Precision Machining of High-Hardness and Heat-Treated Steels: Ideal for finishing molds, cutting tools, and other high-hardness components.
  • Complex Cavity and 3D Surface Machining: Perfect for contour milling of mold cavities, deep cavities, and complex 3D surfaces.
  • High-Precision Contour Machining: Ensures accurate shaping of small radii, transition zones, and free-form surfaces.
  • Precision 3D Surface Finishing: Maintains consistent surface finish and dimensional accuracy in high-hardness steel machining.

Why Choose SAMHO as Your Wholesale Partner?

OEM/ODM Support: Flexible customization to meet the unique requirements of different clients.

Exceptional Dimensional Accuracy: Shank diameter tolerance is strictly controlled within 0–0.003 mm, ensuring stable machining and high repeatability.

High-Performance Tooling: Engineered for high-hardness and heat-treated steels, delivering precise and efficient CNC milling solutions.

Reliable Partner: With over 20 years of CNC tool R&D experience, SAMHO provides expert technical support and long-term supply reliability.
Recommended Materials for Machining (Highly Recommended: ⭐️ | Recommended: ⭕️ | Suggested: )

Category Work Material Grade
DIE STEEL Carbon steels (S45C/S55C)
Alloy steels (SK/SCM/SUS)
Prehardened steels (NAK/HPM)
Hardened steels (~55/~60/~70HRC) ⭐️
SPECIAL MATERIAL Aluminum alloys
Graphite
Copper
Plastics
Carbon fiber
Titanium alloys
Heat resistant alloys
Cemented carbide
Hard brittle (non-metallic) material

2 flute flat long neck end mill

Total 31 models

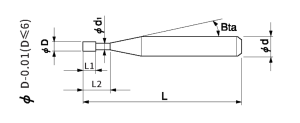
Model Number Outside Diameter Length Of Cut Effective Length Shank Taper Angle Overall Length Number Of Flutes Shank Diameter In Stock
SHHR2-002003 R0.1 0.3 12° 50 2 4
SHHR2-0030045 R0.15 0.45 12° 50 2 4
SHHR2-004006 R0.2 0.6 12° 50 2 4
SHHR2-005008 R0.25 0.8 12° 50 2 4
SHHR2-006009 R0.3 0.9 12° 50 2 4
SHHR2-008012 R0.4 1.2 12° 50 2 4
SHHR2-015015 R0.75 1.5 12° 50 2 4
SHHR2-020020 R1 2 12° 50 2 4
SHHR2-020040-6 R1 2 4 12° 60 2 6
SHHR2-030060-3 R1.5 3 6 50 2 3
SHHR2-030060-4 R1.5 3 6 12° 50 2 4
SHHR2-030060-6 R1.5 3 6 12° 60 2 6
SHHR2-040080 R2 4 8 50 2 4
SHHR2-040080-75 R2 4 8 75 2 4
SHHR2-040080-100 R2 4 8 100 2 4
SHHR2-040080-6 R2 4 8 12° 60 2 6
SHHR2-050100 R2.5 5 10 12° 60 2 6
SHHR2-060120 R3 6 12 60 2 6
SHHR2-060120-75 R3 6 12 75 2 6
SHHR2-060120-100 R3 6 12 100 2 6
SHHR2-080160 R4 8 16 60 2 8
SHHR2-080160-75 R4 8 16 75 2 8
SHHR2-080160-100 R4 8 16 100 2 8
SHHR2-080160-150 R4 8 16 150 2 8
SHHR2-100200 R5 10 20 75 2 10
SHHR2-100200-100 R5 10 20 100 2 10
SHHR2-100200-150 R5 10 20 150 2 10
SHHR2-120240 R6 12 24 75 2 12
SHHR2-120240-100 R6 12 24 100 2 12
SHHR2-120240-150 R6 12 24 150 2 12

Contour Milling Parameters

Work Material HRC48-55 hardened steel HRC56-60 hardened steel HRC63-70 hardened steel
Diameter Effective Length(mm) (min-1) Speed (mm/min) Feed (mm) Axial depth (mm) Radidl depth (min-1) Speed (mm/min) Feed (mm) Axial depth (mm) Radidl depth (min-1) Speed (mm/min) Feed (mm) Axial depth
(mm) Radidl depth
R0.1 0.3 40000 250 0.01 0.03 40000 250 0.01 0.03 36000 200 0.006 0.018
R0.15 0.45 40000 400 0.01 0.03 40000 350 0.01 0.03 36000 250 0.008 0.024
R0.2 0.6 40000 600 0.015 0.045 40000 550 0.015 0.045 36000 350 0.01 0.027
R0.25 0.8 40000 900 0.02 0.065 40000 800 0.015 0.05 30000 400 0.015 0.03
R0.3 0.9 40000 1400 0.045 0.15 36000 1200 0.025 0.13 25000 600 0.02 0.1
R0.4 1.2 35000 1600 0.06 0.21 30000 1600 0.04 0.17 20000 700 0.02 0.12
R0.5 1 30000 1800 0.1 0.3 24000 2000 0.1 0.3 16000 900 0.05 0.2
R0.75 1.5 30000 2200 0.2 0.5 18000 2000 0.12 0.4 11000 900 0.06 0.25
R1 4 28000 2600 0.3 0.7 14000 2000 0.15 0.5 11000 1000 0.08 0.35
R1.5 6 21000 3000 0.4 1 12000 2200 0.2 0.7 8500 1100 0.12 0.55
R2 8 18000 3200 0.5 1.3 9000 2200 0.25 0.95 7000 1200 0.15 0.55
R2.5 10 15000 3500 0.6 1.5 8000 2500 0.25 1.05 6500 1200 0.15 0.55
R3 12 13000 3500 0.7 1.8 6500 2500 0.3 1.3 5000 1500 0.2 1
R4 16 9500 3000 0.8 2.1 5500 2200 0.4 1.7 4000 1000 0.25 1.35
R5 20 7500 2500 0.9 2.5 4500 2000 0.5 2.1 3000 800 0.3 1.7
R6 24 6500 2000 0.9 3 4500 1700 0.6 2.6 2400 800 0.35 2

Milling Amount for Side Milling(mm)

Work Material \ Length of Cut 2.5D (Length of Cut=Diameter*2.5) 4D (Length of Cut=Diameter*4)
45HRC以下Below 45HRC ae​=0.07Dap​=2D ae​=0.07Dap​=2D
45HRC以上Above 45HRC ae​=0.03Dap​=1.5D ae​=0.03Dap​=1.5D

D: Diameter (mm)

ap:AxialDepth (mm)

ae: Radial Depth (mm)

Note:

*Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum spindle speed;

*Recommend oil coolant for Stainless Steels and Heat Resistance Alloys;

*Recommend using a non-contact measuring device to avoid damaging the precisiontip point;

*Decrease both spindle speed and feed rate proportionally in case of chattering;

*When the material hardness is greater than HRC58 degrees, it is recommended to use air blow cooling for roughing andoil mistor air blow cooling for finishing.

Download 2: End Mill for Hardened Steel 2 Flute Ball Nose End Mill File

Related Product

Related Post

Get Your Custom Milling Tool Guide

Fill out the form below to receive SAMHO’s complete product catalog.