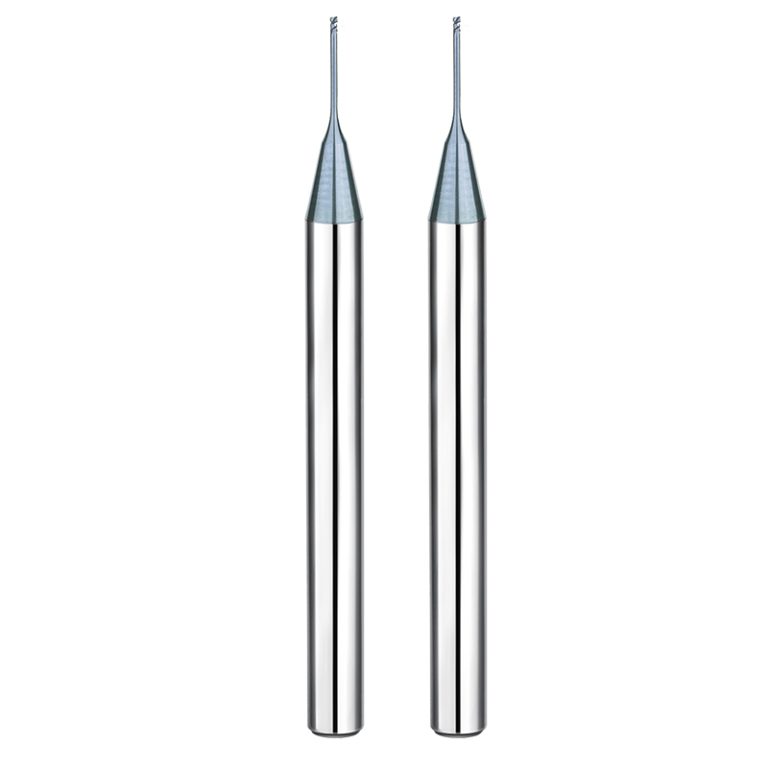
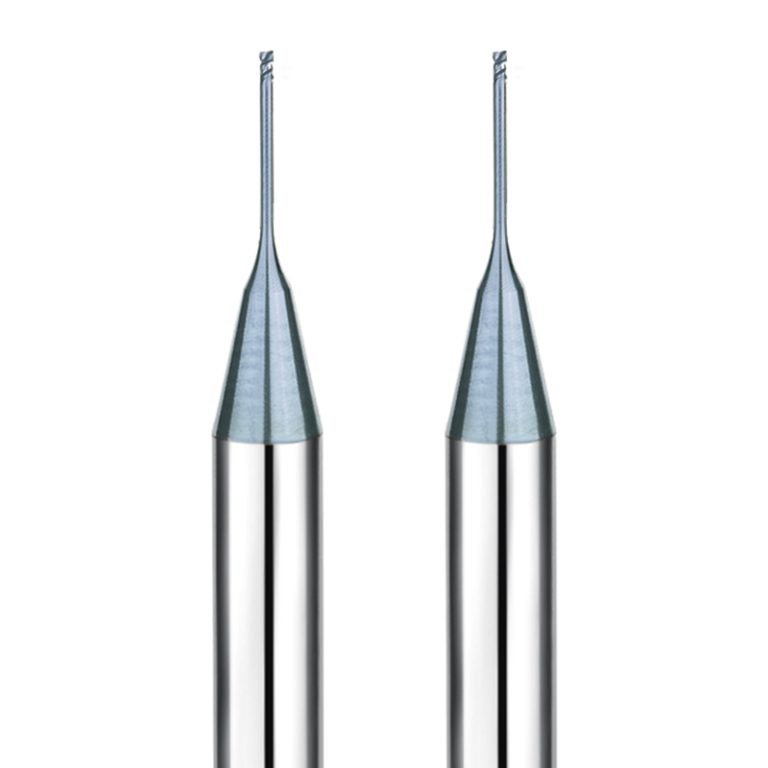
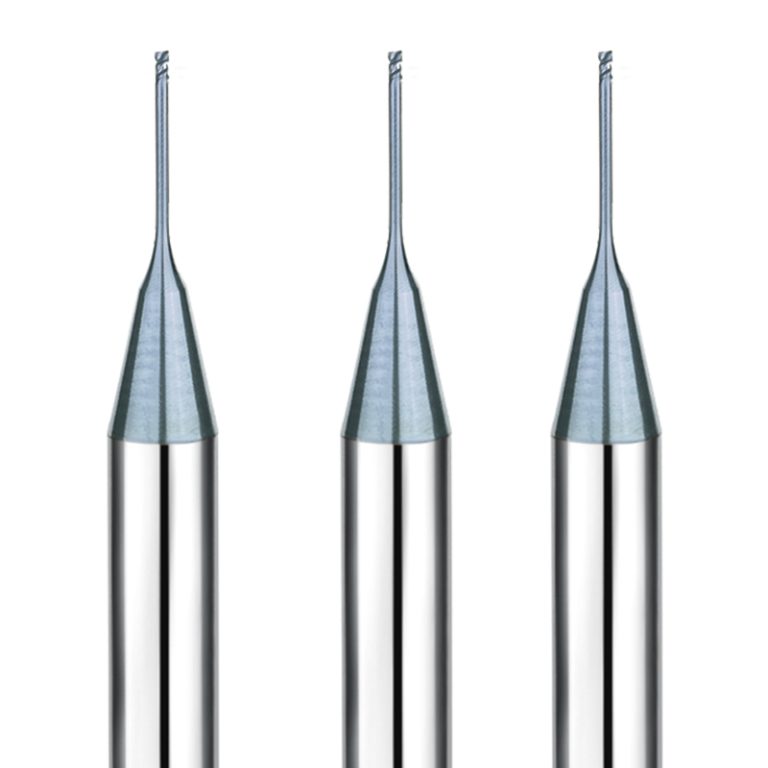
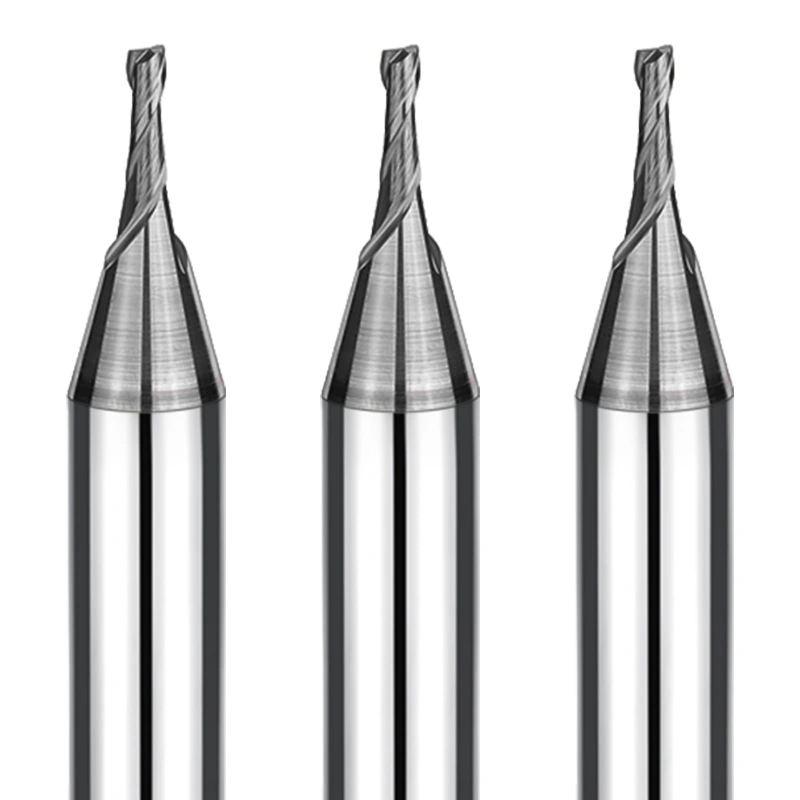
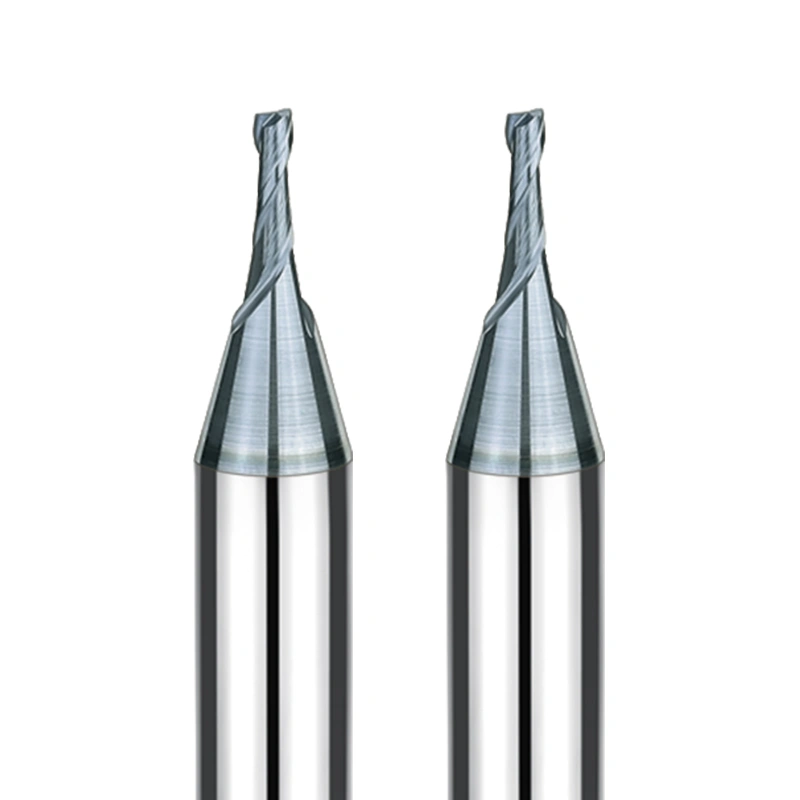
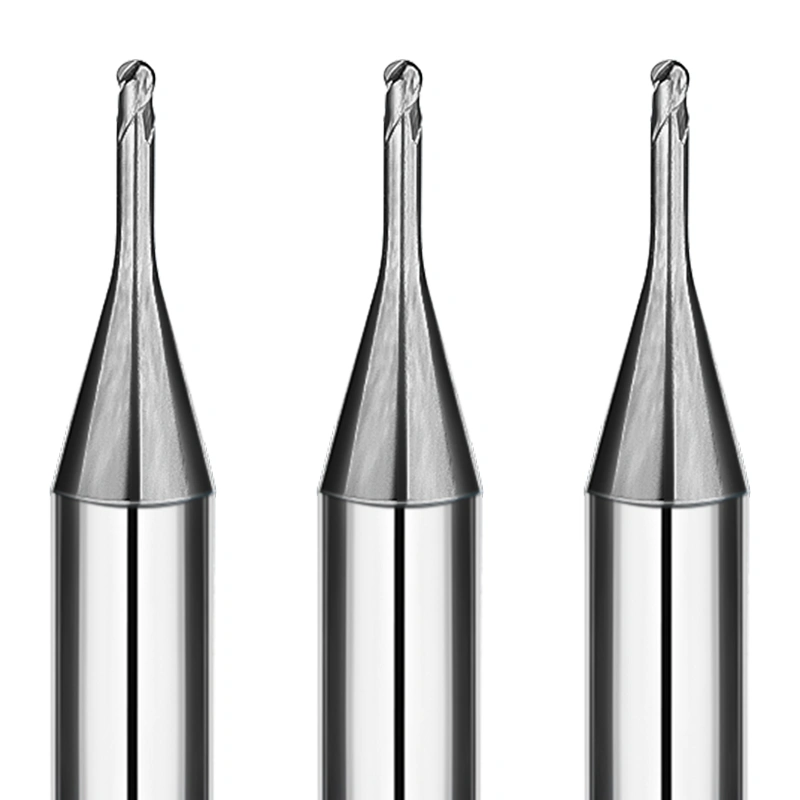
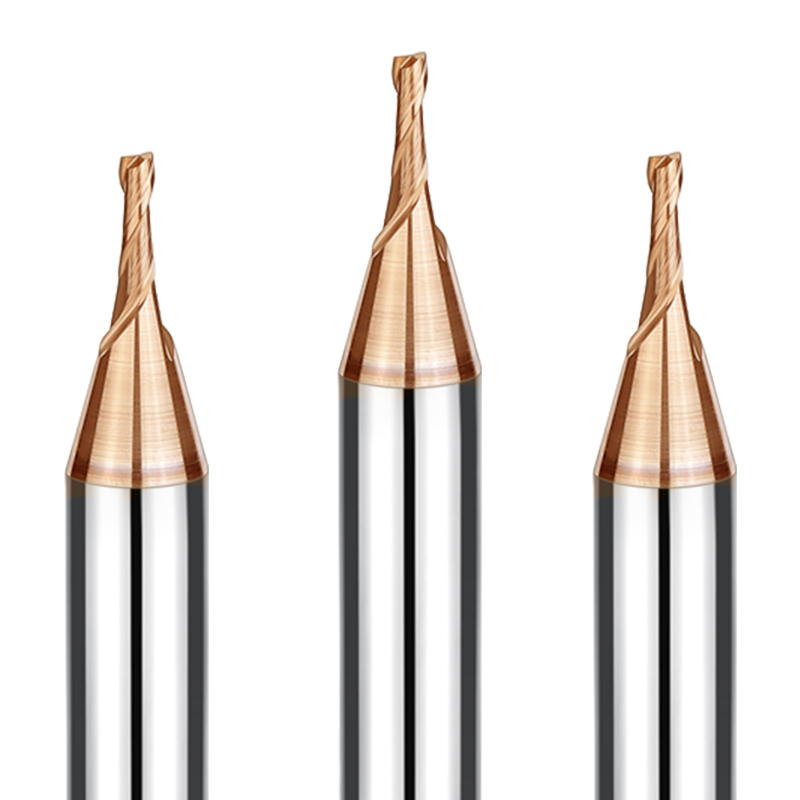
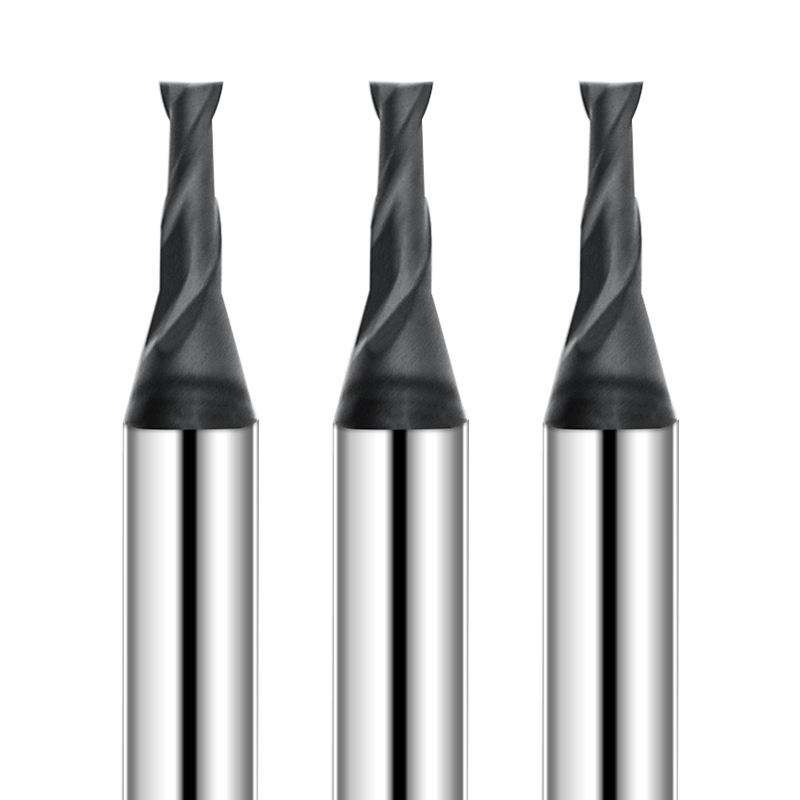
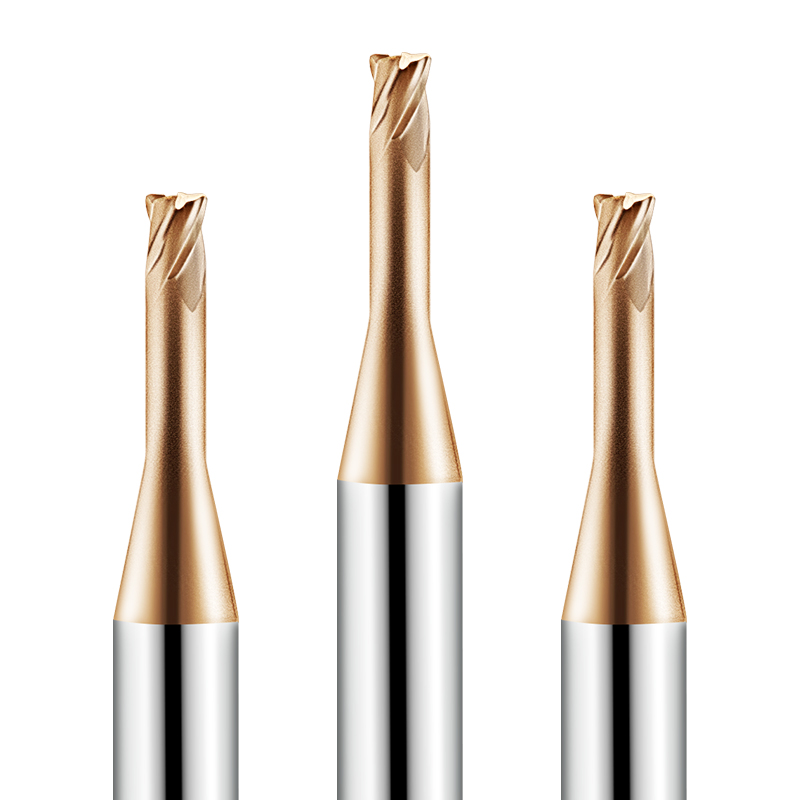
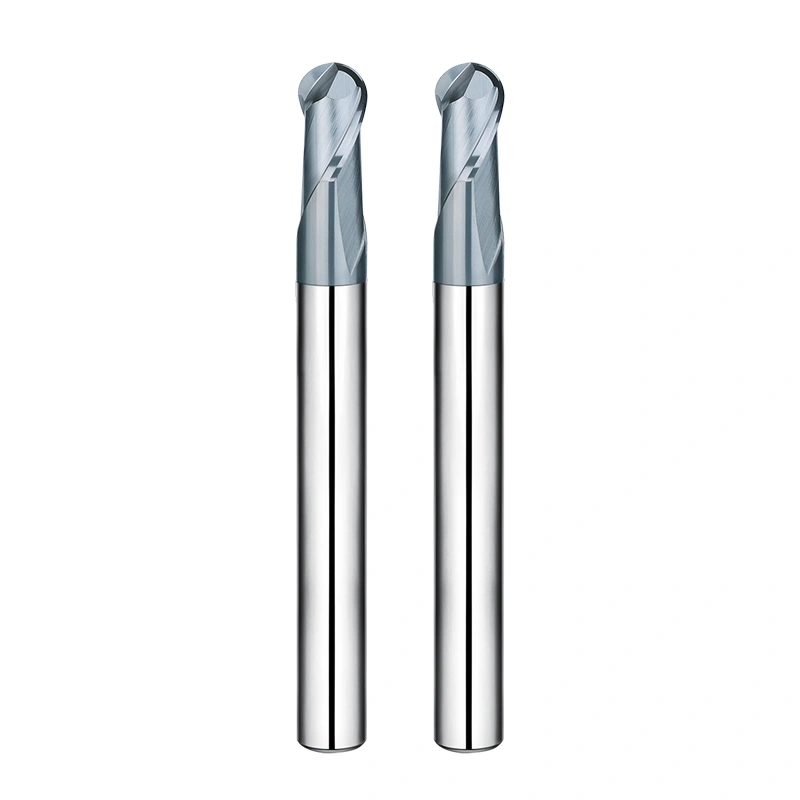
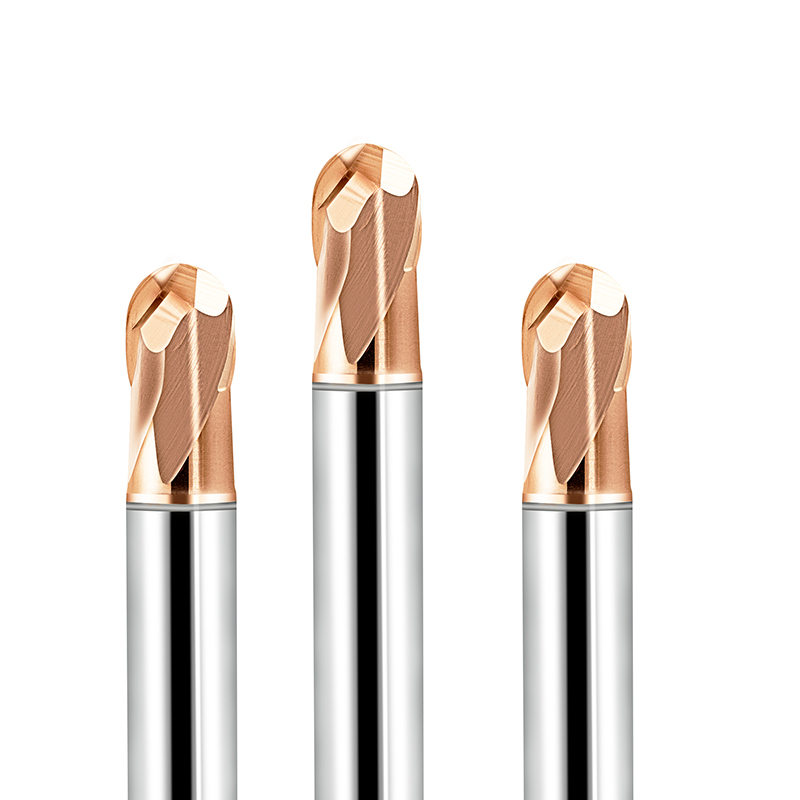
SAMHO HRC55 2-Flute Long-Neck Flat End Mill — High-Efficiency Solution for Deep Cavity Machining
High Hardness (HRC55) for Wear Resistance and Stability
This HRC55 flat end mill bit is made from premium carbide. It offers excellent wear resistance and strong anti-chipping performance. Ideal for stable machining of medium-to-high hardness materials.
2-Flute Design for Smooth Chip Evacuation
The 2 flute long neck end mill provides larger chip clearance. It improves chip evacuation and reduces chip buildup. This makes it especially suitable for stainless steel and mold steel machining.
Long-Neck Design for Deep Cavity Machining
The extended neck allows efficient machining of deep holes, deep slots, and complex contours. It reduces interference and increases machining flexibility.
High-Precision Shank for Stable Clamping
The shank tolerance is controlled within 0 to -0.003 mm. This ensures excellent concentricity and secure clamping. It improves machining accuracy and extends tool life.
Wide Material Compatibility
Suitable for materials from HRC28 to HRC52, including mold steel and stainless steel. Widely used in mold making, precision components, and general machining applications.
HRC55 2-Flute Long-Neck Flat End Mill — Professional Usage Recommendations
Optimize Cutting Parameters
Adjust spindle speed and feed rate based on material hardness (HRC 28–52). Avoid excessive cutting load to maintain tool stability and extend tool life.
Prioritize Deep Cavity and Finishing Operations
The 2 flute long neck end mill is designed for deep holes, deep slots, and complex contours. It is recommended for semi-finishing and finishing operations to achieve better surface quality.
Improve Chip Evacuation Efficiency
When machining stainless steel or mold steel, ensure effective chip removal. Cutting fluid or air cooling is recommended to prevent chip buildup and tool adhesion.
Ensure High-Rigidity Clamping
Use a high-precision tool holder to ensure stable clamping. Keep tool overhang as short as possible to reduce vibration and improve machining accuracy.
Avoid Heavy Side Cutting Loads
Due to the lower rigidity of long-neck tools, avoid heavy radial cutting or impact machining. A multi-pass or layered cutting strategy is recommended for stable performance.
Recommended Materials for Machining (Highly Recommended: ⭐️ | Recommended: ⭕️ | Suggested: ◯)
| Category |
Work Material |
Grade |
| DIE STEEL |
Carbon steels (S45C/S55C) |
⭕️ |
|
Alloy steels (SK/SCM/SUS) |
⭕️ |
|
Prehardened steels (NAK/HPM) |
⭕️ |
|
Hardened steels (~55/~60/~70HRC) |
◯ |
| SPECIAL MATERIAL |
Aluminum alloys |
◯ |
|
Graphite |
|
|
Copper |
⭕️ |
|
Plastics |
|
|
Carbon fiber |
|
|
Titanium alloys |
◯ |
|
Heat resistant alloys |
|
|
Cemented carbide |
|
|
Hard brittle (non-metallic) material |
|
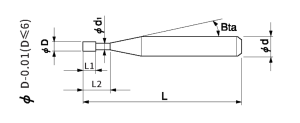
Total 37 models
| Model Number |
Outside Diameter |
Length Of Cut |
Effective Length |
Shank Taper Angle |
Overall Length |
Number Of Flutes |
Shank Diameter |
In Stock |
| SHBLS2-002005 |
0.2 |
0.3 |
0.5 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-002010 |
0.2 |
0.3 |
1 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-002015 |
0.2 |
0.3 |
1.5 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-003010 |
0.3 |
0.5 |
1 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-003015 |
0.3 |
0.5 |
1.5 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-003020 |
0.3 |
0.5 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-003030 |
0.3 |
0.5 |
3 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-004010 |
0.4 |
0.6 |
1 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-004020 |
0.4 |
0.6 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-004030 |
0.4 |
0.6 |
3 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-004040 |
0.4 |
0.6 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-005010 |
0.5 |
0.75 |
1 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-005020 |
0.5 |
0.75 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-005040 |
0.5 |
0.75 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-005060 |
0.5 |
0.75 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-006020 |
0.6 |
0.9 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-006040 |
0.6 |
0.9 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-006060 |
0.6 |
0.9 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-006080 |
0.6 |
0.9 |
8 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-008020 |
0.8 |
1.2 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-008040 |
0.8 |
1.2 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-008060 |
0.8 |
1.2 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-008080 |
0.8 |
1.2 |
8 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-010040 |
1 |
1.5 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-010060 |
1 |
1.5 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-010080 |
1 |
1.5 |
8 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-010100 |
1 |
1.5 |
10 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-015040 |
1.5 |
2.3 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-015060 |
1.5 |
2.3 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-015080 |
1.5 |
2.3 |
8 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-015100 |
1.5 |
2.3 |
10 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-020040 |
2 |
3 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-020060 |
2 |
3 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-020080 |
2 |
3 |
8 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-020100 |
2 |
3 |
10 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-020120 |
2 |
3 |
12 |
12° |
50 |
2 |
4 |
○ |
| SHBLS2-020160 |
2 |
3 |
16 |
12° |
50 |
2 |
4 |
○ |
SHBLS2 Contour Milling Parameters
| Work Material |
Oxygen-free CopperRed Copper |
HRC30-45 carbon steeland prehardened steel |
HRC45-55 hardened steel |
| (mm)Diameter |
(mm)Effective Length |
(min-1)Speed |
(mm/min)Feed |
(min-1)Speed |
(mm/min)Feed |
(min-1)Speed |
(mm/min)Feed |
| D0.2 |
0.5 |
30000 |
120 |
30000 |
120 |
30000 |
120 |
| D0.2 |
1 |
30000 |
120 |
30000 |
120 |
30000 |
100 |
| D0.2 |
1.5 |
28000 |
120 |
28000 |
120 |
28000 |
100 |
| D0.3 |
1 |
30000 |
150 |
30000 |
150 |
30000 |
150 |
| D0.3 |
1.5 |
28000 |
120 |
28000 |
120 |
26000 |
120 |
| D0.3 |
2 |
26000 |
120 |
26000 |
120 |
22000 |
100 |
| D0.3 |
3 |
26000 |
100 |
26000 |
100 |
20000 |
80 |
| D0.4 |
1 |
26000 |
300 |
26000 |
300 |
26000 |
260 |
| D0.4 |
2 |
26000 |
220 |
26000 |
220 |
24000 |
200 |
| D0.4 |
3 |
24000 |
180 |
24000 |
180 |
20000 |
200 |
| D0.4 |
4 |
24000 |
150 |
24000 |
150 |
18000 |
150 |
| D0.5 |
1 |
26000 |
400 |
26000 |
400 |
20000 |
300 |
| D0.5 |
2 |
26000 |
300 |
26000 |
300 |
18000 |
200 |
| D0.5 |
4 |
24000 |
180 |
24000 |
180 |
16000 |
150 |
| D0.5 |
6 |
24000 |
150 |
24000 |
150 |
15000 |
100 |
| D0.6 |
2 |
26000 |
500 |
26000 |
500 |
20000 |
500 |
| D0.6 |
4 |
24000 |
300 |
24000 |
300 |
16000 |
200 |
| D0.6 |
6 |
22000 |
200 |
22000 |
200 |
16000 |
150 |
| D0.6 |
8 |
20000 |
150 |
20000 |
150 |
14000 |
100 |
| D0.8 |
2 |
18000 |
600 |
18000 |
600 |
18000 |
500 |
| D0.8 |
4 |
16000 |
400 |
16000 |
400 |
14000 |
300 |
| D0.8 |
6 |
16000 |
300 |
16000 |
300 |
14000 |
200 |
| D0.8 |
8 |
14000 |
150 |
14000 |
150 |
13000 |
150 |
| D1.0 |
4 |
13000 |
800 |
13000 |
800 |
12000 |
800 |
| D1.0 |
6 |
11000 |
600 |
11000 |
600 |
10000 |
600 |
| D1.0 |
8 |
10000 |
300 |
10000 |
300 |
9000 |
300 |
| D1.0 |
10 |
9000 |
150 |
9000 |
150 |
8000 |
120 |
| D1.5 |
4 |
13000 |
1200 |
13000 |
1200 |
13000 |
1000 |
| D1.5 |
6 |
11000 |
800 |
11000 |
800 |
11000 |
600 |
| D1.5 |
8 |
10000 |
500 |
10000 |
500 |
10000 |
400 |
| D1.5 |
10 |
9000 |
400 |
9000 |
400 |
9000 |
300 |
| D2.0 |
4 |
12000 |
1400 |
12000 |
1400 |
10000 |
1000 |
| D2.0 |
6 |
12000 |
1200 |
12000 |
1200 |
10000 |
800 |
| D2.0 |
8 |
10000 |
1000 |
10000 |
1000 |
9000 |
600 |
| D2.0 |
10 |
9500 |
600 |
9500 |
600 |
8000 |
400 |
| D2.0 |
12 |
8500 |
400 |
8500 |
400 |
7000 |
260 |
| D2.0 |
16 |
7000 |
300 |
7000 |
300 |
6000 |
200 |
Note:
*Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum spindle speed;
*Recommend oil coolant for Stainless Steels and Heat Resistance Alloys;
*Recommend using a non-contact measuring device to avoid damaging the precision tip point;
*Decrease both spindle speed and feed rate proportionally in case of chattering.