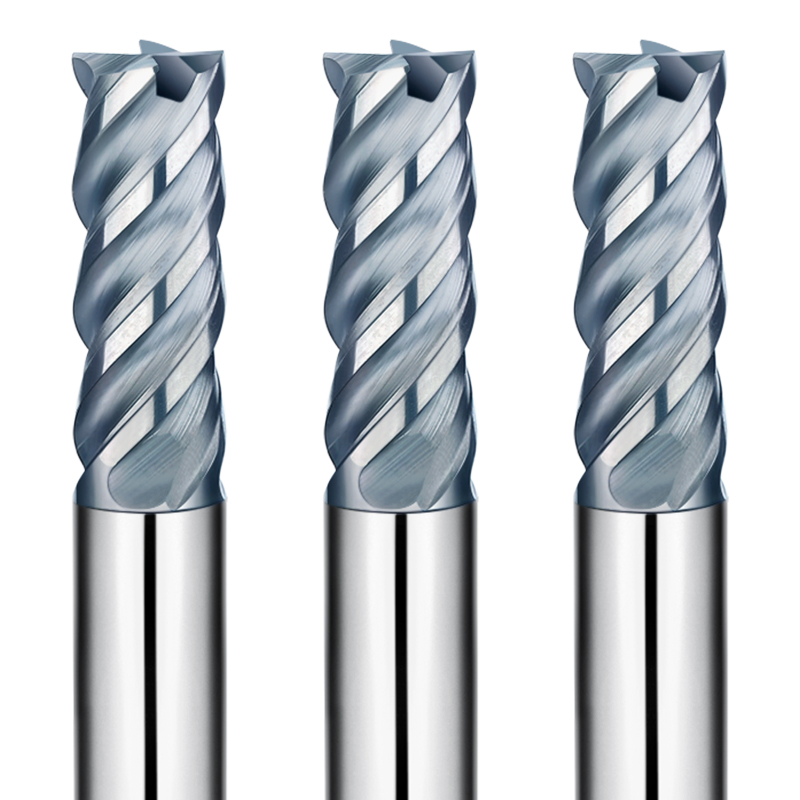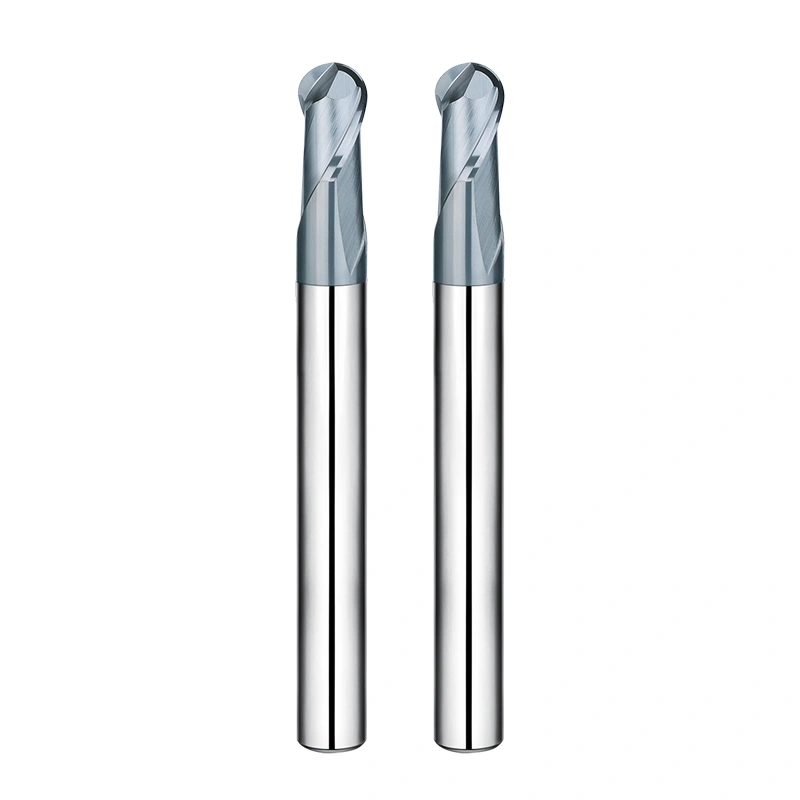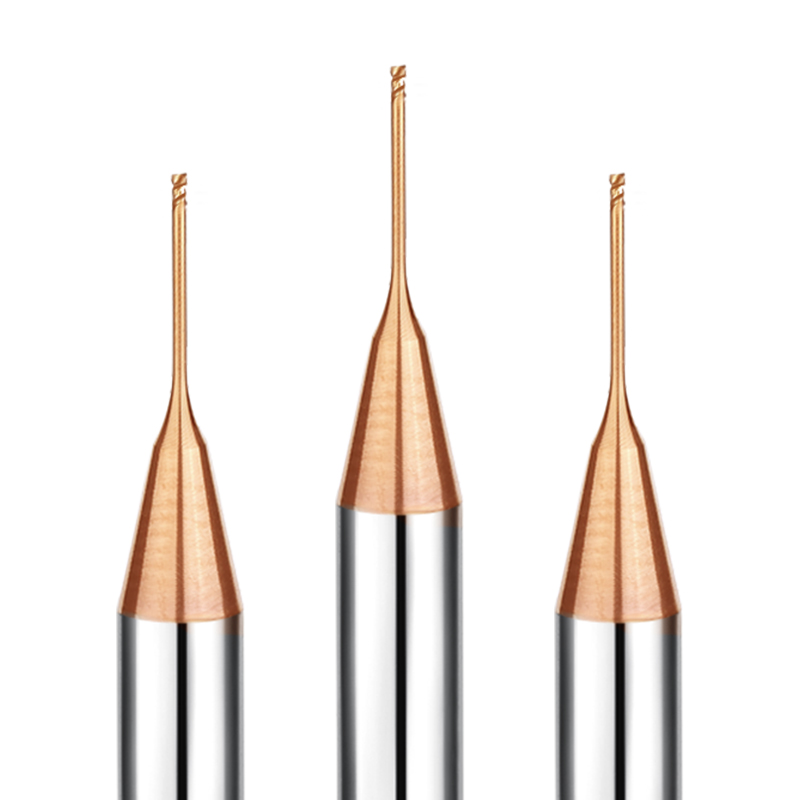
hrc55 end mills 2 flute long neck ball nose end mill 2

Tungsten Copper Long Neck Ball Nose End Mill

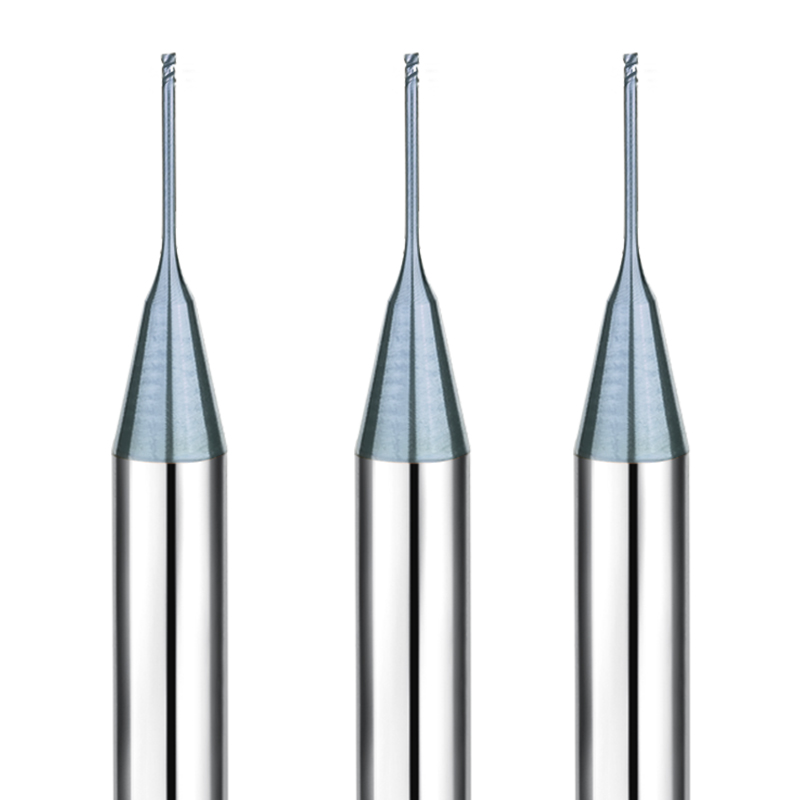
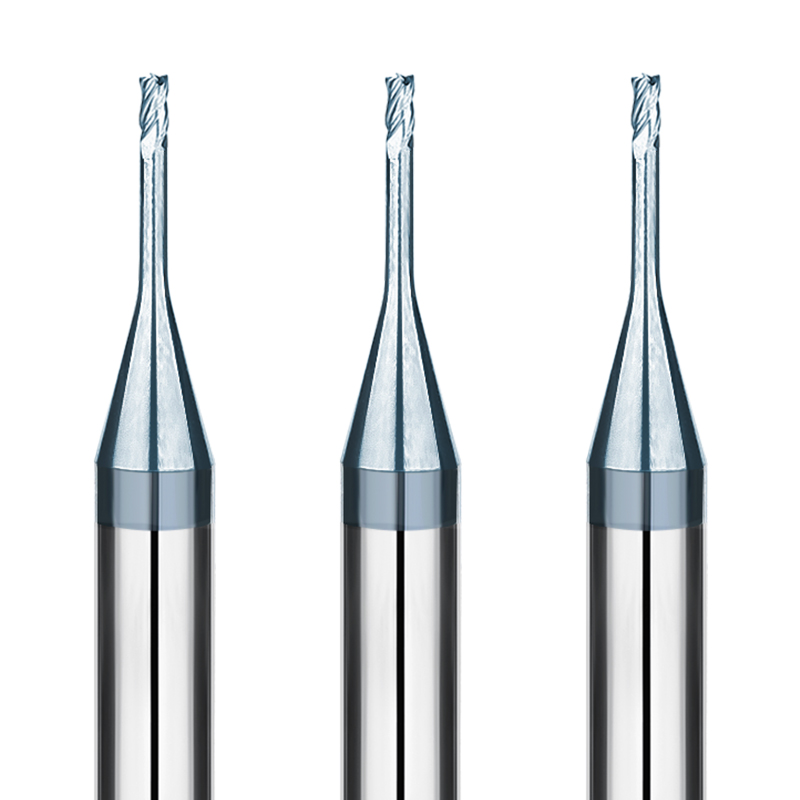
Struggling with tool interference in deep tungsten copper cavities? The SAMHO WCu Series provides the ultimate reach and precision. Specifically engineered for Tungsten Copper (WCu) alloys, these long-neck ball nose cutters feature optimized geometry for EDM electrodes, complex 3D contours, and micro-mold features.

Extended Reach: Long neck design for deep pocket clearance without tool deflection.

Micro-Precision: Ultra-fine radii starting from R0.1 mm for intricate detailing.

Wear Resistance: Premium ultra-fine grain carbide resists the abrasive nature of WCu.

Accuracy: 5-axis CNC ground to a strict ±0.01 mm dimensional tolerance.

In the manufacturing of complex EDM electrodes and micro-molds, reaching deep features while maintaining surface integrity is a major challenge. The SAMHO Long Neck WCu Series is engineered to provide the necessary clearance and stability for machining dense, abrasive tungsten copper alloys in high-precision CNC environments.


Advanced Technical Features

  • Long Neck Design for Interference-Free Deep Milling
    The specialized extended neck geometry is key for deep cavity and narrow feature access:
    • Access Deep Contours: Perfect for complex 3D electrode geometries and undercuts
    • Maintain Rigidity: Optimized neck-to-diameter ratios ensure stable cutting and minimize vibration, critical for WCu machining
  • Sharp 2-Flute Geometry for Low Cutting Resistance
    Tungsten copper is a dense composite that requires sharp cutting edges to prevent heat buildup:
    • Smooth Chip Evacuation: Rapid removal of debris to prevent chip welding
    • Lower Cutting Forces: Maintains accuracy in thin-walled features and delicate micro-structures
  • Ultra-Fine Grain Carbide for Extreme Wear Resistance
    SAMHO uses a premium ultra-fine grain solid carbide substrate:
    • Exceptional Hardness: Maintains sharp edges even under friction of dry machining or MQL
    • Chipping Resistance: Provides fracture toughness for consistent performance in dense non-ferrous composites
  • Ball Nose Tip for Precision 3D Surface Finishing
    Precision-ground hemispherical tip:
    • Mirror-Like Finishes: Reduces need for post-processing or manual polishing
    • Geometric Consistency: Vital for high-tolerance mold inserts where every micron counts

Comprehensive Model Selection (56 Models)

With 56 specialized models in the SHDLR series, we cover a radius range from R0.1 to R2.0 mm. Whether milling micro-fluidic channels or large-scale electrode cores, SAMHO has the exact size and neck length to fit your CNC requirements.


Target Applications & Industries

  • EDM Electrode Manufacturing: High-precision milling of WCu electrodes for aerospace and electronics
  • Micro-Mold Making: Intricate 3D cavity milling in dense, abrasive non-ferrous alloys
  • Medical & Automotive: Precision profiling of complex, high-tolerance components

Professional Usage Recommendations

  • Cooling Strategy: Use MQL (Minimum Quantity Lubrication) or dry machining with high-pressure air blast to manage thermal stability
  • Setup Accuracy: For micro-diameters (R0.1–R0.5 mm), use high-precision hydraulic or shrink-fit holders to minimize runout and maximize tool life
  • Tip Protection: Use non-contact measuring devices during tool setting to avoid damaging the precision-ground radius

Why Source Wholesale from SAMHO?

  • Wholesale Cost-Efficiency: Significant savings for global distributors and high-volume electrode shops
  • Proven Performance: Specialized substrates designed specifically for Tungsten Copper challenges
  • Rapid Global Shipping: 56+ models in stock and ready for immediate international dispatch
Recommended Materials for Machining (Highly Recommended: ⭐️ | Recommended: ⭕️ | Suggested: ◯)

DIE STEEL Grade
Carbon steels (S45C/S55C)
Alloy steels (SK/SCM/SUS)
Prehardened steels (NAK/HPM)
Hardened steels (~55/~60/~70HRC)
SPECIAL MATERIAL
Aluminum alloys
Graphite
Copper
Plastics
Tungsten copper ⭐
Carbon fiber
Titanium alloys
Heat resistant alloys
Cemented carbide
Hard brittle (non-metallic) material

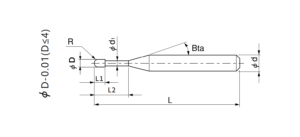
long neck ball nose end mill

Total 56 models

Model Number Outside Diameter Length of Cut Effective Length Shank Taper Angle Overall Length Number of Flutes Shank Diameter In Stock
CGLR2-002005 R0.1 0.2 0.5 15° 50 2 4 ○
CGLR2-002010 R0.1 0.2 1 15° 50 2 4 ○
CGLR2-002015 R0.1 0.2 1.5 15° 50 2 4 ○
CGLR2-003010 R0.15 0.3 1 15° 50 2 4 ○
CGLR2-003015 R0.15 0.3 1.5 15° 50 2 4 ○
CGLR2-003020 R0.15 0.3 2 15° 50 2 4 ○
CGLR2-003030 R0.15 0.3 3 15° 50 2 4 ○
CGLR2-004010 R0.2 0.4 1 15° 50 2 4 ○
CGLR2-004020 R0.2 0.4 2 15° 50 2 4 ○
CGLR2-004030 R0.2 0.4 3 15° 50 2 4 ○
CGLR2-004040 R0.2 0.4 4 15° 50 2 4 ○
CGLR2-005010 R0.25 0.5 1 15° 50 2 4 ○
CGLR2-005020 R0.25 0.5 2 15° 50 2 4 ○
CGLR2-005040 R0.25 0.5 4 15° 50 2 4 ○
CGLR2-005060 R0.25 0.5 6 15° 50 2 4 ○
CGLR2-005080 R0.25 0.5 8 15° 50 2 4 ○
CGLR2-006020 R0.3 0.6 2 15° 50 2 4 ○
CGLR2-006040 R0.3 0.6 4 15° 50 2 4 ○
CGLR2-006060 R0.3 0.6 6 15° 50 2 4 ○
CGLR2-006080 R0.3 0.6 8 15° 50 2 4 ○
CGLR2-008020 R0.4 0.8 2 15° 50 2 4 ○
CGLR2-008040 R0.4 0.8 4 15° 50 2 4 ○
CGLR2-008060 R0.4 0.8 6 15° 50 2 4 ○
CGLR2-008080 R0.4 0.8 8 15° 50 2 4 ○
CGLR2-010020 R0.5 1 2 15° 50 2 4 ○
CGLR2-010040 R0.5 1 4 15° 50 2 4 ○
CGLR2-010060 R0.5 1 6 15° 50 2 4 ○
CGLR2-010080 R0.5 1 8 15° 50 2 4 ○
CGLR2-010100 R0.5 1 10 15° 50 2 4 ○
CGLR2-010120 R0.5 1 12 15° 50 2 4 ○
CGLR2-010140 R0.5 1 14 15° 50 2 4 ○
CGLR2-010160 R0.5 1 16 15° 50 2 4 ○
CGLR2-015040 R0.75 1.5 4 15° 50 2 4 ○
CGLR2-015060 R0.75 1.5 6 15° 50 2 4 ○
CGLR2-015080 R0.75 1.5 8 15° 50 2 4 ○
CGLR2-015100 R0.75 1.5 10 15° 50 2 4 ○
CGLR2-015120 R0.75 1.5 12 15° 50 2 4 ○
CGLR2-015140 R0.75 1.5 14 15° 50 2 4 ○
CGLR2-015160 R0.75 1.5 16 15° 50 2 4 ○
CGLR2-020040 R1 2 4 15° 50 2 4 ○
CGLR2-020060 R1 2 6 15° 50 2 4 ○
CGLR2-020080 R1 2 8 15° 50 2 4 ○
CGLR2-020100 R1 2 10 15° 50 2 4 ○
CGLR2-020120 R1 2 12 15° 50 2 4 ○
CGLR2-020160 R1 2 16 15° 50 2 4 ○
CGLR2-030060 R1.5 3 6 15° 50 2 4 ○
CGLR2-030080 R1.5 3 8 15° 50 2 4 ○
CGLR2-030100 R1.5 3 10 15° 50 2 4 ○
CGLR2-030120 R1.5 3 12 15° 50 2 4 ○
CGLR2-030160 R1.5 3 16 15° 50 2 4 ○
CGLR2-030200 R1.5 3 20 15° 50 2 4 ○
CGLR2-040080 R2 4 8 — 50 2 4 ○
CGLR2-040100 R2 4 10 — 50 2 4 ○
CGLR2-040120 R2 4 12 — 50 2 4 ○
CGLR2-040160 R2 4 16 — 50 2 4 ○
CGLR2-040200 R2 4 20 – 50 2 4 ○

Milling Conditions

Work Material Tungsten Copper
Radius of Ball Nose (mm)Effective Length (min-1)Speed (mm/min)Feed Ap(mm) Ae(mm)
R0.1 0.5 30000 120 0.006 0.006
R0.1 1 30000 100 0.003 0.003
R0.1 1.5 30000 100 0.003 0.003
R0.15 1 26000 200 0.006 0.006
R0.15 1.5 26000 200 0.004 0.004
R0.15 2 24000 150 0.003 0.003
R0.15 3 18000 100 0.003 0.003
R0.2 1 2400 300 0.01 0.01
R0.2 2 20000 200 0.008 0.01
R0.2 3 18000 150 0.006 0.006
R0.2 4 16000 150 0.003 0.003
R0.25 1 20000 600 0.01 0.01
R0.25 2 18000 600 0.01 0.01
R0.25 4 16000 300 0.008 0.008
R0.25 6 14000 150 0.008 0.008
R0.25 8 14000 100 0.003 0.003
R0.3 2 20000 800 0.02 0.02
R0.3 4 15000 500 0.01 0.01
R0.3 6 13000 300 0.008 0.008
R0.3 8 13000 150 0.005 0.005
R0.4 2 18000 1200 0.02 0.02
R0.4 4 18000 800 0.02 0.02
R0.4 6 16000 600 0.01 0.02
R0.4 8 15000 400 0.005 0.01
R0.5 2 14000 1200 0.02 0.03
R0.5 4 14000 1000 0.02 0.03
R0.5 6 14000 800 0.02 0.03
R0.5 8 12000 500 0.01 0.02
R0.5 10 12000 400 0.01 0.02
R0.5 12 10000 300 0.01 0.02
R0.5 14 10000 200 0.008 0.01
R0.5 16 10000 200 0.005 0.01
R0.75 4 16000 1400 0.02 0.04
R0.75 6 14000 1200 0.02 0.04
R0.75 8 13000 1000 0.02 0.04
R0.75 10 12000 600 0.01 0.04
R0.75 12 11000 500 0.01 0.04
R0.75 14 10000 400 0.01 0.02
R0.75 16 9000 300 0.01 0.01
R1 4 16000 2000 0.03 0.06
R1 6 14000 1800 0.03 0.06
R1 8 14000 1800 0.03 0.06
R1 10 14000 1800 0.03 0.06
R1 12 12000 1400 0.02 0.06
R1 16 10000 1000 0.02 0.06
R1.5 6 16000 2000 0.03 0.06
R1.5 8 14000 1800 0.03 0.06
R1.5 10 14000 1800 0.03 0.06
R1.5 12 14000 1800 0.03 0.06
R1.5 16 12000 1400 0.02 0.06
R1.5 20 10000 1000 0.02 0.06
R2 8 12000 2200 0.03 0.07
R2 10 12000 2200 0.03 0.07
R2 12 12000 2200 0.03 0.07
R2 16 12000 2200 0.03 0.07
R2 20 11000 2000 0.03 0.07

Note:
*Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum spindle speed;
*Recommend using a non-contact measuring device to avoid damaging the precision tip point.

Download 2: Tungsten Copper Long Neck Ball Nose End Mill File

Related Product

Related Post

graphite end mill

Graphite 4 Flutes Flat End Mill

In graphite manufacturing, machining operations place exceptionally high demands on cutting tools, requiring both precise performance and long-lasting durability. The SAMHO diamond coated 4 flute

Read More »
thread mill

HRC65 RC/PT Full Tooth Thread Mill

In high-hardness material machining, cutting tool performance requirements are extremely demanding. Tools must maintain stable cutting in hardened steel up to HRC65. At the same

Read More »
grinding head

Emery Thread Grinding Head

In the field of machining hard and brittle materials, cutting tools face exceptionally rigorous demands. They must deliver extreme precision, outstanding wear resistance, and stable

Read More »
Get Your Custom Milling Tool Guide

Fill out the form below to receive SAMHO’s complete product catalog.