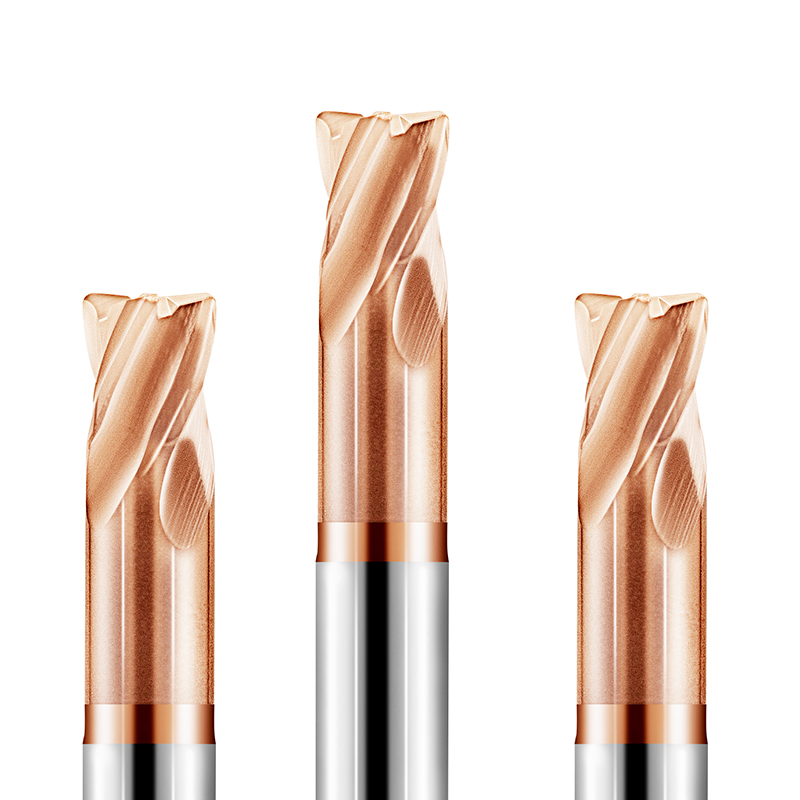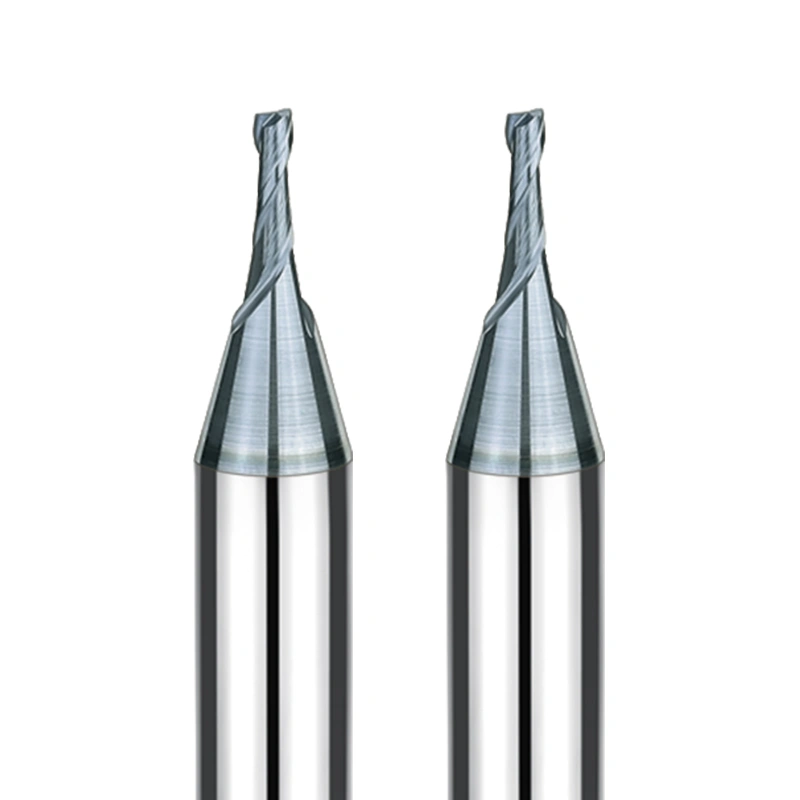
hrc65 end mills 2 flute ball nose end mill2 hrc65 end mills 2 flute ball nose end mill3 hrc65 end mills 2 flute ball nose end mill1

hrc65 end mills 2 flute ball nose end mill

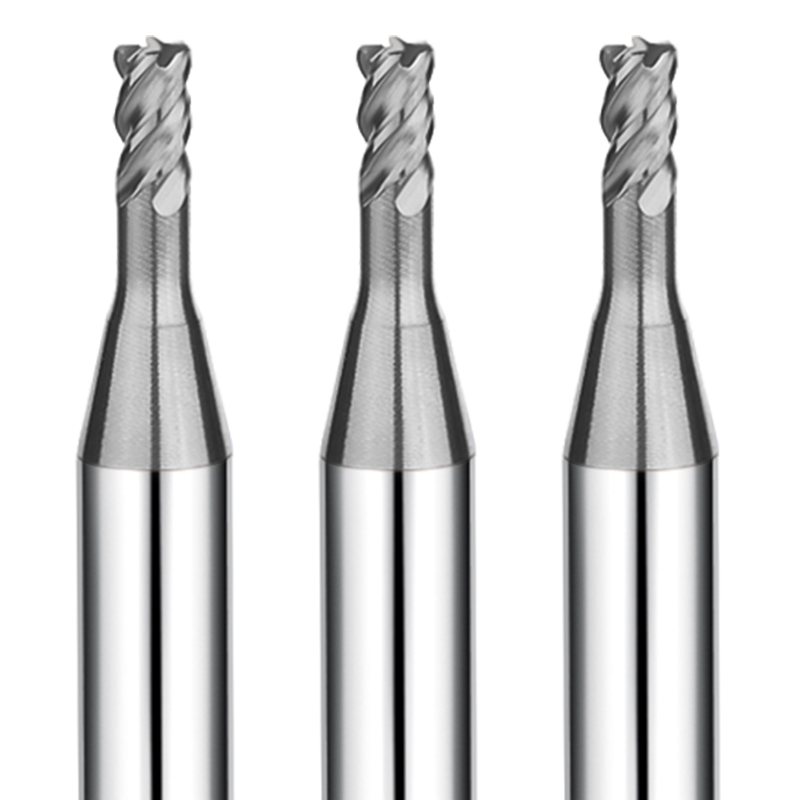
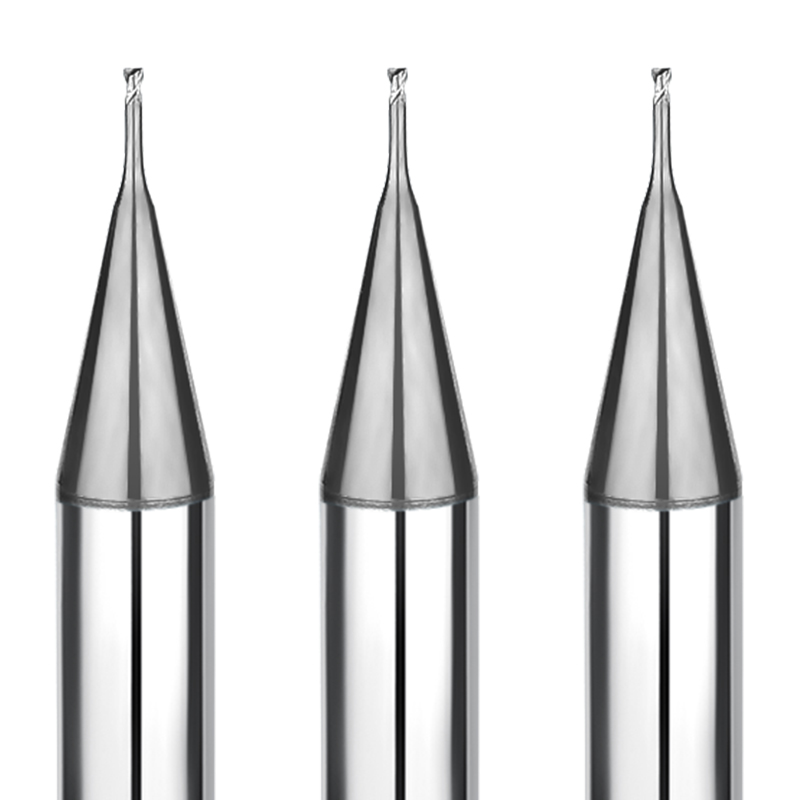
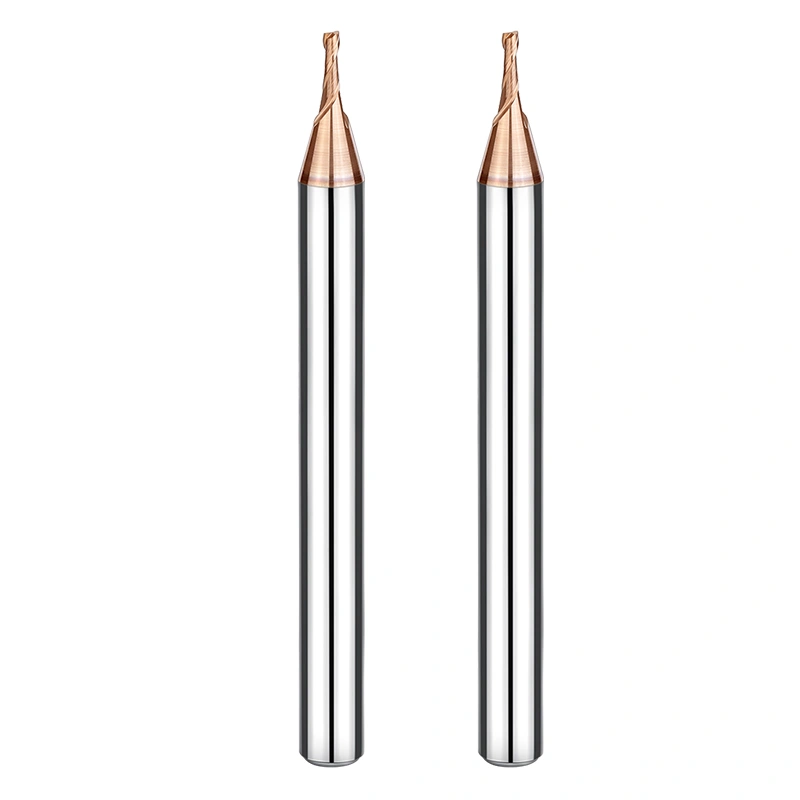
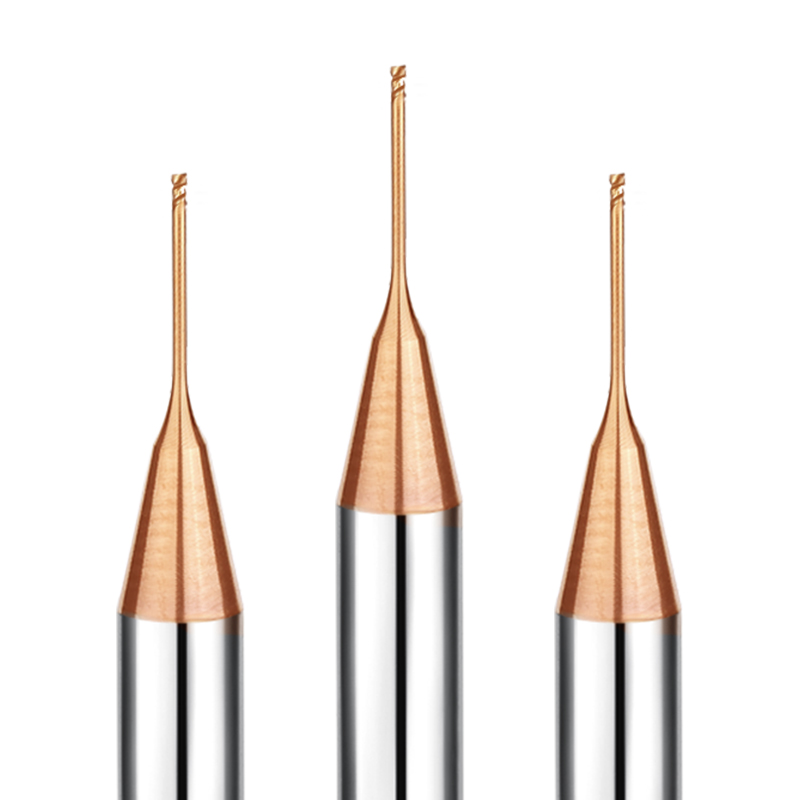
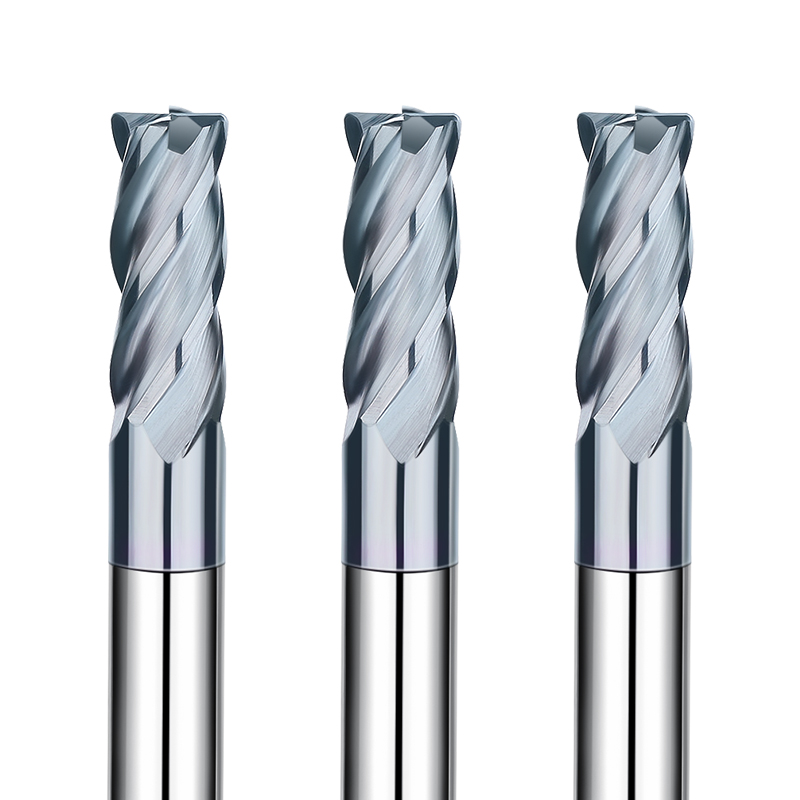
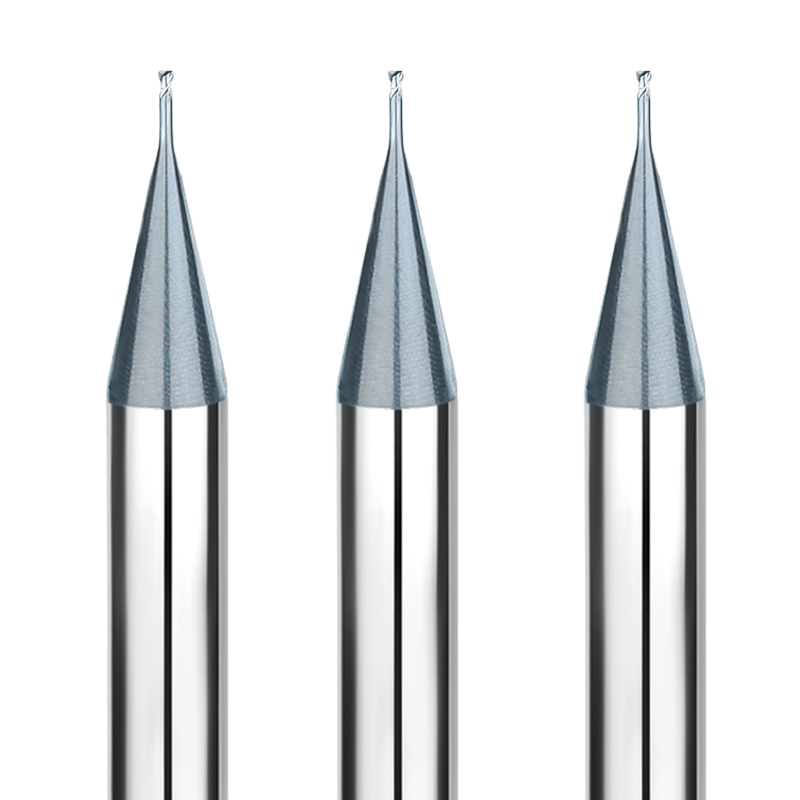
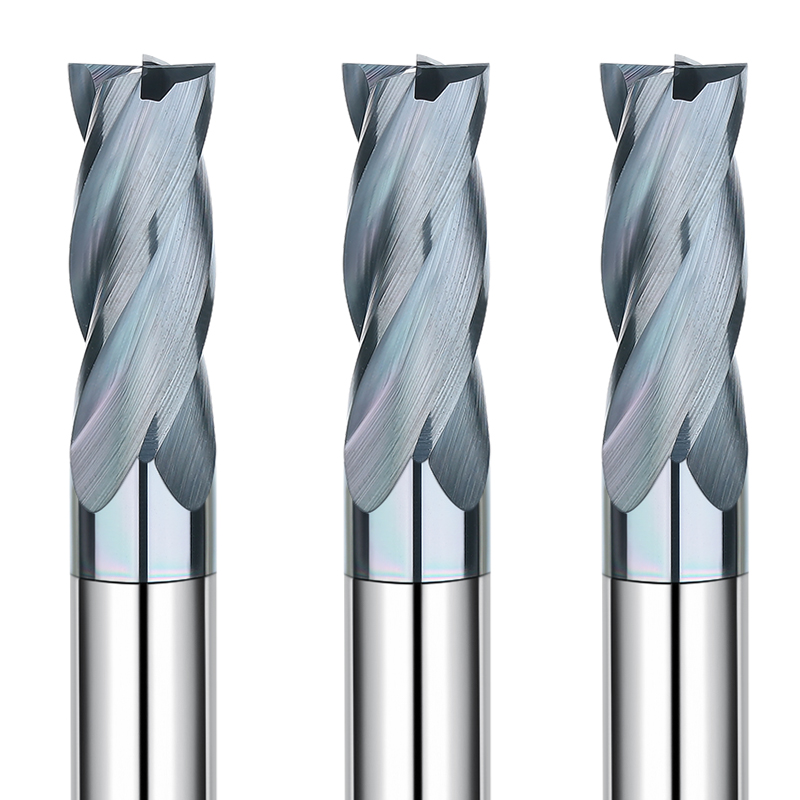
Achieve superior surface integrity on hardened materials with the SAMHO SHGR2 Series. Specifically engineered for steels up to 65HRC, this carbide ball nose cutter is the professional choice for 3D profiling, sculpted features, and mold finishing.

Size Range: Comprehensive selection from R0.15 to R10.0 mm (36 models).

Design: 2-flute geometry for maximum chip evacuation and reduced vibration.

Performance: High-hardness coating enables stable, high-speed dry machining.

Supply: Wholesale factory-direct pricing with OEM customization options.

Precision mold-making and aerospace components require tools that can withstand extreme heat while maintaining a perfect hemispherical geometry. The SAMHO HRC65 2-flute ball nose series delivers exceptional dimensional accuracy and mirror-like finishes on materials up to HRC65.


Core Engineering & Technical Benefits

  • Specifically Engineered for High-Hardness Steel (Up to HRC65)
    Manufactured from an ultra-fine grain carbide substrate, these end mills possess the fracture toughness needed for hardened tool steels and die steels. The high-performance wear-resistant coating ensures long tool life and stable performance during prolonged finishing cycles
  • 2-Flute Geometry for Efficient Chip Evacuation
    Ample chip space is critical when machining deep cavities or narrow 3D contours:
    • Greater Stability: Ideal for semi-finishing and fine finishing
    • Improved Accuracy: Consistent radius tolerance for perfect rest milling and blending
  • Optimized for Complex 3D Contouring
    Precision-ground hemispherical tip:
    • Surface Finishing: Eliminates scalloping marks in complex 3D profiles
    • Intricate Features: From micro-molds (R0.15 mm) to large die cores (R10 mm), ensuring surface integrity across all scales
  • High Red Hardness Coating for Dry Machining
    Thermal-resistant coating maintains edge sharpness at elevated temperatures, supporting high-speed machining (HSM) under dry or MQL conditions, enhancing sustainability and reducing manufacturing costs

Comprehensive Model Selection (36 Models)

Covers a diameter range from Φ0.3 mm (R0.15 mm) to Φ20 mm (R10 mm). Perfect for micro-medical components or large-scale automotive dies, all in stock for immediate use


Usage Guidelines for Peak Performance

  • Overhang Sensitivity: For best results, use the shortest possible overhang. If the overhang exceeds 3×D, decrease spindle speed and feed rate proportionally
  • Coolant Strategy: Use Air/Mist cooling for hardened steel and oil coolant for stainless steels or heat-resistant alloys
  • Setup Safety: Use non-contact tool setters to avoid damaging the radius during setup

Why Partner with SAMHO for Wholesale?

  • Tested Parameters: Field-tested cutting data provided to reduce setup time
  • Bulk Availability: High stock levels on all 36 models for rapid global fulfillment
  • OEM Customization: Custom shank lengths or specialized coatings available upon request
Recommended Materials for Machining (Highly Recommended: ⭐️ | Recommended: ⭕️ | Suggested: ◯)

Category Work Material Grade
DIE STEEL Carbon steels (S45C/S55C) ◯
Alloy steels (SK/SCM/SUS) ◯
Prehardened steels (NAK/HPM) ⭕️
Hardened steels (~55/~60/~70HRC) ⭕️
SPECIAL MATERIAL Aluminum alloys
Graphite
Copper ◯
Plastics
Carbon fiber
Titanium alloys ◯
Heat resistant alloys
Cemented carbide
Hard brittle (non-metallic) material

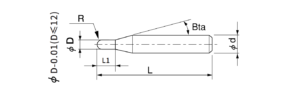
ball nose end mill

Total 36 models

Model Number Outside Diameter Length Of Cut Effective Length Shank Taper Angle Overall Length Number Of Flutes Shank Diameter In Stock
SHGR2-003003 R0.15 0.45 – 12° 50 2 4 ○
SHGR2-004004 R0.2 0.6 – 12° 50 2 4 ○
SHGR2-005005 R0.25 0.8 – 12° 50 2 4 ○
SHGR2-006006 R0.3 0.9 – 12° 50 2 4 ○
SHGR2-008008 R0.4 1.2 – 12° 50 2 4 ○
SHGR2-010010 R0.5 1 – 12° 50 2 4 ○
SHGR2-015025 R0.75 1.5 2.5 12° 50 2 4 ○
SHGR2-020040 R1 2 4 12° 50 2 4 ○
SHGR2-020040-6 R1 2 4 12° 60 2 6 ○
SHGR2-030060-3 R1.5 3 6 – 50 2 3 ○
SHGR2-030060-4 R1.5 3 6 12° 50 2 4 ○
SHGR2-030060-6 R1.5 3 6 12° 60 2 6 ○
SHGR2-040080-4 R2 4 8 – 50 2 4 ○
SHGR2-040080-6 R2 4 8 12° 60 2 6 ○
SHGR2-050100 R2.5 5 10 12° 60 2 6 ○
SHGR2-060120 R3 6 12 – 60 2 6 ○
SHGR2-060120-75 R3 6 12 – 75 2 6 ○
SHGR2-060120-100 R3 6 12 – 100 2 6 ○
SHGR2-080160 R4 8 16 – 60 2 8 ○
SHGR2-080160-75 R4 8 16 – 75 2 8 ○
SHGR2-080160-100 R4 8 16 – 100 2 8 ○
SHGR2-080160-150 R4 8 16 – 150 2 8 ○
SHGR2-100200 R5 10 20 – 75 2 10 ○
SHGR2-100200-100 R5 10 20 – 100 2 10 ○
SHGR2-100200-150 R5 10 20 – 150 2 10 ○
SHGR2-120240 R6 12 24 – 75 2 12 ○
SHGR2-120240-100 R6 12 24 – 100 2 12 ○
SHGR2-120240-150 R6 12 24 – 150 2 12 ○
SHGR2-140280-100 R7 14 28 – 100 2 14 ○
SHGR2-140280-150 R7 14 28 – 150 2 14 ○
SHGR2-160320-100 R8 16 32 – 100 2 16 ○
SHGR2-160320-150 R8 16 32 – 150 2 16 ○
SHGR2-180360-100 R9 18 36 – 100 2 18 ○
SHGR2-180360-150 R9 18 36 – 150 2 18 ○
SHGR2-200400-100 R10 20 40 – 100 2 20 ○
SHGR2-200400-150 R10 20 40 – 150 2 20 ○

Milling Conditions

Work Material HRC30-45 Prehardened Steels HRC45-55 Hardened Steels HRC55-65 Hardened Steels
Radius of Ball Nose (min-1)Speed (mm/min)Feed Ap (mm)Axial Depth Ae (mm)Radidl Depth (min-1)Speed (mm/min)Feed Ap (mm)Axial Depth Ae (mm)Radidl Depth (min-1)Speed (mm/min)Feed Ap (mm)Axial Depth Ae (mm)Radidl Depth
R0.15 26000 300 0.01 0 24000 200 0.008 0.008 20000 200 0.005 0.005
R0.2 22000 400 0.015 0.015 22000 300 0.01 0.01 18000 300 0.008 0.008
R0.25 20000 400 0.015 0.015 22000 400 0.015 0.015 16000 400 0.008 0.008
R0.3 20000 800 0.02 0.02 20000 600 0.015 0.015 15000 500 0.015 0.015
R0.4 18000 1200 0.02 0.03 20000 800 0.02 0.02 13000 600 0.02 0.02
R0.5 16000 1200 0.03 0.04 18000 1000 0.02 0.03 12000 700 0.02 0.03
R0.75 16000 1500 0.03 0.05 16000 1200 0.02 0.04 10000 800 0.02 0.04
R1 15000 1800 0.03 0.05 14000 1800 0.02 0.05 9000 1200 0.02 0.04
R1 15000 1800 0.04 0.05 14000 1800 0.02 0.05 9000 1400 0.02 0.04
R1.5 14000 2200 0.04 0.07 13000 2200 0.03 0.06 9000 1200 0.02 0.05
R1.5 14000 2200 0.05 0.07 13000 2200 0.03 0.06 9000 1300 0.02 0.05
R1.5 14000 2200 0.04 0.07 13000 2200 0.03 0.06 9000 1500 0.02 0.05
R2 14000 2400 0.04 0.08 12000 2400 0.03 0.06 8000 1500 0.02 0.06
R2 14000 2400 0.05 0.08 12000 2400 0.03 0.06 8000 1500 0.02 0.06
R2.5 12000 2600 0.05 0.08 12000 2400 0.03 0.06 8000 1500 0.02 0.06
R3 12000 2600 0.05 0.08 10000 2600 0.03 0.08 7000 1800 0.02 0.08
R4 10000 3000 0.05 0.1 9000 2800 0.03 0.1 6500 2200 0.02 0.1
R5 9000 3000 0.05 0.12 8000 2800 0.03 0.12 6000 2200 0.02 0.1
R6 9000 3000 0.05 0.15 7000 2800 0.03 0.12 5000 2000 0.02 0.12
R7 7000 3000 0.08 0.15 6000 2800 0.03 0.15 4000 2000 0.02 0.15
R8 6000 3000 0.08 0.15 5500 2800 0.03 0.15 4000 2000 0.02 0.15
R9 5000 3000 0.08 0.15 4500 2800 0.03 0.15 4000 2000 0.02 0.15
R10 4500 3000 0.08 0.15 4000 2800 0.03 0.15 4000 2000 0.02 0.15

Note:
The above milling parameters are calculated based on 3xD. Decrease both spindle speed and feed rate proportionally if the overhang length exceeds 3xD;
*Recommend oil coolant for Stainless Steels and Heat Resistance Alloys;
*Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum spindle speed.

Download 2: hrc65 end mills 2 flute ball nose end mill File

Related Product

Related Post

hrc65 NPT full teeth thread mill

In the manufacturing of high-pressure fittings and precision molds, threading after heat treatment is a critical challenge. The SAMHO HRC65 Full-Tooth NPT Series is designed

Read More »
Get Your Custom Milling Tool Guide

Fill out the form below to receive SAMHO’s complete product catalog.