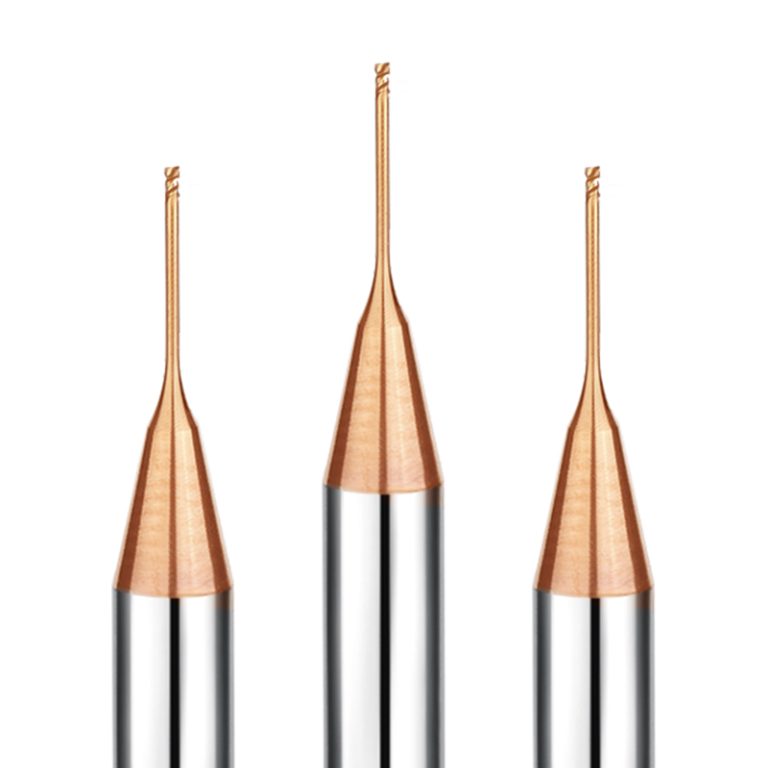
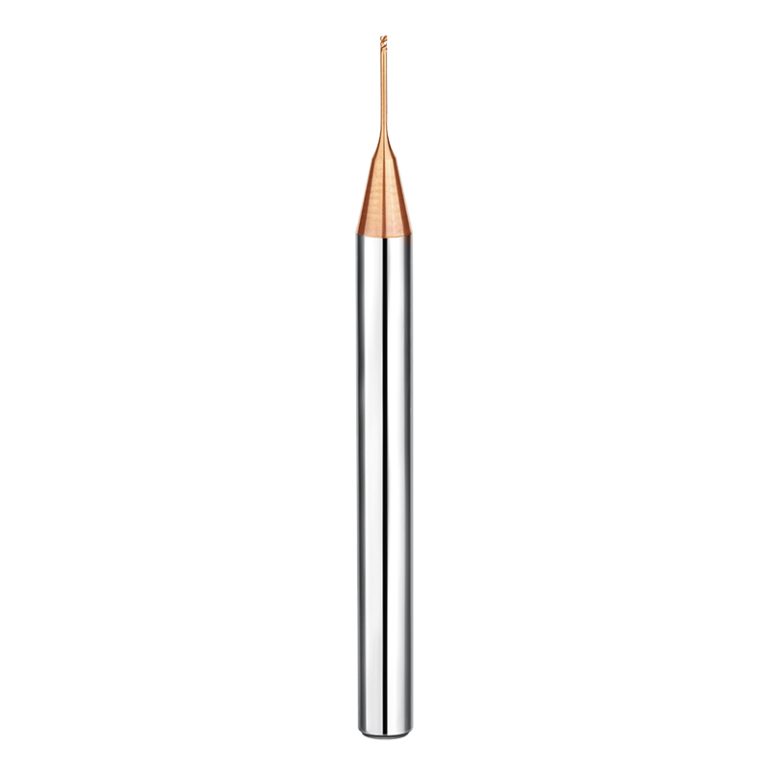
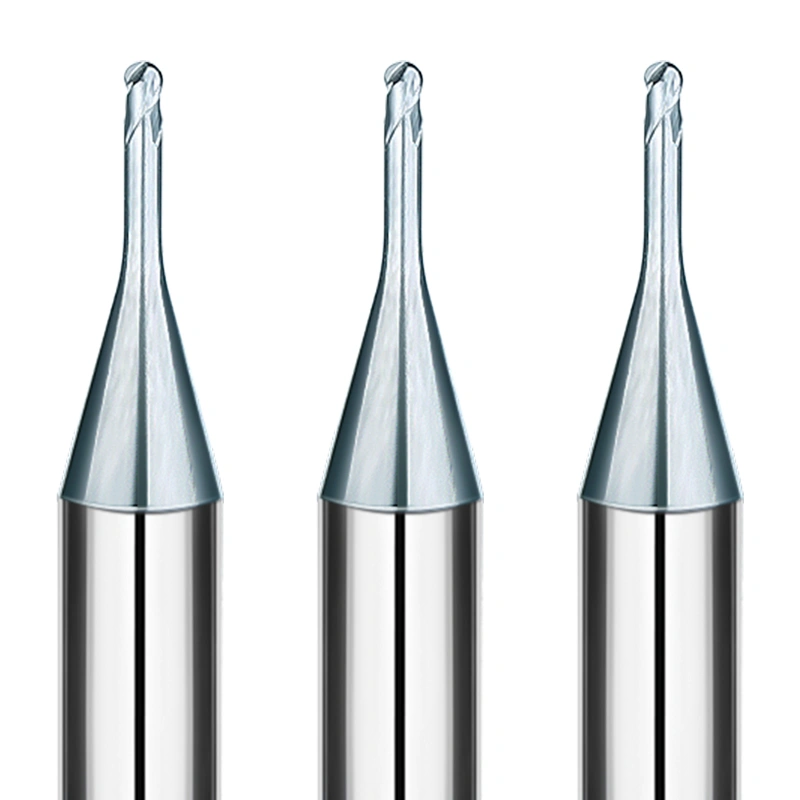
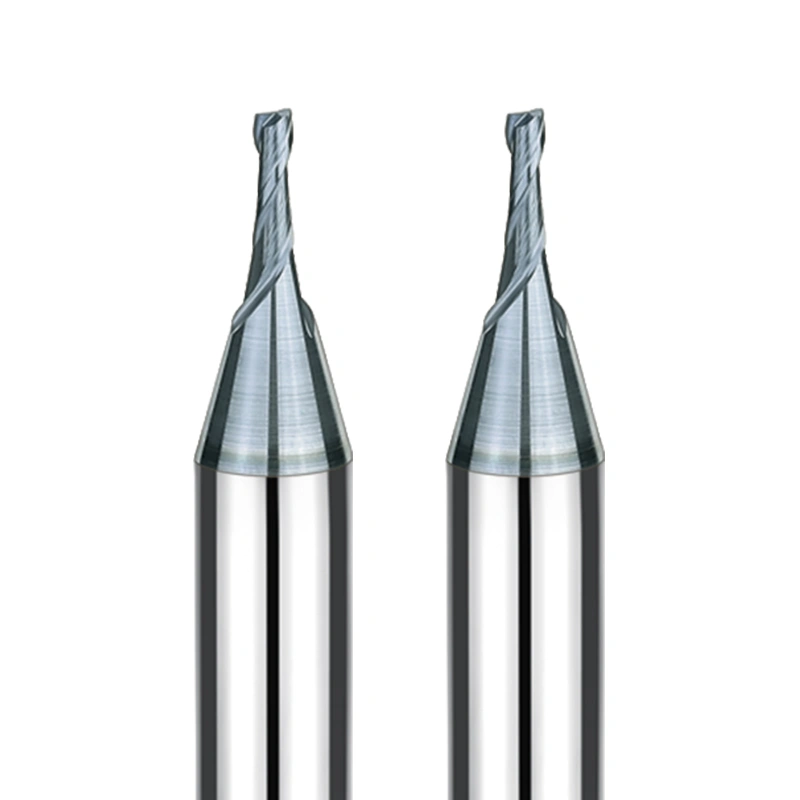
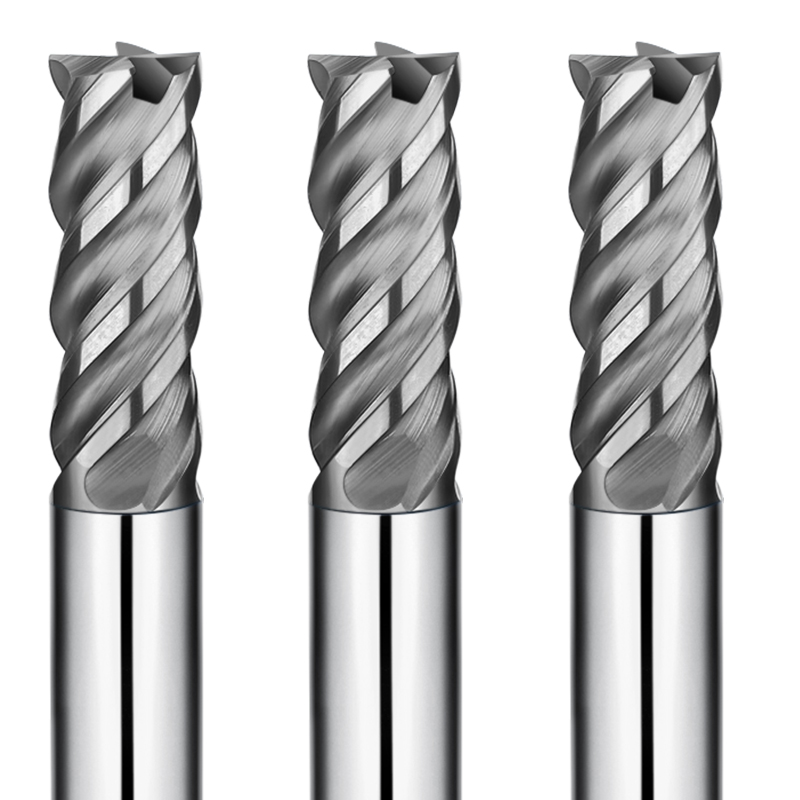
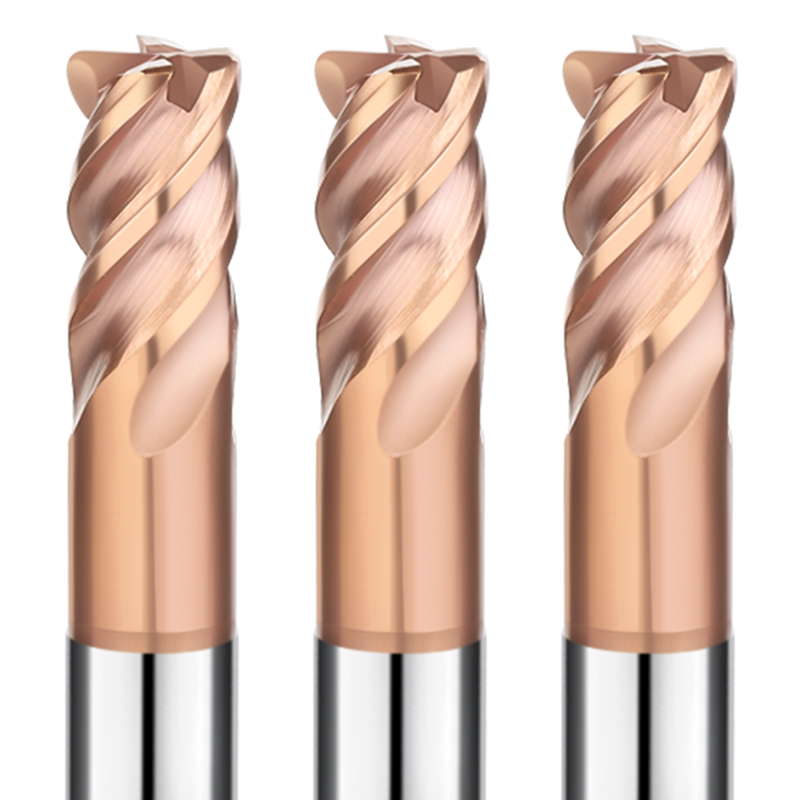
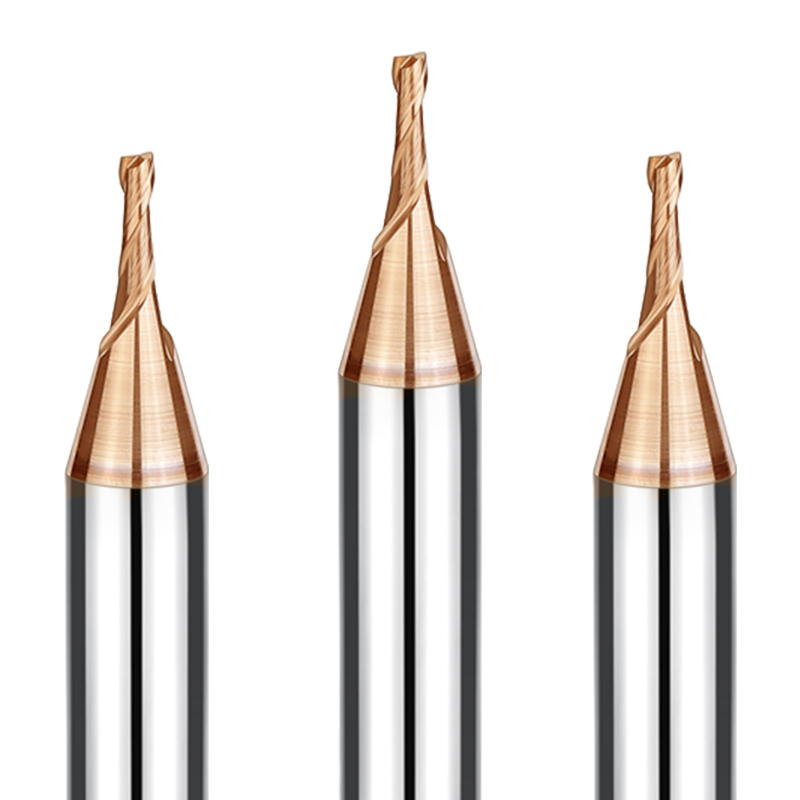
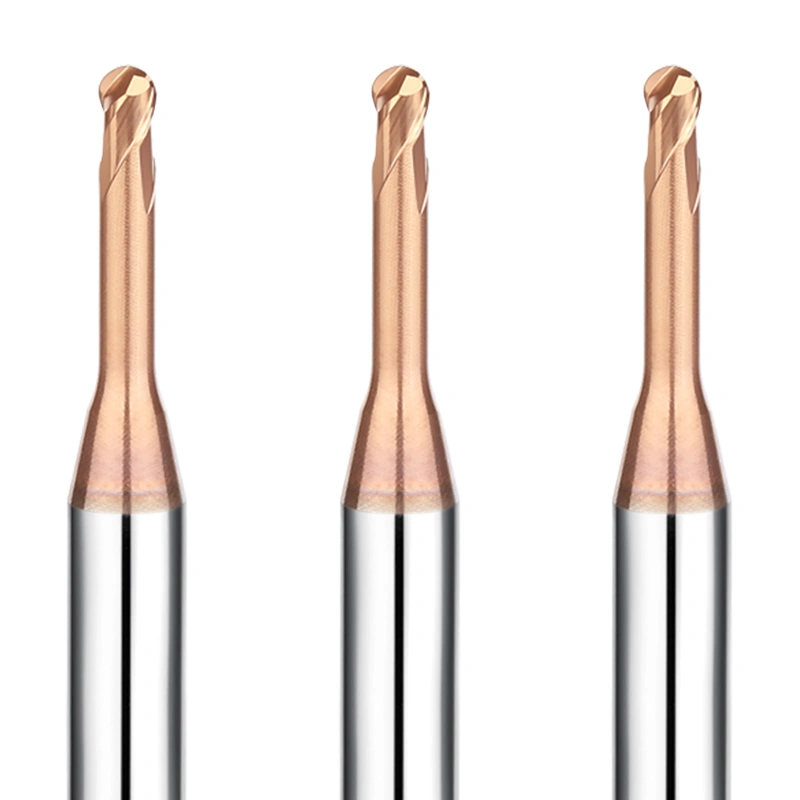
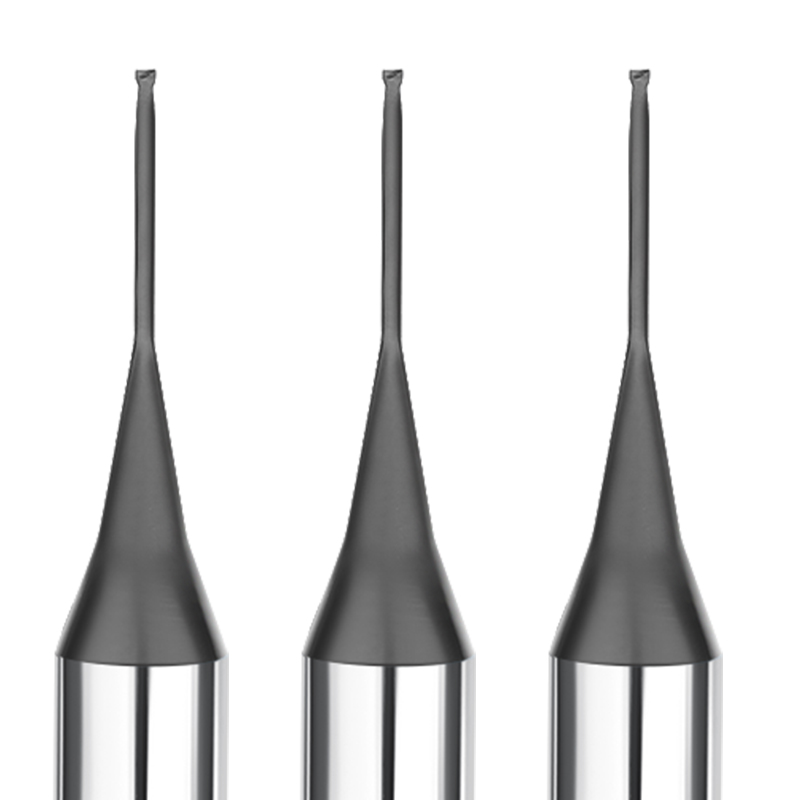
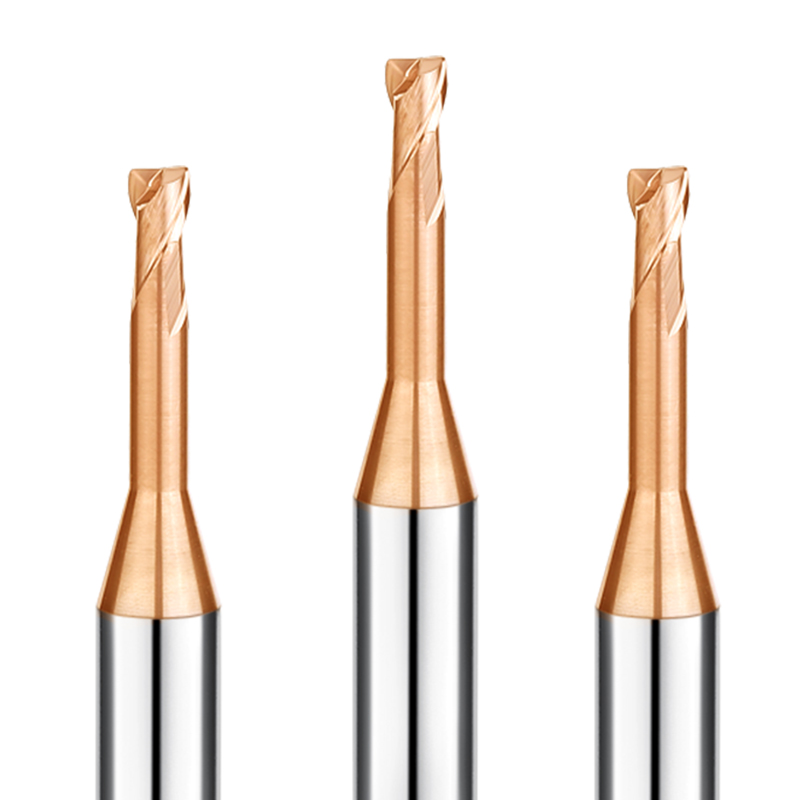
In the field of hardened steel machining, tool requirements are extremely demanding. CNC operators need tools that deliver both precise cutting and superior wear resistance. The SAMHO coated 2-flute long neck flat end mill bit (D0.2-0.8 mm) is engineered to meet these high-intensity machining demands. It is specifically designed for CNC machining of hardened steel and high-hardness alloys, providing reliable performance and long-lasting durability.
Advanced Technical Features
High-Adhesion Coating for Ultra-Long Service Life
The SAMHO coated 2-flute long neck square end mill features a proprietary high-adhesion coating that provides exceptional hardness and chemical inertness:
- Wear Resistance: Maintains a sharp cutting edge even during prolonged, high-intensity CNC machining of hardened steel.
- Micro-Chipping Prevention: The coating adheres firmly to the carbide substrate, even under high-speed friction and extreme heat.
Precision Cutting-Edge Geometry for Hardened Steel
This double-flute, long-neck, flat-bottom end mill is engineered for efficient machining of complex contours and deep cavities:
- Efficient Cutting: Sharp double flutes reduce cutting heat and improve chip evacuation.
- Reduced Load: Minimizes heat buildup, preventing thermal cracking in hardened steel workpieces.
Ultra-Fine Grain Carbide Substrate and High-Precision Grinding
The tool is constructed with a high-strength, ultra-fine grain carbide substrate and finished with a high-precision grinding process to ensure superior performance:
- Dimensional Accuracy: Tolerances are strictly controlled within ±0.01 mm, ensuring consistent batch production.
- Fracture Resistance: Significantly improves tool durability, ideal for machining highly abrasive hardened steels.
High-Efficiency Double-Flute “Cold Cutting” Design
- Maximized Chip Evacuation: Quickly clears heat and debris from the cutting zone.
- Enhanced Machining Stability: Extends tool life and supports prolonged, high-precision CNC operations.
Target Applications & Industries
This series of 2-flute, long-neck, flat-end CNC end mills is widely applicable for:
- Precision Machining of Hardened Steel: Designed for high-precision cutting of high-hardness steel workpieces.
- Deep-Hole and Complex Contour Machining: Efficiently machines deep cavities, internal corners, and intricate structures.
- Machining of High-Hardness Alloys and Wear-Resistant Materials: Provides excellent tool stability and long-term durability.
- High-Precision Batch Processing: Ensures dimensional consistency and repeatable CNC machining results.
Why Choose SAMHO as Your Wholesale Partner?
This series of 2-flute, long-neck, flat-end CNC end mills is widely applicable for:
- Precision Machining of Hardened Steel: Designed for high-precision cutting of high-hardness steel workpieces.
- Deep-Hole and Complex Contour Machining: Efficiently machines deep cavities, internal corners, and intricate structures.
- Machining of High-Hardness Alloys and Wear-Resistant Materials: Provides excellent tool stability and long-term durability.
- High-Precision Batch Processing: Ensures dimensional consistency and repeatable CNC machining results.
Recommended Materials for Machining (Highly Recommended: ⭐️ | Recommended: ⭕️ | Suggested: ◯)
| Category |
Work Material |
Grade |
| DIE STEEL |
Carbon steels (S45C/S55C) |
|
|
Alloy steels (SK/SCM/SUS) |
|
|
Prehardened steels (NAK/HPM) |
|
|
Hardened steels (~55/~60/~70HRC) |
⭐️ |
| SPECIAL MATERIAL |
Aluminum alloys |
|
|
Graphite |
|
|
Copper |
|
|
Plastics |
|
|
Carbon fiber |
|
|
Titanium alloys |
|
|
Heat resistant alloys |
|
|
Cemented carbide |
|
|
Hard brittle (non-metallic) material |
|
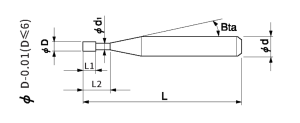
Total 23 models
| Model Number |
Outside Diameter |
Length Of Cut |
Effective Length |
Shank Taper Angle |
Overall Length |
Number Of Flutes |
Shank Diameter |
In Stock |
| SHHLS2-002005 |
0.2 |
0.3 |
0.5 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-002010 |
0.2 |
0.3 |
1 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-002015 |
0.2 |
0.3 |
1.5 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-003010 |
0.3 |
0.5 |
1 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-003015 |
0.3 |
0.5 |
1.5 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-003020 |
0.3 |
0.5 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-003030 |
0.3 |
0.5 |
3 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-004010 |
0.4 |
0.6 |
1 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-004020 |
0.4 |
0.6 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-004030 |
0.4 |
0.6 |
3 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-004040 |
0.4 |
0.6 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-005010 |
0.5 |
0.75 |
1 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-005020 |
0.5 |
0.75 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-005040 |
0.5 |
0.75 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-005060 |
0.5 |
0.75 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-006020 |
0.6 |
0.9 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-006040 |
0.6 |
0.9 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-006060 |
0.6 |
0.9 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-006080 |
0.6 |
0.9 |
8 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-008020 |
0.8 |
1.2 |
2 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-008040 |
0.8 |
1.2 |
4 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-008060 |
0.8 |
1.2 |
6 |
12° |
50 |
2 |
4 |
○ |
| SHHLS2-008080 |
0.8 |
1.2 |
8 |
12° |
50 |
2 |
4 |
○ |
Contour Milling Parameters
| Work Material |
HRC48-55 hardened steel |
HRC56-62 hardened steel |
HRC63-70 hardened steel |
| Diameter |
Effective Length(mm) |
(min-1) Speed |
(mm/min) Feed |
(mm) Axial depth |
(mm) Radidl depth |
(min-1) Speed |
(mm/min) Feed |
(mm) Axial depth |
(mm) Radidl depth |
(min-1) Speed |
(mm/min) Feed |
(mm) Axial depth |
(mm) Radidl depth |
| 0.2 |
0.5 |
30000 |
200 |
0.003 |
0.1 |
30000 |
160 |
0.003 |
0.08 |
30000 |
120 |
0.003 |
0.06 |
| 0.2 |
1 |
30000 |
150 |
0.003 |
0.1 |
30000 |
120 |
0.003 |
0.08 |
30000 |
80 |
0.003 |
0.06 |
| 0.2 |
1.5 |
30000 |
100 |
0.002 |
0.1 |
30000 |
80 |
0.002 |
0.08 |
30000 |
60 |
0.002 |
0.06 |
| 0.3 |
1 |
30000 |
300 |
0.003 |
0.15 |
30000 |
250 |
0.003 |
0.12 |
30000 |
200 |
0.003 |
0.09 |
| 0.3 |
1.5 |
30000 |
200 |
0.003 |
0.15 |
30000 |
160 |
0.003 |
0.12 |
30000 |
120 |
0.003 |
0.09 |
| 0.3 |
2 |
30000 |
150 |
0.003 |
0.15 |
30000 |
120 |
0.003 |
0.12 |
25000 |
100 |
0.003 |
0.09 |
| 0.3 |
3 |
25000 |
50 |
0.002 |
0.15 |
25000 |
40 |
0.002 |
0.12 |
25000 |
30 |
0.002 |
0.09 |
| 0.4 |
1 |
30000 |
400 |
0.005 |
0.2 |
30000 |
350 |
0.005 |
0.16 |
25000 |
300 |
0.005 |
0.12 |
| 0.4 |
2 |
30000 |
320 |
0.005 |
0.2 |
25000 |
280 |
0.005 |
0.16 |
25000 |
220 |
0.005 |
0.12 |
| 0.4 |
3 |
25000 |
360 |
0.004 |
0.2 |
20000 |
220 |
0.003 |
0.16 |
18000 |
180 |
0.003 |
0.12 |
| 0.4 |
4 |
25000 |
200 |
0.003 |
0.2 |
20000 |
160 |
0.002 |
0.16 |
18000 |
120 |
0.002 |
0.12 |
| 0.5 |
1 |
25000 |
500 |
0.01 |
0.25 |
23000 |
450 |
0.007 |
0.2 |
20000 |
400 |
0.005 |
0.15 |
| 0.5 |
2 |
25000 |
420 |
0.01 |
0.25 |
23000 |
380 |
0.007 |
0.2 |
20000 |
320 |
0.005 |
0.15 |
| 0.5 |
4 |
25000 |
280 |
0.005 |
0.25 |
23000 |
240 |
0.003 |
0.2 |
20000 |
200 |
0.002 |
0.15 |
| 0.5 |
6 |
20000 |
200 |
0.003 |
0.25 |
18000 |
150 |
0.002 |
0.2 |
16000 |
100 |
0.002 |
0.15 |
| 0.6 |
2 |
25000 |
500 |
0.01 |
0.3 |
23000 |
400 |
0.007 |
0.25 |
18000 |
350 |
0.005 |
0.18 |
| 0.6 |
4 |
25000 |
400 |
0.005 |
0.3 |
23000 |
300 |
0.003 |
0.25 |
18000 |
250 |
0.002 |
0.18 |
| 0.6 |
6 |
20000 |
300 |
0.002 |
0.3 |
18000 |
200 |
0.002 |
0.25 |
16000 |
150 |
0.001 |
0.18 |
| 0.6 |
8 |
20000 |
300 |
0.002 |
0.3 |
18000 |
200 |
0.002 |
0.25 |
16000 |
150 |
0.001 |
0.18 |
| 0.8 |
2 |
25000 |
780 |
0.03 |
0.4 |
23000 |
650 |
0.02 |
0.32 |
20000 |
550 |
0.012 |
0.24 |
| 0.8 |
4 |
25000 |
700 |
0.025 |
0.4 |
23000 |
600 |
0.015 |
0.32 |
20000 |
500 |
0.007 |
0.24 |
| 0.8 |
6 |
20000 |
550 |
0.02 |
0.4 |
18000 |
450 |
0.01 |
0.32 |
16000 |
350 |
0.005 |
0.24 |
| 0.8 |
8 |
16000 |
400 |
0.007 |
0.4 |
14000 |
300 |
0.005 |
0.32 |
12000 |
200 |
0.003 |
0.24 |
Note:
*Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum spindle speed;
*Recommend oil coolant for Stainless Steels and Heat Resistance Alloys;
*Recommend using a non-contact measuring device to avoid damaging the precisiontip point;
*Decrease both spindle speed and feed rate proportionally in case of chattering;
*When the material hardness is greater than HRC58 degrees, it is recommended to use air blow cooling for roughing andoil mistor air blow cooling for finishing.