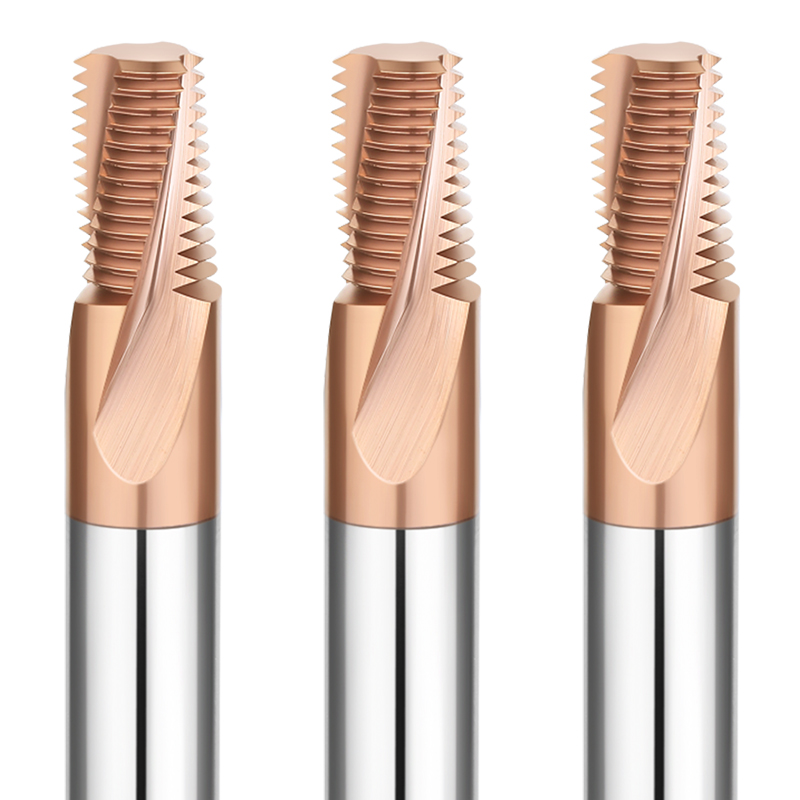
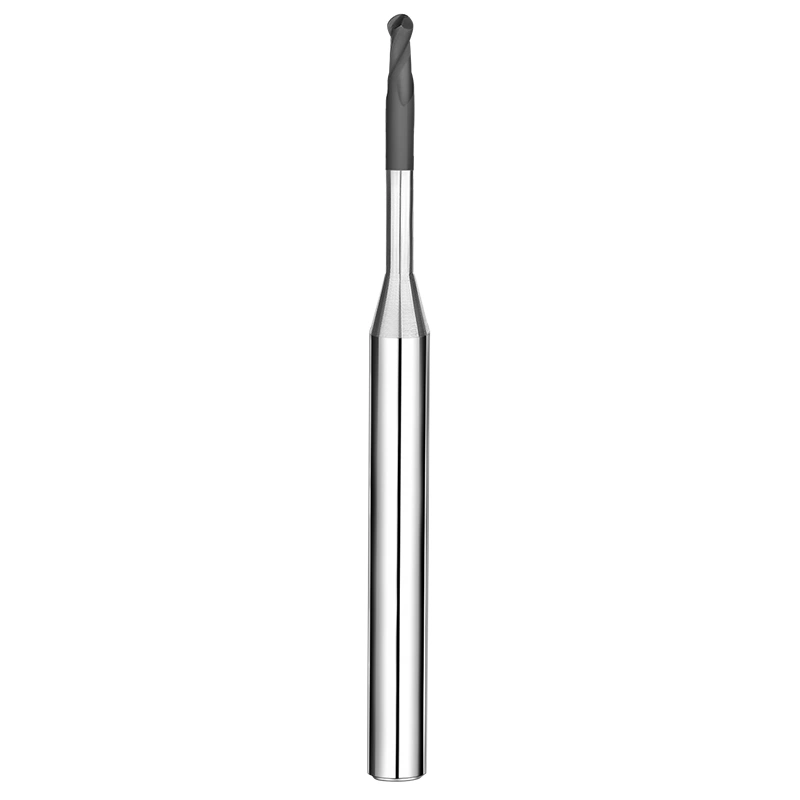
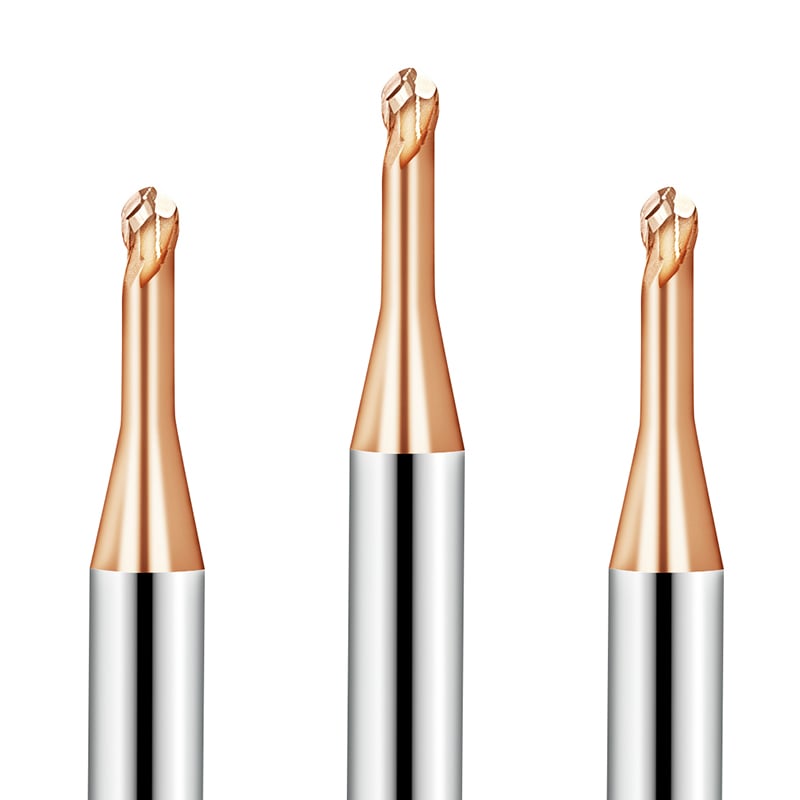
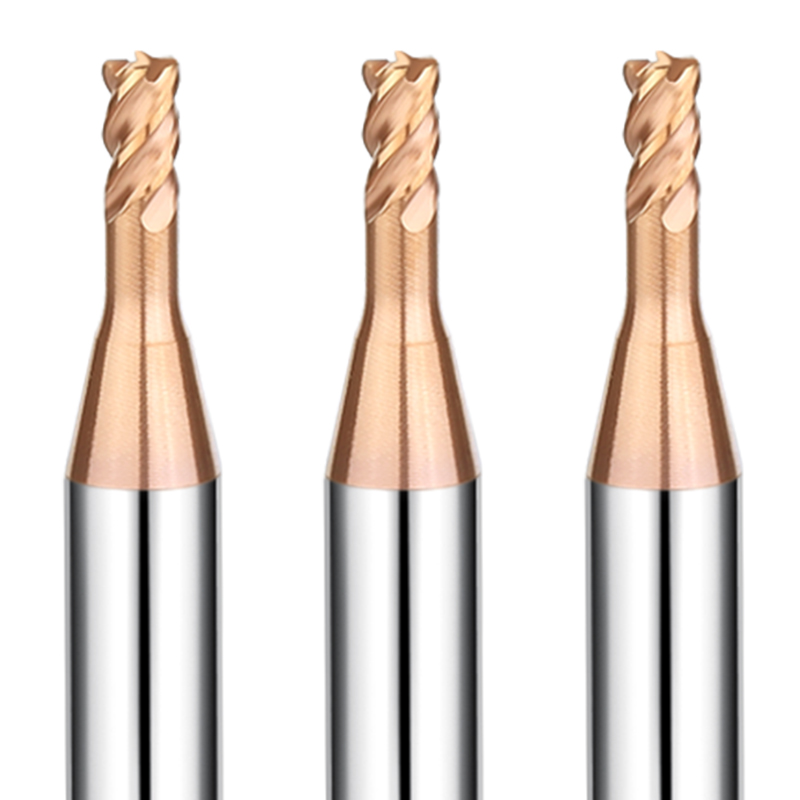
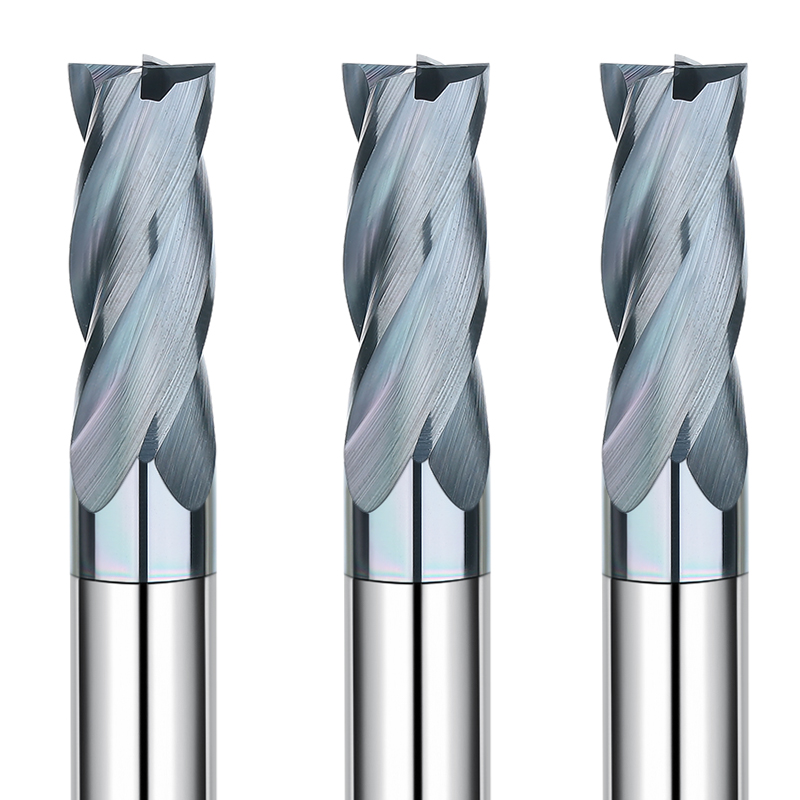
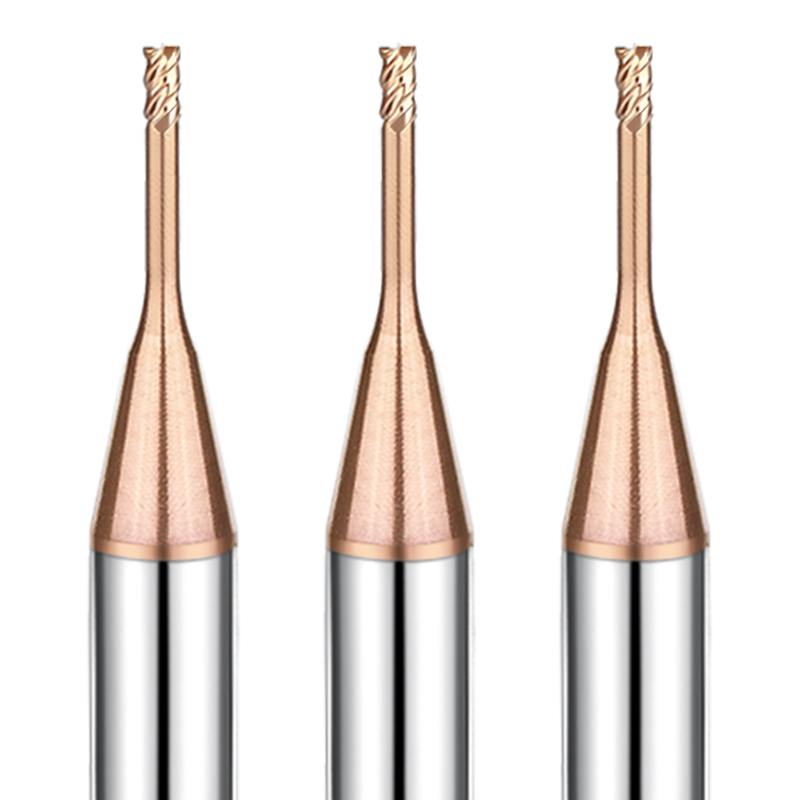
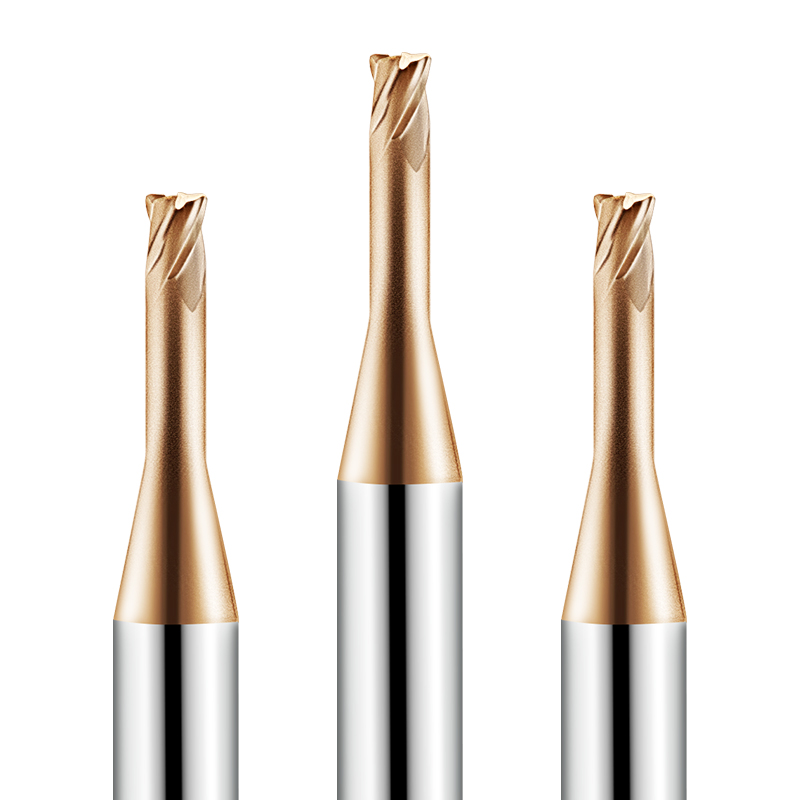
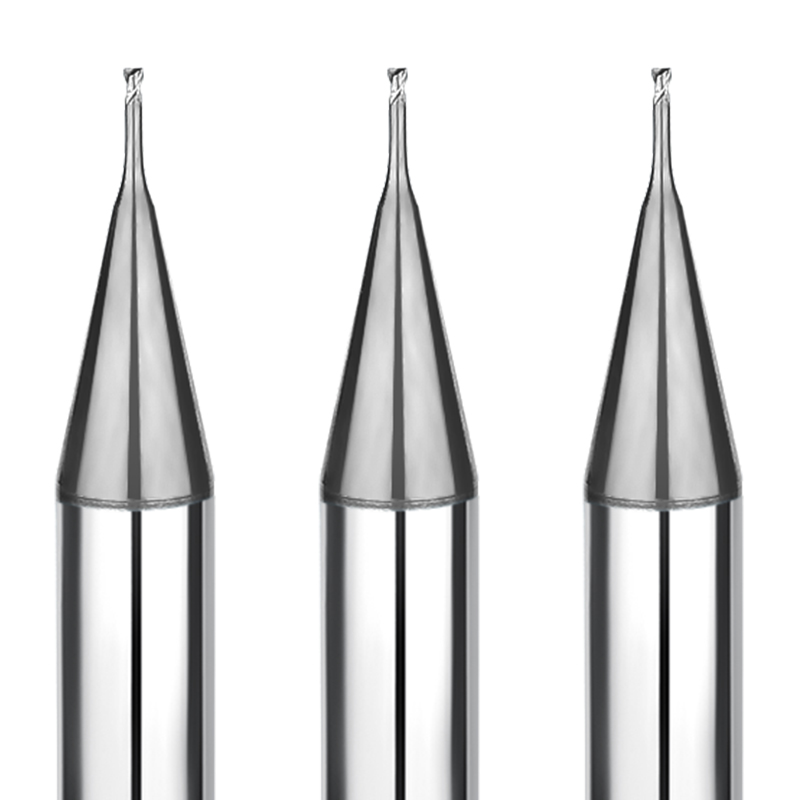
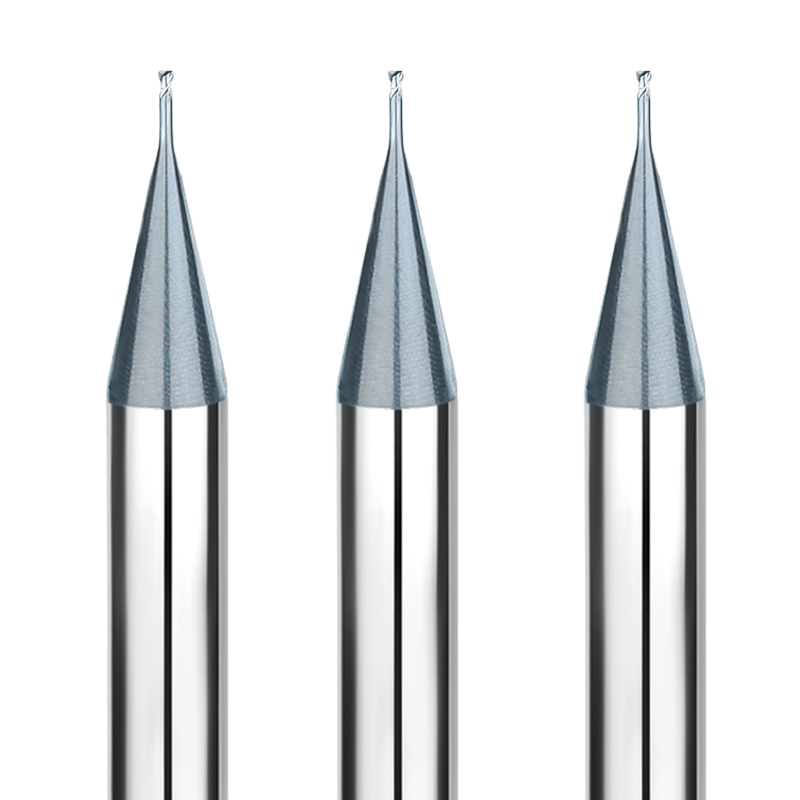
In the world of high-precision manufacturing, micro-features require tools that balance extreme accuracy with robust durability. The SAMHO HRC55 2-Flute Flat End Mill is designed to meet the rigorous demands of CNC operators working with aluminum alloys, pre-hardened steels, and non-ferrous metals.
Core Technical Advantages
- Superior Micro-Diameter Performance (Φ0.2 to Φ6.0 mm)
Our Micro Flat End Mill series is tailored for processing intricate details and complex curved surfaces. Whether milling micro-fluidic channels or precision electronic housings, these tools provide the dimensional consistency your project requires
- Optimized 2-Flute Spiral Design
Engineered to facilitate:
- Rapid Chip Evacuation: Prevents heat buildup in deep-groove or slotting operations
- Cutting Stability: Minimizes vibration and chatter in high-speed CNC environments
- Multi-Stage Capability: Handles roughing, semi-finishing, and finishing cycles with a single tool
- Advanced Coating for HRC55 Versatility
Crafted from high-grade solid carbide with a heat-resistant coating, this tool maintains edge sharpness across a wide range of materials:
- Alloy & Carbon Steels: Reliable performance in general engineering
- Copper & Aluminum: Exceptional surface finishes in non-ferrous mold making
- Medical Equipment: High-precision milling of surgical-grade components
- Data-Driven Tool Protection
SAMHO provides application-specific milling parameters (Speed, Feed, Depth of Cut) to:
- Protect the tool’s micro-diameter tip
- Improve machining efficiency
- Significantly reduce production costs
Professional Usage Recommendations
- Spindle Speed Management: If CNC machine cannot reach recommended RPMs, proportionally decrease both spindle speed and feed rate
- Coolant Strategy: Use oil coolant for stainless steels and heat-resistant alloys to prevent edge wear
- Precision Setup: For micro-diameter tips (Φ0.2–0.5 mm), use non-contact measuring devices
- Vibration Control: Reduce feed rates if chattering occurs to maintain desired surface finish
Why Partner with SAMHO China?
- Industrial-Grade Quality: 15+ models covering Φ0.2–6.0 mm in stock
- Unbeatable Wholesale Prices: Direct-from-factory deals for global distributors and large-scale workshops
- OEM & Customization: Specialized coatings or custom neck lengths available via our dedicated engineering team
Recommended Materials for Machining (Highly Recommended: ⭐️ | Recommended: ⭕️ | Suggested: ◯)
| Category |
Work Material |
Grade |
| DIE STEEL |
Carbon steels (S45C/S55C) |
⭕️ |
|
Alloy steels (SK/SCM/SUS) |
⭕️ |
|
Prehardened steels (NAK/HPM) |
⭕️ |
|
Hardened steels (~55/~60/~70HRC) |
◯ |
| SPECIAL MATERIAL |
Aluminum alloys |
◯ |
|
Graphite |
|
|
Copper |
⭕️ |
|
Plastics |
|
|
Carbon fiber |
|
|
Titanium alloys |
◯ |
|
Heat resistant alloys |
|
|
Cemented carbide |
|
|
Hard brittle (non-metallic) material |
|
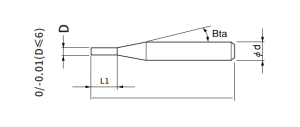
Total 15 models
| Model Number |
Outside Diameter |
Length Of Cut |
Effective Length |
Shank Taper Angle |
Overall Length |
Number Of Flutes |
Shank Diameter |
In Stock |
| SHBS2-0020040 |
0.2 |
0.4 |
– |
12° |
50 |
2 |
4 |
○ |
| SHBS2-0030060 |
0.3 |
0.6 |
– |
12° |
50 |
2 |
4 |
○ |
| SHBS2-0040080 |
0.4 |
0.8 |
– |
12° |
50 |
2 |
4 |
○ |
| SHBS2-0050100 |
0.5 |
1 |
– |
12° |
50 |
2 |
4 |
○ |
| SHBS2-0060150 |
0.6 |
1.5 |
– |
12° |
50 |
2 |
4 |
○ |
| SHBS2-0070180 |
0.7 |
1.8 |
– |
12° |
50 |
2 |
4 |
○ |
| SHBS2-0080200 |
0.8 |
2 |
– |
12° |
50 |
2 |
4 |
○ |
| SHBS2-0100300 |
1 |
3 |
– |
12° |
50 |
2 |
4 |
○ |
| SHBS2-0150400 |
1.5 |
4 |
– |
12° |
50 |
2 |
4 |
○ |
| SHBS2-0200500 |
2 |
5 |
– |
12° |
50 |
2 |
4 |
○ |
| SHBS2-0250650 |
2.5 |
6.5 |
– |
12° |
50 |
2 |
4 |
○ |
| SHBS2-0300800-4 |
3 |
8 |
– |
12° |
50 |
2 |
4 |
○ |
| SHBS2-0401000-4 |
4 |
10 |
– |
– |
50 |
2 |
4 |
○ |
| SHBS2-0401000-6 |
4 |
10 |
– |
12° |
60 |
2 |
6 |
○ |
| SHBS2-0601500 |
6 |
15 |
– |
– |
60 |
2 |
6 |
○ |
Side Milling
| Work Material |
Oxygen-free Copper Red Copper |
HRC30-45 carbon steel and prehardened steel |
HRC45-55 hardened steel |
| (mm)Diameter |
(min-1)Speed |
(mm/min)Feed |
(min-1)Speed |
(mm/min)Feed |
(min-1)Speed |
(mm/min)Feed |
| D1.0 |
10000 |
150 |
10000 |
100 |
8000 |
60 |
| D1.5 |
8000 |
180 |
8000 |
120 |
6000 |
60 |
| D2.0 |
8000 |
200 |
7000 |
120 |
5000 |
60 |
| D2.5 |
6000 |
300 |
6000 |
120 |
4500 |
60 |
| D3 |
7000 |
300 |
5000 |
150 |
4000 |
80 |
| D4 |
7000 |
300 |
4000 |
150 |
4000 |
100 |
| D4 |
7000 |
300 |
4000 |
150 |
4000 |
100 |
| D6 |
7000 |
300 |
3500 |
250 |
3000 |
200 |
Milling Amountfor Side Milling(mm)
| Work Material \ Length of Cut |
2.5D (Length of Cut=Diameter*2.5) |
4D (Length of Cut=Diameter*4) |
| Below 45HRC |
ae=0.07D ap=2D |
ae=0.07D ap=2D |
| Above 45HRC |
ae=0.03D ap=1.5D |
ae=0.03D ap=1.5D |
D:Diameter (mm)
ap:Axial Depth (mm)
ae: Radial Depth (mm)
Note:
*Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum spindle speed;
*Recommend oil coolant for Stainless Steels and Heat Resistance Alloys;
*Recommend using a non-contact measuring device to avoid damaging the precision tip point;
*Decrease both spindle speed and feed rate proportionally in case of chattering.
Contour Milling
| Work Material |
Oxygen-free Copper Red Copper |
HRC30-45 carbon steel and prehardened steel |
HRC45-55 hardened steel |
| (mm)Diameter |
(min-1)Speed |
(mm/min)Feed |
(min-1)Speed |
(mm/min)Feed |
(min-1)Speed |
(mm/min)Feed |
| D0.2 |
30000 |
200 |
30000 |
120 |
30000 |
120 |
| D0.3 |
30000 |
220 |
30000 |
150 |
30000 |
150 |
| D0.3 |
30000 |
300 |
30000 |
200 |
30000 |
200 |
| D0.3 |
26000 |
300 |
26000 |
200 |
26000 |
200 |
| D0.3 |
24000 |
500 |
24000 |
300 |
24000 |
300 |
| D0.3 |
20000 |
500 |
20000 |
500 |
20000 |
500 |
| D0.3 |
16000 |
800 |
16000 |
800 |
16000 |
800 |
| D0.3 |
13000 |
1000 |
13000 |
1000 |
13000 |
1000 |
| D0.3 |
13000 |
1200 |
13000 |
1200 |
13000 |
1200 |
| D0.3 |
12000 |
1500 |
12000 |
1500 |
12000 |
1500 |
| D0.3 |
12000 |
1500 |
12000 |
1500 |
12000 |
1500 |
| D0.3 |
11000 |
1800 |
11000 |
1800 |
11000 |
1800 |
| D0.3 |
10000 |
2200 |
10000 |
2200 |
10000 |
2200 |
| D0.3 |
10000 |
2200 |
10000 |
2200 |
10000 |
2200 |
| D0.3 |
9000 |
2500 |
9000 |
2500 |
9000 |
2500 |
Note:
*Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum spindle speed;
*Recommend oil coolant for Stainless Steels and Heat Resistance Alloys;
*Recommend using a non-contact measuring device to avoid damaging the precision tip point;
*Decrease both spindle speed and feed rate proportionally in case of chattering.