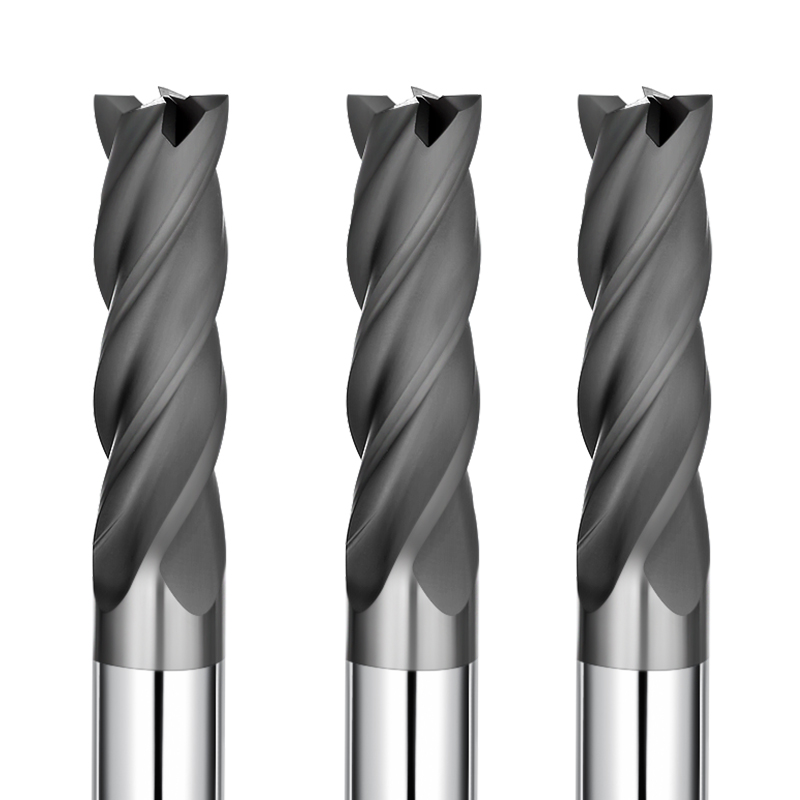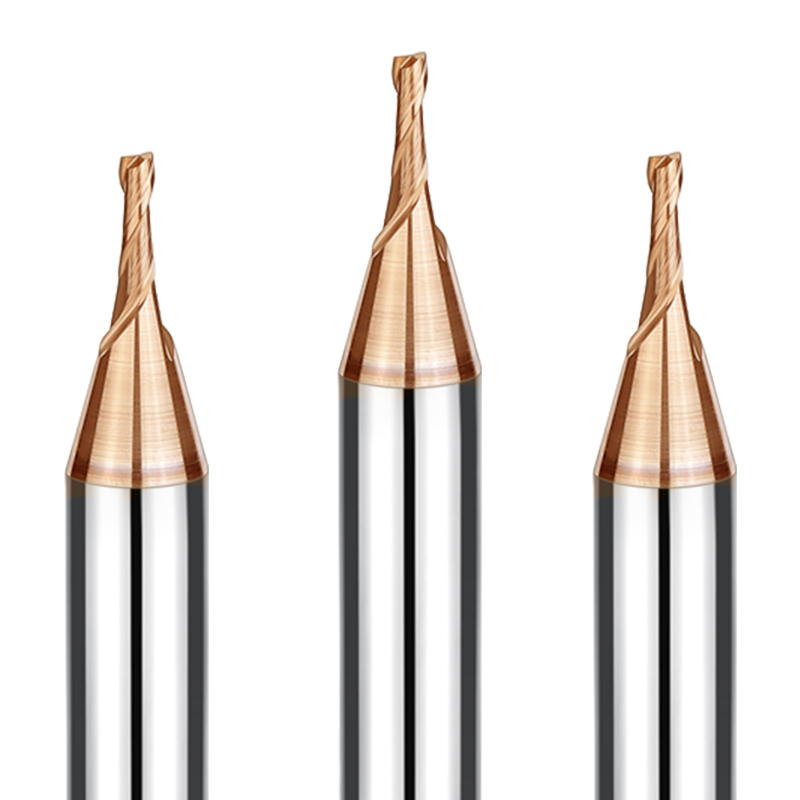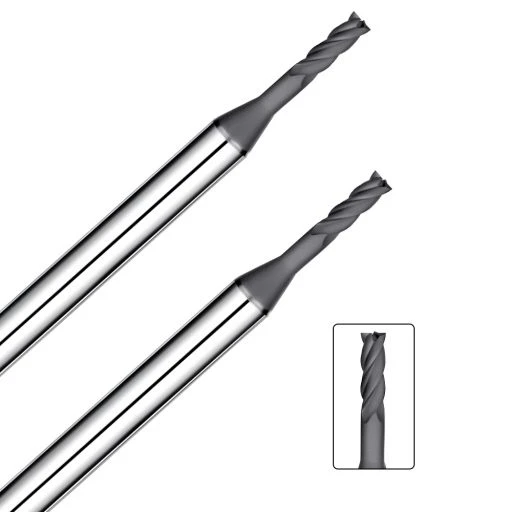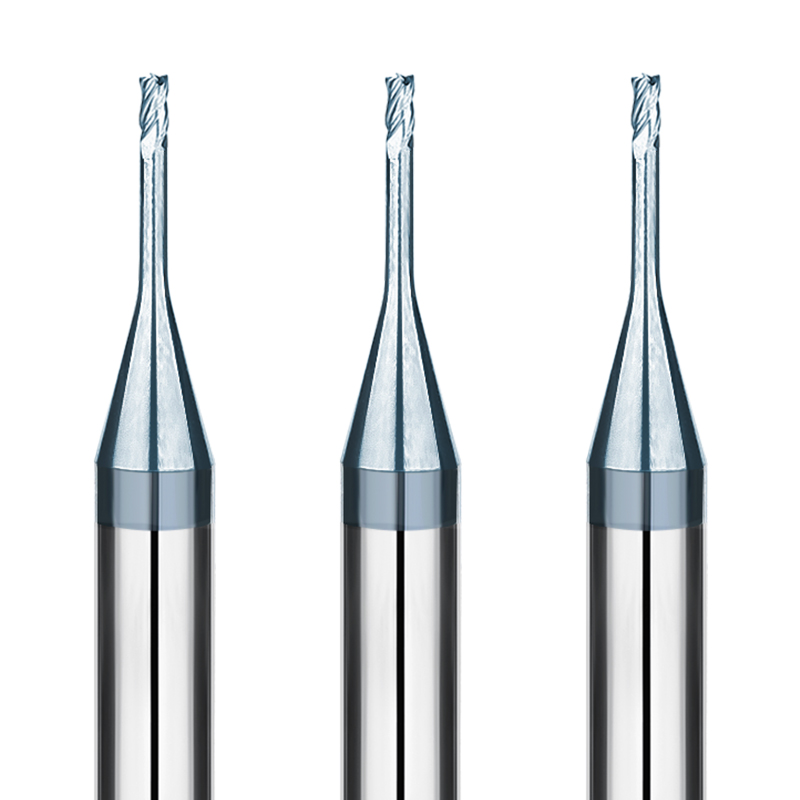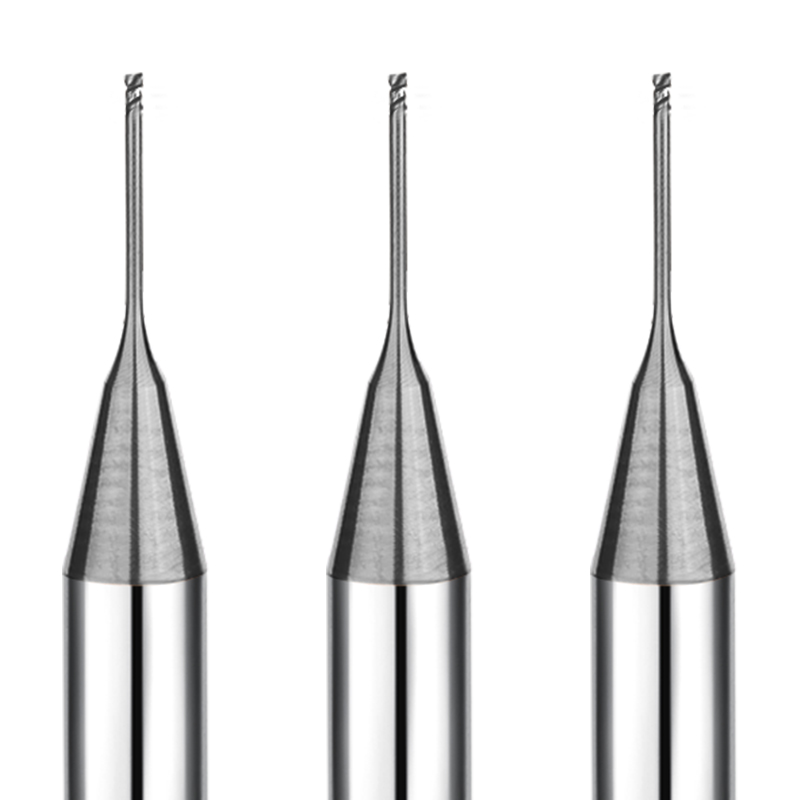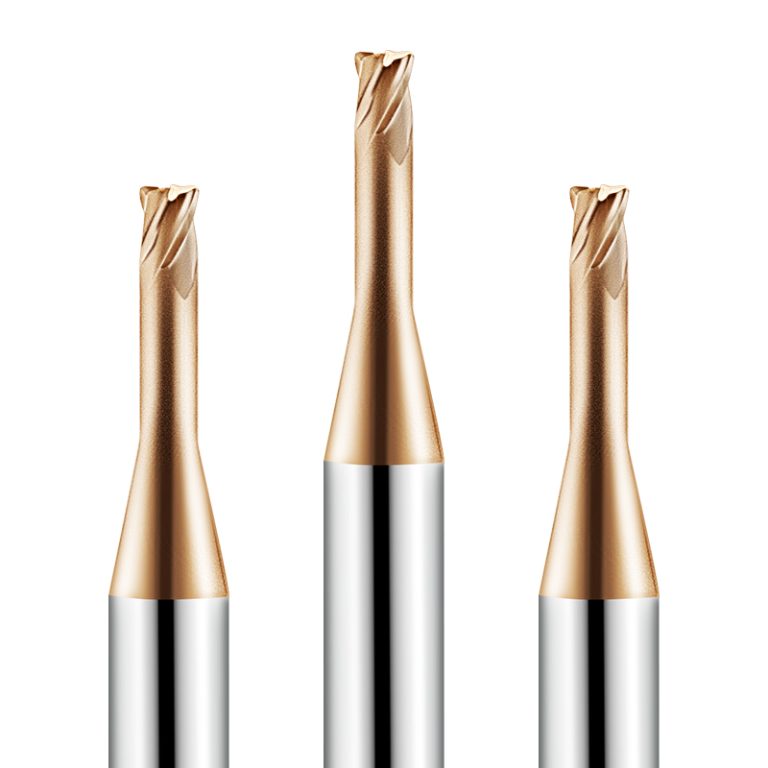
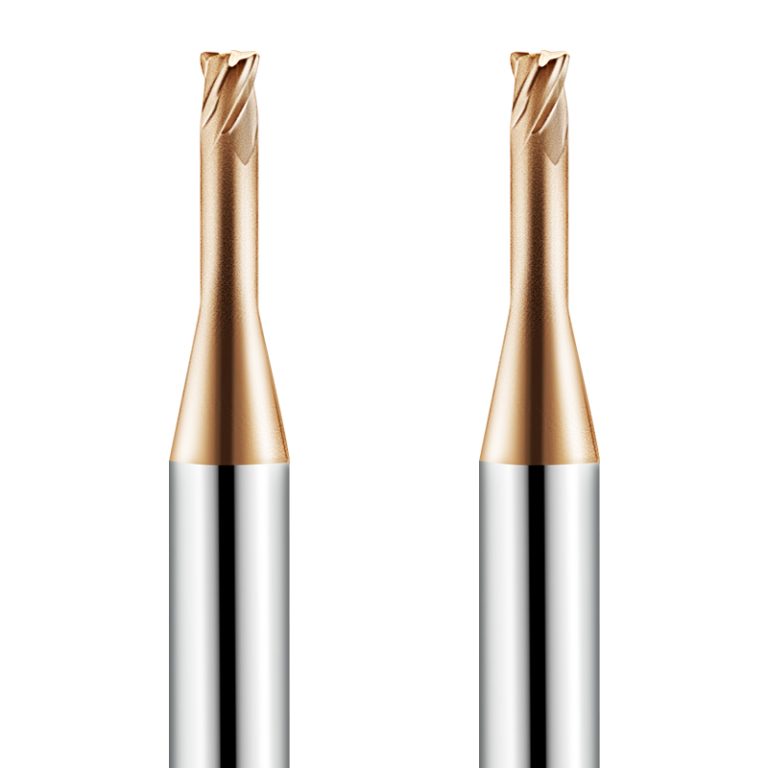
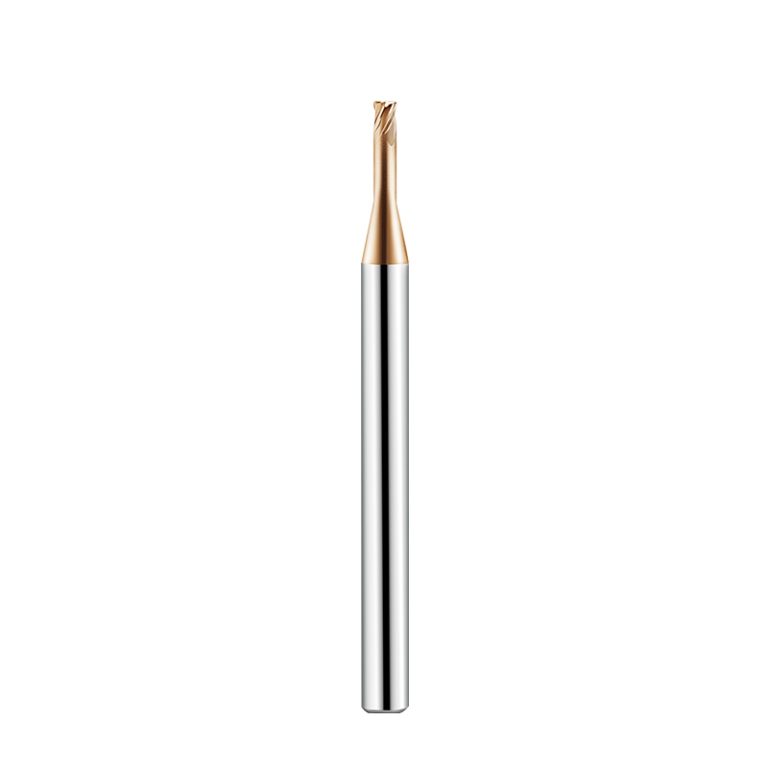
end mill end mill end mill

End Mill for Hardened Steel 4 Flute Long Neck Corner Radius End Mill

SAMHO 4-Flute Long-Neck Corner-Radius End Mill with High-Wear-Resistance Coating — Precision Machining Tool for Hardened Steel

Don’t let high-hardness materials compromise your machining efficiency. The SAMHO 4-flute long neck corner radius endmill is engineered for precision CNC machining of hardened steel and other high-hardness alloys. It delivers efficient and stable performance, even under high-intensity cutting conditions.

Featuring advanced high-adhesion, wear-resistant coating technology, this tool has been field-proven to maintain a sharp cutting edge over extended periods.

Applicable Materials
Optimized for hardened steel, high-hardness alloys, and wear-resistant steels. Ideal for deep-cavity machining and processing complex contours.

Exceptional Durability
Built with an ultra-fine-grain carbide substrate and precision-ground geometry, enhanced by a high-adhesion, wear-resistant coating:

  • Extended Tool Life: Significantly increases tool longevity, reducing tool replacement frequency.
  • Superior Resilience: Resists micro-chipping and withstands high temperatures, ideal for continuous cutting of hardened steels.
  • Precision Shank: Precisely machined shank diameter ensures stable mounting and improved machining accuracy.

In the field of hardened steel machining, cutting tools must meet extremely high standards for both precision and durability. They need to deliver excellent cutting accuracy while withstanding long-term wear from high-hardness steels and alloys.

SAMHO’s specially coated 4-flute long neck corner radius end mill is engineered to meet these demanding requirements. Its optimized cutting edge geometry and advanced wear-resistant coating improve both cutting efficiency and tool life. This end mill helps CNC operators efficiently and consistently process quenched steel and other high-hardness materials.


Advanced Technical Features

High-Adhesion Coating for Ultra-Long Tool Life
SAMHO’s proprietary high-wear coating technology gives this end mill exceptional hardness and chemical inertness:

  • Wear Resistance: Maintains a sharp cutting edge during prolonged, continuous machining of hardened steels and high-hardness alloys.
  • Prevents Micro-Chipping: Keeps the coating firmly bonded to the carbide substrate under high-speed friction and heavy cutting loads.

4-Flute, Long-Neck, Corner-Radius Geometry Optimized for Hardened Steel
The carefully engineered cutting-edge geometry delivers outstanding performance in complex contour and deep cavity machining:

  • Efficient Cutting: The optimized 4-flute structure with corner-radius design enables smooth cutting, reducing vibration and heat accumulation.
  • Deep Cavity Adaptability: Long-neck design allows easy access to deep holes, narrow cavities, and complex mold profiles.

Efficient Chip Evacuation and “Cool Cutting” Performance
Sharp cutting edges and optimized flute geometry lower cutting heat and improve machining efficiency:

  • Rapid Chip Evacuation: Quickly removes chips and debris from the cutting zone, preventing localized heat buildup.
  • Reduced Cutting Load: Minimizes heat accumulation, preventing thermal cracking in hardened steels.

Ultra-Fine Grain Carbide Substrate and High-Precision Grinding
High-strength, ultra-fine grain carbide combined with precision grinding ensures exceptional machining accuracy and repeatability:

  • Dimensional Tolerance Control: Strictly held within ±0.01 mm, guaranteeing consistent batch production.
  • Fracture Resistance: Significantly improves tool durability, making it ideal for machining hardened steels and highly abrasive materials.

Target Applications & Industries

This series of 4-flute long-neck corner-radius end mills is ideal for:

  • Precision contouring and machining of hardened steels and other high-hardness alloys
  • Machining mold cavities and deep cavities
  • Processing wear-resistant and high-hardness materials
  • Creating high-precision contours, complex structures, and internal corners

Why Choose SAMHO as Your Wholesale Partner?

OEM/ODM Support: Customized tool specifications and designs meet diverse project requirements with full flexibility.

High-Precision Shank Diameter: Tolerance is strictly controlled within 0–0.003 mm, ensuring stable tool installation and improved machining accuracy.

High Wear-Resistant Coating: Patented coating technology delivers exceptional tool life and durability, ideal for hardened steel and other high-hardness materials.

Excellent Cutting Performance: The 4-flute structure, long neck, and corner-radius design deliver efficient cutting in deep cavities, complex contours, and high-precision internal angles.

Trusted International Supplier: Mature production processes and strict quality control ensure consistent performance and reliable batch supply.
Recommended Materials for Machining (Highly Recommended: ⭐️ | Recommended: ⭕️ | Suggested: )

Category Work Material Grade
DIE STEEL Carbon steels (S45C/S55C)
Alloy steels (SK/SCM/SUS)
Prehardened steels (NAK/HPM)
Hardened steels (~55/~60/~70HRC) ⭐️
SPECIAL MATERIAL Aluminum alloys
Graphite
Copper
Plastics
Carbon fiber
Titanium alloys
Heat resistant alloys
Cemented carbide
Hard brittle (non-metallic) material

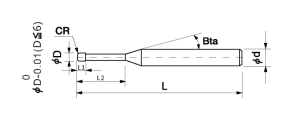
long neck corner radius end mill

Total 83 models

Model Number Outside Diameter Radius Length Of Cut Effective Length Shank Taper Angle Overall Length Number Of Flutes Shank Diameter In Stock
SHHLSR4-01001040 D1.0 R0.1 1 4 12° 50 4 4
SHHLSR4-01001060 D1.0 R0.1 1 6 12° 50 4 4
SHHLSR4-01001080 D1.0 R0.1 1 8 12° 50 4 4
SHHLSR4-01001100 D1.0 R0.1 1 10 12° 50 4 4
SHHLSR4-01001120 D1.0 R0.1 1 12 12° 50 4 4
SHHLSR4-01001160 D1.0 R0.1 1 16 12° 50 4 4
SHHLSR4-01002040 D1.0 R0.2 1 4 12° 50 4 4
SHHLSR4-01002060 D1.0 R0.2 1 6 12° 50 4 4
SHHLSR4-01002080 D1.0 R0.2 1 8 12° 50 4 4
SHHLSR4-01002100 D1.0 R0.2 1 10 12° 50 4 4
SHHLSR4-01002120 D1.0 R0.2 1 12 12° 50 4 4
SHHLSR4-01002160 D1.0 R0.2 1 16 12° 50 4 4
SHHLSR4-01501060 D1.5 R0.1 1.5 6 12° 50 4 4
SHHLSR4-01501080 D1.5 R0.1 1.5 8 12° 50 4 4
SHHLSR4-01501100 D1.5 R0.1 1.5 10 12° 50 4 4
SHHLSR4-01501120 D1.5 R0.1 1.5 12 12° 50 4 4
SHHLSR4-01501160 D1.5 R0.1 1.5 16 12° 50 4 4
SHHLSR4-01502060 D1.5 R0.2 1.5 6 12° 50 4 4
SHHLSR4-01502080 D1.5 R0.2 1.5 8 12° 50 4 4
SHHLSR4-01502100 D1.5 R0.2 1.5 10 12° 75 4 4
SHHLSR4-01502120 D1.5 R0.2 1.5 12 12° 50 4 4
SHHLSR4-01502160 D1.5 R0.2 1.5 16 12° 50 4 4
SHHLSR4-02001060 D2.0 R0.1 2 6 12° 50 4 4
SHHLSR4-02001080 D2.0 R0.1 2 8 12° 50 4 4
SHHLSR4-02001100 D2.0 R0.1 2 10 12° 50 4 4
SHHLSR4-02001120 D2.0 R0.1 2 12 12° 50 4 4
SHHLSR4-02001160 D2.0 R0.1 2 16 12° 50 4 4
SHHLSR4-02002060 D2.0 R0.2 2 6 12° 50 4 4
SHHLSR4-02002080 D2.0 R0.2 2 8 12° 50 4 4
SHHLSR4-02002100 D2.0 R0.2 2 10 12° 50 4 4
SHHLSR4-02002120 D2.0 R0.2 2 12 12° 50 4 4
SHHLSR4-02002160 D2.0 R0.2 2 16 12° 50 4 4
SHHLSR4-03001060 D3.0 R0.1 3 6 12° 50 4 4
SHHLSR4-03001080 D3.0 R0.1 3 8 12° 50 4 4
SHHLSR4-03001100 D3.0 R0.1 3 10 12° 50 4 4
SHHLSR4-03001120 D3.0 R0.1 3 12 12° 50 4 4
SHHLSR4-03001160 D3.0 R0.1 3 16 12° 50 4 4
SHHLSR4-03001200 D3.0 R0.1 3 20 12° 50 4 4
SHHLSR4-03002060 D3.0 R0.2 3 6 12° 50 4 4
SHHLSR4-03002080 D3.0 R0.2 3 8 12° 50 4 4
SHHLSR4-03002100 D3.0 R0.2 3 10 12° 50 4 4
SHHLSR4-03002120 D3.0 R0.2 3 12 12° 50 4 4
SHHLSR4-03002160 D3.0 R0.2 3 16 12° 50 4 4
SHHLSR4-03002200 D3.0 R0.2 3 20 12° 50 4 4
SHHLSR4-03005060 D3.0 R0.5 3 6 12° 50 4 4
SHHLSR4-03005080 D3.0 R0.5 3 8 12° 50 4 4
SHHLSR4-03005100 D3.0 R0.5 3 10 12° 50 4 4
SHHLSR4-03005120 D3.0 R0.5 3 12 12° 50 4 4
SHHLSR4-03005160 D3.0 R0.5 3 16 12° 50 4 4
SHHLSR4-03005200 D3.0 R0.5 3 20 12° 50 4 4
SHHLSR4-0301060-6 D3.0 R0.1 3 6 12° 60 4 6
SHHLSR4-0301080-6 D3.0 R0.1 3 8 12° 60 4 6
SHHLSR4-0301100-6 D3.0 R0.1 3 10 12° 60 4 6
SHHLSR4-0301120-6 D3.0 R0.1 3 12 12° 60 4 6
SHHLSR4-0301160-6 D3.0 R0.1 3 16 12° 60 4 6
SHHLSR4-0301200-6 D3.0 R0.1 3 20 12° 60 4 6
SHHLSR4-0302060-6 D3.0 R0.2 3 6 12° 60 4 6
SHHLSR4-0302080-6 D3.0 R0.2 3 8 12° 60 4 6
SHHLSR4-0302100-6 D3.0 R0.2 3 10 12° 60 4 6
SHHLSR4-0302120-6 D3.0 R0.2 3 12 12° 60 4 6
SHHLSR4-0302160-6 D3.0 R0.2 3 16 12° 60 4 6
SHHLSR4-0302200-6 D3.0 R0.2 3 20 12° 60 4 6
SHHLSR4-0305060-6 D3.0 R0.5 3 6 12° 60 4 6
SHHLSR4-0305080-6 D3.0 R0.5 3 8 12° 60 4 6
SHHLSR4-0305100-6 D3.0 R0.5 3 10 12° 60 4 6
SHHLSR4-0305120-6 D3.0 R0.5 3 12 12° 60 4 6
SHHLSR4-0305160-6 D3.0 R0.5 3 16 12° 60 4 6
SHHLSR4-0305200-6 D3.0 R0.5 3 20 12° 60 4 6
SHHLSR4-04001080-6 D4.0 R0.1 4 8 12° 60 4 6
SHHLSR4-04001100-6 D4.0 R0.1 4 10 12° 60 4 6
SHHLSR4-04001120-6 D4.0 R0.1 4 12 12° 60 4 6
SHHLSR4-04001160-6 D4.0 R0.1 4 16 12° 60 4 6
SHHLSR4-04001200-6 D4.0 R0.1 4 20 12° 60 4 6
SHHLSR4-04002080-6 D4.0 R0.2 4 8 12° 60 4 6
SHHLSR4-04002100-6 D4.0 R0.2 4 10 12° 60 4 6
SHHLSR4-04002120-6 D4.0 R0.2 4 12 12° 60 4 6
SHHLSR4-04002160-6 D4.0 R0.2 4 16 12° 60 4 6
SHHLSR4-04002200-6 D4.0 R0.2 4 20 12° 60 4 6
SHHLSR4-04005080-6 D4.0 R0.5 4 8 12° 60 4 6
SHHLSR4-04005100-6 D4.0 R0.5 4 10 12° 60 4 6
SHHLSR4-04005120-6 D4.0 R0.5 4 12 12° 60 4 6
SHHLSR4-04005160-6 D4.0 R0.5 4 16 12° 60 4 6
SHHLSR4-04005200-6 D4.0 R0.5 4 20 12° 60 4 6

Contour Milling Parameters

Work Material HRC48-55 hardened steel HRC56-62 hardened steel HRC63-70 hardened steel
Diameter Radius Effective Length (mm) (min-1) Speed (mm/min) Feed (mm) Axial depth (mm) Radidl depth (min-1) Speed (mm/min) Feed (mm) Axial depth (mm) Radidl depth (min-1) Speed (mm/min) Feed (mm) Axial depth
(mm) Radidl depth
D1.0 R0.1 4 21000 1800 0.04 0.3 18000 1500 0.03 0.25 14000 1100 0.02 0.2
D1.0 R0.1 6 16000 1400 0.02 0.3 14000 1200 0.01 0.25 11000 850 0.007 0.2
D1.0 R0.1 8 15000 1100 0.015 0.3 13000 900 0.008 0.25 10000 650 0.005 0.2
D1.0 R0.1 10 13000 800 0.01 0.3 11000 700 0.006 0.25 9000 500 0.005 0.2
D1.0 R0.2 4 21000 1800 0.04 0.3 18000 1500 0.03 0.25 14000 1100 0.02 0.2
D1.0 R0.2 6 16000 1400 0.02 0.3 14000 1200 0.01 0.25 11000 850 0.007 0.2
D1.0 R0.2 8 15000 1100 0.015 0.3 13000 900 0.008 0.25 10000 650 0.005 0.2
D1.0 R0.2 10 13000 800 0.01 0.3 11000 700 0.006 0.25 9000 500 0.005 0.2
D1.5 R0.1 6 19000 1800 0.045 0.5 16000 1500 0.03 0.4 13000 1100 0.02 0.3
D1.5 R0.1 8 16000 1500 0.04 0.5 14000 1300 0.025 0.4 11000 900 0.01 0.3
D1.5 R0.1 10 15000 1300 0.03 0.5 13000 1100 0.02 0.4 10000 750 0.01 0.3
D1.5 R0.1 12 13000 1100 0.03 0.5 11000 950 0.02 0.4 9000 650 0.007 0.3
D1.5 R0.1 16 11000 800 0.02 0.5 9000 700 0.007 0.4 7000 500 0.005 0.3
D1.5 R0.2 6 19000 1800 0.045 0.5 16000 1500 0.3 0.4 13000 1100 0.02 0.3
D1.5 R0.2 8 16000 1500 0.04 0.5 14000 1300 0.025 0.4 11000 900 0.01 0.3
D1.5 R0.2 10 15000 1300 0.03 0.5 13000 1100 0.02 0.4 10000 750 0.01 0.3
D1.5 R0.2 12 13000 1100 0.03 0.5 11000 950 0.02 0.4 9000 650 0.007 0.3
D1.5 R0.2 16 11000 800 0.02 0.5 9000 700 0.007 0.4 7000 500 0.005 0.3
D2.0 R0.1 6 18000 2100 0.06 0.6 15000 1800 0.05 0.5 12000 1300 0.03 0.35
D2.0 R0.1 8 16000 1800 0.05 0.6 14000 1500 0.04 0.5 11000 1100 0.02 0.35
D2.0 R0.1 10 14000 1500 0.05 0.6 13000 1300 0.03 0.5 10000 950 0.015 0.35
D2.0 R0.1 12 13000 1400 0.04 0.6 11000 1200 0.03 0.5 9000 850 0.01 0.35
D2.0 R0.1 16 11000 1100 0.03 0.6 9500 950 0.02 0.5 7500 650 0.007 0.35
D2.0 R0.2 6 18000 2100 0.06 0.6 15000 1800 0.05 0.5 12000 1300 0.03 0.35
D2.0 R0.2 8 16000 1800 0.05 0.6 14000 1500 0.04 0.5 11000 1100 0.02 0.35
D2.0 R0.2 10 14000 1500 0.05 0.6 13000 1300 0.03 0.5 10000 950 0.015 0.35
D2.0 R0.2 12 13000 1400 0.04 0.6 11000 1200 0.03 0.5 9000 850 0.01 0.35
D2.0 R0.2 16 11000 1100 0.03 0.6 9500 950 0.02 0.5 7500 650 0.007 0.35
D3.0 R0.1 6 13000 2100 0.1 0.8 11000 1800 0.07 0.7 9000 1300 0.05 0.6
D3.0 R0.1 8 11000 1800 0.1 0.8 9500 1500 0.07 0.7 7500 1100 0.05 0.6
D3.0 R0.1 10 11000 1700 0.09 0.8 9500 1400 0.06 0.7 7500 1000 0.04 0.6
D3.0 R0.1 12 11000 1600 0.08 0.8 9500 1400 0.06 0.7 7500 1000 0.04 0.6
D3.0 R0.1 16 10000 1500 0.07 0.8 8500 1300 0.05 0.7 7000 900 0.03 0.6
D3.0 R0.1 20 8000 1100 0.05 0.8 7000 950 0.04 0.7 5500 700 0.02 0.6
D3.0 R0.2 6 13000 2100 0.1 0.8 11000 1800 0.07 0.7 9000 1300 0.05 0.6
D3.0 R0.2 8 11000 1800 0.1 0.8 9500 1500 0.07 0.7 7500 1100 0.05 0.6
D3.0 R0.2 10 11000 1700 0.09 0.8 9500 1400 0.06 0.7 7500 1000 0.04 0.6
D3.0 R0.2 12 11000 1600 0.08 0.8 9500 1400 0.06 0.7 7500 1000 0.04 0.6
D3.0 R0.2 16 10000 1500 0.07 0.8 8500 1300 0.05 0.7 7000 900 0.03 0.6
D3.0 R0.2 20 8000 1100 0.05 0.8 7000 950 0.04 0.7 5500 700 0.02 0.6
D3.0 R0.5 6 13000 2100 0.1 0.8 11000 1800 0.07 0.7 9000 1300 0.05 0.6
D3.0 R0.5 8 11000 1800 0.1 0.8 9500 1500 0.07 0.7 7500 1100 0.05 0.6
D3.0 R0.5 10 11000 1700 0.09 0.8 9500 1400 0.06 0.7 7500 1000 0.04 0.6
D3.0 R0.5 12 11000 1600 0.08 0.8 9500 1400 0.06 0.7 7500 1000 0.04 0.6
D3.0 R0.5 16 10000 1500 0.07 0.8 8500 1300 0.05 0.7 7000 900 0.03 0.6
D3.0 R0.5 20 8000 1100 0.05 0.8 7000 950 0.04 0.7 5500 700 0.02 0.6
D4.0 R0.1 8 10000 2100 0.15 1.2 8500 1800 0.08 1 7000 1300 0.06 0.8
D4.0 R0.1 10 10000 2100 0.15 1.2 8500 1800 0.08 1 7000 1300 0.06 0.8
D4.0 R0.1 12 10000 2100 0.15 1.2 8500 1800 0.08 1 7000 1300 0.06 0.8
D4.0 R0.1 16 8000 1800 0.1 1.2 7000 1500 0.06 1 5500 1100 0.05 0.8
D4.0 R0.1 20 7200 1500 0.09 1.2 6300 1300 0.06 1 5000 950 0.04 0.8
D4.0 R0.2 8 10000 2100 0.15 1.2 8500 1800 0.08 1 7000 1300 0.06 0.8
D4.0 R0.2 10 10000 2100 0.15 1.2 8500 1800 0.08 1 7000 1300 0.06 0.8
D4.0 R0.2 12 10000 2100 0.15 1.2 8500 1800 0.08 1 7000 1300 0.06 0.8
D4.0 R0.2 16 8000 1800 0.1 1.2 7000 1500 0.06 1 5500 1100 0.05 0.8
D4.0 R0.2 20 7200 1500 0.09 1.2 6300 1300 0.06 1 5000 950 0.04 0.8
D4.0 R0.5 8 10000 2100 0.15 1.2 8500 1800 0.08 1 7000 1300 0.06 0.8
D4.0 R0.5 10 10000 2100 0.15 1.2 8500 1800 0.08 1 7000 1300 0.06 0.8
D4.0 R0.5 12 10000 2100 0.15 1.2 8500 1800 0.08 1 7000 1300 0.06 0.8
D4.0 R0.5 16 8000 1800 0.1 1.2 7000 1500 0.06 1 5500 1100 0.05 0.8
D4.0 R0.5 20 7200 1500 0.09 1.2 6300 1300 0.06 1 5000 950 0.04 0.8

Milling Amount for Side Milling(mm)

Work Material \ Length of Cut 2.5D (Length of Cut=Diameter*2.5) 4D (Length of Cut=Diameter*4)
45HRC以下Below 45HRC ae​=0.07Dap​=2D ae​=0.07Dap​=2D
45HRC以上Above 45HRC ae​=0.03Dap​=1.5D ae​=0.03Dap​=1.5D

D: Diameter (mm)

ap:AxialDepth (mm)

ae: Radial Depth (mm)

Note:

*Decrease both spindle speed and feed rate proportionally when the milling parameters exceed the machine’s maximum spindle speed;

*Recommend oil coolant for Stainless Steels and Heat Resistance Alloys;

*Recommend using a non-contact measuring device to avoid damaging the precisiontip point;

*Decrease both spindle speed and feed rate proportionally in case of chattering;

*When the material hardness is greater than HRC58 degrees, it is recommended to use air blow cooling for roughing andoil mistor air blow cooling for finishing.

Download 2: End Mill for Hardened Steel 4 Flute Long Neck Corner Radius End Mill File

Related Product

Related Post

hrc65 NPT full teeth thread mill

In the manufacturing of high-pressure fittings and precision molds, threading after heat treatment is a critical challenge. The SAMHO HRC65 Full-Tooth NPT Series is designed

Read More »
Get Your Custom Milling Tool Guide

Fill out the form below to receive SAMHO’s complete product catalog.